Quick Overview: Accumulator Unloading Valve in Excavators
What is an accumulator unloading valve and what does it do in an excavator?
An accumulator unloading valve manages the charge-and-hold cycle of a hydraulic accumulator by automatically diverting pump flow to the reservoir when the accumulator reaches its maximum set pressure, then resealing to allow recharging when pressure drops. In excavators, it protects the pilot circuit, swing brake release system, and emergency lowering functions — ensuring the accumulator is reliably charged between demand events without the pump running at full pressure unnecessarily.
How the charge-unload-recharge cycle works:
- Charging phase – pump pushes fluid into the accumulator while the valve remains closed; pressure builds toward the cut-out threshold
- Cut-out (pump unloads) – when accumulator pressure reaches the set maximum, the valve diverts pump output to the reservoir at near-zero pressure, minimizing energy use and heat generation
- Discharge phase – accumulator supplies pilot valves, swing brake release, and actuators while the pump idles; built-in check valve prevents reverse flow back through the valve
- Cut-in (pump reloads) – when pressure drops to approximately 85% of the cut-out setting, the valve closes and pump recharges the accumulator automatically
HFD VDA specifications at a glance:
- Flow variants – VDA 38: 25 L/min | VDA 12: 50 L/min | VDA 34: 100 L/min
- Max pressure – 210 bar (aluminium body) | 350 bar (steel body)
- Temperature range – −40°C to +100°C
- Built-in check valve – eliminates need for a separate check valve in the circuit
Example
During an excavator’s idle period between dig cycles, the accumulator unloading valve diverts the pump to the reservoir at near-zero pressure — preventing continuous high-pressure pump operation. When the operator releases the swing brake to resume the next cycle, the accumulator instantly supplies the pilot pressure needed to disengage the brake, with the pump recharging the accumulator automatically within seconds.
Summary
An accumulator unloading valve is the component that makes excavator accumulator circuits reliable — it keeps the accumulator correctly charged, prevents over-pressure damage, protects pump life, and ensures stored pressure is available for pilot control, swing brake release, and emergency lowering exactly when it is needed.
What Is an Accumulator Unloading Valve?
A hydraulic accumulator stores pressurized fluid so that it can be released rapidly when a system demands more flow than the pump alone can supply. But stored pressure needs to be managed — if the accumulator reaches its rated capacity and the pump keeps pushing fluid in, the system risks overcharging, overheating, and component damage. That is the problem the accumulator unloading valve is designed to solve.
An accumulator unloading valve sits in the hydraulic supply line between the pump and the accumulator. According to US Patent 4,199,941 (USPTO), it is operative to prevent the accumulator from being overcharged and to allow the pump to recharge the accumulator should the pressure stored therein fall below a desired minimum value.
This makes the accumulator unloading valve distinct from a standard pump unloading valve, which responds to system idle conditions in general. The accumulator unloading valve specifically responds to accumulator pressure levels — its entire job is managing the charge-and-hold cycle. As noted by AutomationForum, these valves are used in accumulator circuits so that when the accumulator is charged, the pump can be unloaded.
The built-in check valve found on most accumulator unloading valves — including the HFD VDA — plays an equally important role: it prevents stored accumulator pressure from flowing back through the valve toward the pump when the pump is unloaded.
How the Charge-Unload-Recharge Cycle Works
The accumulator unloading valve operates on a cut-out/cut-in principle. Understanding these two pressure thresholds is key to understanding the whole circuit.
Phase 1 — Charging
The pump runs and pushes fluid through the unloading valve into the accumulator. The valve remains closed — blocking the path to the tank — while accumulator pressure is below the set cut-out pressure.
Phase 2 — Cut-Out (Pump Unloads)
When the system pressure reaches the cut-out pressure (the adjusted maximum), the valve acts to divert the pump delivery to the reservoir at low pressure (Yuken Hydraulics). The pump is now unloaded — it keeps running but circulates fluid back to the tank with almost no resistance, consuming minimal energy and generating minimal heat. As described in US Patent 4,199,941 (USPTO), the unloader valve provides the accumulator with a working range in which the pump can idle or be disabled, to prevent the hydraulic fluid from overheating.
Phase 3 — Accumulator Discharges
With the pump unloaded, the accumulator supplies pressure to the circuit — pilot valves, brake release circuits, actuators — as demand requires.
Phase 4 — Cut-In (Pump Reloads)
When the pressure has dropped to approximately 85% of the valve setting, the valve spool closes, thus diverting the pump delivery back to the accumulator to recharge it (Danfoss Engineering Datasheet BC447667830356). This differential band between cut-out and cut-in — sometimes called hysteresis — prevents the valve from cycling rapidly. According to Sun Hydraulics (QCDA Product Data), the pressure differential between unload and reset will be within +3/−2% of the stated ratio of the valve.
The cycle then repeats automatically, maintaining accumulator pressure between its upper and lower thresholds without operator input.
How Excavators Use Accumulator Circuits
Excavators are one of the most demanding environments for accumulator technology. The machine operates in continuous duty cycles, frequently idles between tasks, and must maintain pressure availability for safety-critical functions even when the engine is shut down or the pump fails. Here are the three primary roles accumulator circuits play on a modern excavator.
Pilot Circuit Supply and Pressure Stabilization
The pilot system in an excavator controls the main control valves that command every boom, arm, bucket, and travel function. According to Caterpillar’s 320D–336D Excavator Service Training documentation (SERV1852-01), the pilot accumulator is used to release the swing brake and for lowering the boom and stick in the event of a loss of pilot system pressure or a dead engine. The pilot accumulator also helps to dampen pressure spikes in the pilot system, which enhances the stability of the machine control systems. The accumulator unloading valve in the pilot circuit ensures the pump is not continuously running at full pressure to maintain this supply — it charges the accumulator, unloads, and recharges as needed.
Swing Brake Release
Per Caterpillar SERV1852-01, pilot oil is directed through the swing brake solenoid valve to release the swing park brake in the swing motor group. This is a spring-applied, hydraulically-released brake — meaning it requires stored pilot pressure to disengage. If pilot pressure drops suddenly due to pump failure, engine stall, or rapid demand elsewhere in the system, the accumulator provides the pressure needed to hold the brake released long enough for controlled deceleration, preventing abrupt mechanical lock-up of the swing mechanism.
Emergency Lowering and Safe Shutdown
If there is the possibility of an engine stoppage or pump failure, the properly-sized accumulator stores enough energy to allow the operator to carry out crucial non-powered tasks — for example, using the stored power to securely lower a suspended load, or to release the brakes to allow the machine to be towed (WHYPS — Heavy Equipment Engineering). This is a direct operator safety function. Without a correctly functioning accumulator and its associated unloading valve managing the charge cycle, the accumulator may not hold sufficient pressure when it is needed most.
In all three of these use cases, the accumulator unloading valve is not a passive component — it is the mechanism that ensures the accumulator is reliably charged between demand events, and that the pump is not doing unnecessary work (and generating unnecessary heat) while the accumulator is already at pressure.
What Happens Without a Proper Unloading Valve
Skipping or incorrectly sizing the accumulator unloading valve has predictable consequences:
- Continuous pump overload. Without an unloading valve, the pump must maintain system pressure at all times, even when the accumulator is fully charged, and there is no active demand. This drives up power consumption and engine load unnecessarily.
- Excessive heat generation. When the swing is braking or the boom is lowering during every cycle, the braking energy and the gravitational energy are wasted by converting into heat (ScienceDirect / PMC — Energy-Saving Analysis of Hydraulic Hybrid Excavator). Compounding this with a pump that cannot unload accelerates oil temperature rise, degrading fluid viscosity and seal integrity faster.
- Accumulator bladder failure. If the accumulator is repeatedly charged past its rated pressure because no unloading valve diverts flow at cut-out, the internal bladder or diaphragm is subjected to repeated over-pressure cycles, shortening its service life significantly.
- Rapid valve cycling (pressure hunting). Rapid cycling is commonly caused by incorrect accumulator pre-charge, too small a cut-in/cut-out differential (hysteresis), or leakage through the check valve or system (Rekith Hydraulics). This symptom — sometimes heard as repeated clicking or chatter from the valve — signals that the unloading valve’s differential band is mismatched to the accumulator volume.

The HFD Accumulator Unloading Valve — VDA
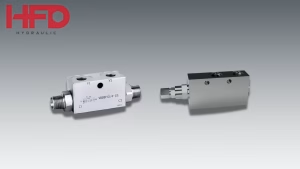
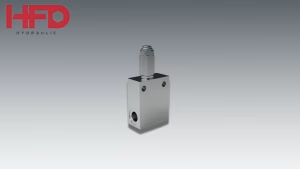
The HFD Accumulator Unloading Valve — VDA is a purpose-built hydraulic valve designed specifically for accumulator circuit management. It is an alternative to the Walvoil VDA and is manufactured by HFD to the same functional specification.
Key features:
- Built-in check valve that prevents reverse flow from the accumulator back through the valve — eliminating the need for a separate check valve in the circuit
- Automatic pressure sensing — redirects pump flow to the reservoir when the accumulator reaches its set pressure, then reseals to allow recharging when pressure drops
- Compact design for integration into existing hydraulic circuits without significant manifold redesign
- Three flow capacity variants to match your system’s demand
VDA Ratings
| Model | Flow Rating |
| VDA 38 | 25 l/min (6.6 US gpm) |
| VDA 12 | 50 l/min (13.2 US gpm) |
| VDA 34 | 100 l/min (26.4 US gpm) |
| Body Material | Maximum Pressure |
| Aluminium | 210 bar (3,050 psi) |
| Steel | 350 bar (5,100 psi) |
| Temperature Rating |
| −40°C (−40°F) to 100°C (212°F) |
The aluminium body suits most excavator accumulator applications that operate within 210 bar. For higher-pressure accumulator circuits, the steel body covers up to 350 bar. The three flow variants — 25, 50, and 100 l/min — allow selection based on actual pump output and accumulator volume, avoiding oversizing that can cause pressure hunting or undersizing that limits recharge speed. The operating temperature range of −40°C to 100°C makes the VDA suitable for excavators working in both cold-climate conditions and high-ambient-temperature job sites.
The VDA’s built-in check valve directly addresses one of the most common installation oversights in accumulator circuits: reverse flow during the pump-unloaded phase. When the pump is diverted to the tank, and the accumulator begins discharging, pressure can attempt to flow backwards through the unloading valve. The integral check prevents this, maintaining stable accumulator pressure during the discharge phase without requiring the installer to source and fit a separate check valve.
→ View the VDA product page and request a quote
Selecting the Right Valve for Your Application
When specifying an accumulator unloading valve for an excavator, consider the following:
- System pressure range. Match the valve’s pressure rating to your accumulator’s maximum rated pressure. For higher-pressure applications, the steel body VDA at 350 bar provides the appropriate margin.
- Cut-in/cut-out differential. According to Sun Hydraulics, careful consideration should be given when selecting an adjustment range — system pressure drops and flows tend to affect the operation of unloading valves, and low operating pressures combined with low differentials result in a very narrow band between unload and reset. A narrower differential means faster cycling; a wider differential means a larger pressure swing in the accumulator between charges.
- Accumulator pre-charge pressure. The nitrogen pre-charge in a bladder or diaphragm accumulator should be matched to the system’s minimum operating pressure. If the pre-charge is too high relative to the cut-in pressure, the accumulator will not accept fluid at the recharge point and rapid cycling may result.
- Check valve integration. If your existing circuit does not already include a check valve between the pump and the accumulator, the VDA’s built-in check valve simplifies installation and reduces potential leak points.

Related Resources
For further reading on related hydraulic valve types covered on this site:
- Hydraulic Unloading Valve: The Complete Guide — Overview of all unloading valve types and principles
- Two-Pump High-Low Unloading Valve Systems — High-low pump circuits and their unloading logic
- CETOP Face Mounting High-Low Unloading Valves — Compact mounting alternatives for unloading valve integration
- Shuttle Valves in Mobile Hydraulics — How shuttle valves interact with pilot and accumulator circuits
- Dump Truck Hydraulic Control Valve Complete Guide — Another heavy equipment application of pressure control valves
→ Contact HFD to discuss your application or request a VDA quote