Quick Overview: Double Pilot Operated Check Valve in AWP Leveling Systems
What does a double pilot operated check valve do in an aerial work platform?
It locks each leveling or outrigger cylinder in position — in both the extend and retract directions — so the platform chassis stays level once set, even as the load shifts or the platform moves on uneven ground. Because the valve is bi-directional, it holds the cylinder regardless of which way an external force is trying to push it.
Why leveling circuits specifically need the double (not single) version:
- A single pilot check valve only actively controls one direction of flow; the free-flow direction can still permit drift under an off-balance load.
- Leveling systems can be pushed from either direction depending on ground slope and load position, so both directions need positive, pilot-controlled shutoff.
- Multiple cylinders in the same leveling circuit must hold independently without cross-influencing each other — a role the valve’s independent A/B pilot circuits are built for.
Where it sits in the circuit: mounted directly at (or very close to) each leveling/outrigger cylinder port, downstream of the directional control valve, so mechanical failure of a hose or fitting elsewhere in the circuit cannot cause the cylinder to drift or collapse.
Why Leveling Precision Matters on Aerial Work Platforms
Mobile elevating work platforms (MEWPs) — the term that now formally covers boom lifts, scissor lifts, and vertical mast lifts under ANSI/SAIA A92.20 — are designed to raise personnel, tools, and materials well above the chassis. Because the platform amplifies any base-level tilt, keeping the chassis level (or within a certified slope tolerance) before and during elevation is a structural stability requirement, not just an operator convenience.
Under the A92.20 design standard, which replaced the older A92.3, A92.5, and A92.6 standards effective June 1, 2020, manufacturers must equip MEWPs with a chassis tilt sensor that alerts the operator and automatically restricts boom or drive functions if the machine exceeds its rated slope limit — a function directly dependent on how precisely the machine can be leveled and held level in the first place (Sunbelt Rentals; Construction Equipment magazine). JLG’s product management team notes that this platform load and tilt sensing is a standard MEWP feature under the updated design rules, and manufacturers now provide real-time feedback displays so operators can confirm the machine is within its operating envelope before working aloft (JLG).
It’s worth being precise about which regulation applies to which equipment: OSHA’s federal aerial-lift standard, 29 CFR 1926.453, incorporates the older ANSI A92.2-1969 definition of “aerial lift,” and OSHA has clarified in a standard interpretation that scissor lifts are not covered under that definition — they instead fall under the mobile-scaffold requirements in 1926.452(w) and the general scaffold rules in 1926.451. Boom-type and articulating platforms are covered by 1926.453. ANSI’s voluntary A92.20/22/24 suite, by contrast, applies its design, safe-use, and training requirements across both groups of equipment (Group A — vertical-travel machines like scissor lifts, and Group B — boom-type machines) (United Rentals). In practice, this means the leveling and tilt-sensing hardware discussed below is relevant to both equipment groups, even though the two categories sit under different federal citations.
How Leveling and Outrigger Circuits Work
Most self-leveling scissor lifts and truck- or trailer-mounted AWPs use one of two leveling approaches: independently controlled outrigger/jack cylinders that touch down on the ground before the platform extends, or a leveling cylinder integrated into the lift linkage itself that compensates for chassis tilt as the platform rises.
In a typical circuit, a directional control valve routes pressurized fluid to the piston or rod side of each leveling cylinder, and a check valve — pilot-operated so it can be commanded open in the reverse-flow direction — sits at the cylinder port to prevent the cylinder from retracting or extending under external force once the directional valve returns to neutral. A U.S. patent for a hydraulic leveling circuit for power machines describes exactly this arrangement: a pilot-operated check valve permits flow along the leveling path during a commanded cylinder movement, but blocks flow — locking the cylinder — when an external load tries to compress it outside of a commanded motion (USPTO Patent 11,168,712).
TVH’s parts catalog for scissor lift hydraulics confirms that check valves are a standard component across scissor lift hydraulic systems specifically because they allow flow in one direction while blocking it in the other whenever port pressures are equalized or reversed — the basic mechanism leveling circuits rely on to hold position (TVH Americas). A hydraulics training resource that walks through scissor lift circuit design similarly notes that a pilot-operated check valve is used specifically to hold the load stationary at any position, with the pilot signal for opening it sourced from the lowering side of the circuit (e4training Scissor Lift Design Project).

Why the Leveling Function Calls for the Double Pilot Design
A single pilot operated check valve — the type discussed in the training example above — controls flow in one direction only (typically the lowering or retraction path) while behaving as a passive, spring-loaded check valve in the other. That’s sufficient for a simple lift circuit where load direction is predictable. Leveling and outrigger circuits are a different problem: because ground slope and load distribution can push a cylinder in either direction depending on which corner of the machine is loaded or which way the terrain slopes, the valve needs active, pilot-controlled shutoff on both the extend and retract sides.
This is where the double pilot operated check valve’s independent A/B pilot circuits — each with its own pilot piston, sized so pilot pressure on one circuit doesn’t affect the closure of the other — become the more application-appropriate choice for chassis leveling. It also matters when multiple leveling cylinders are running off the same circuit: independent bi-directional locking at each cylinder prevents one corner of the platform from creeping out of level while another corner holds firm, which would otherwise reintroduce the very chassis tilt the leveling system exists to eliminate.
Pressure spikes are a related concern specific to scissor mechanisms. Because hydraulic fluid is effectively incompressible, a sudden load transfer onto an elevated scissor table — rather than a smoothly applied load — can generate transient pressure spikes reported to reach two to four times steady-state operating pressure (Industrial Monitor Direct). A leveling or lift cylinder held only by a passive check valve is more exposed to seat damage or gradual leakage under repeated spikes like this; a pilot-operated valve rated for the application’s cracking and back-pressure requirements is part of how that risk is managed, alongside correct cylinder mounting and circuit design.
Single Pilot vs. Double Pilot Check Valves in Leveling Applications
| Consideration | Single Pilot Check Valve | Double Pilot Operated Check Valve |
| Direction of active pilot control | One direction only | Both directions, independently |
| Suitability for outrigger/leveling cylinders under variable side-loading | Limited — free-flow direction can still drift | Better matched — both directions positively locked |
| Behavior with multiple cylinders on one circuit | Each valve controls one direction per cylinder; asymmetric loading can still cause drift | Independent A/B circuits per cylinder reduce cross-cylinder drift risk |
| Typical use case | Predictable single-direction load holding (e.g., a simple lift cylinder) | Bi-directional holding where load direction isn’t fixed (e.g., leveling, outriggers, cranes) |
(This table is illustrative of the functional distinction; specific valve selection should always be validated against the machine manufacturer’s hydraulic schematic and load case.)
What Happens When a Leveling Valve Underperforms
A leveling circuit that relies on an undersized, worn, or incorrectly specified check valve doesn’t usually fail catastrophically and immediately — it tends to drift. Over repeated cycles, a small amount of internal leakage at the valve seat lets a leveling cylinder creep back toward center, which shows up as a machine that reads level at startup but loses that reading over the course of a shift, or a platform that needs re-leveling more often than the duty cycle should require. Because the chassis tilt sensors required under A92.20 are there specifically to catch out-of-tolerance slope conditions, a leveling circuit that can’t reliably hold its set position will trigger those alarms and restrict boom or drive functions more often than necessary — reducing uptime even before it becomes a safety issue.
For a broader look at diagnosing drift, leakage, and response-time problems in pilot-operated check valves generally, see our Hydraulic Check Valve Selection Guide for Wholesale Buyers and the troubleshooting section of Double Pilot Operated Check Valve: Complete Guide.
Selection Considerations for AWP and Scissor Lift Leveling Circuits
- Leakage rating. Leveling cylinders that are expected to hold position for an entire shift need a valve rated for minimal internal leakage at the seat, not just at initial installation but across its service interval.
- Pilot ratio. The pilot ratio needs to be matched to the back-pressure the valve will see from the leveling cylinder under maximum side-load, so the valve opens reliably on command without becoming unstable under light loads.
- Mounting proximity. As with any load-holding check valve, mounting it directly at (or integrated into) the cylinder port — rather than upstream in the manifold — limits the length of hose or line that could fail and cause uncontrolled movement.
- Independent circuit behavior. For multi-cylinder leveling systems, confirm the valve’s two pilot circuits are genuinely independent, so pressure changes commanding one cylinder don’t inadvertently affect the lock on another.
- Compatibility with the machine’s existing directional and tilt-sensing architecture. Leveling valves don’t operate in isolation — they need to work correctly alongside the machine’s tilt sensor cutout logic described in A92.20, which depends on the leveling system actually holding the position it reports.
HFD’s Double Pilot Check Valve Options
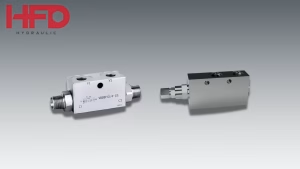
HFD Hydraulic’s double pilot operated check valve line — including the DIN 2352 pilot check valve for double-acting cylinders (VRDE), the double acting pilot check valve (VBPDE), the double flangeable pilot check valve (VRDL-FL), and the double pilot check shut-off valve (VBPDL/R) — covers the mounting configurations (in-line, flanged, manifold) that leveling and outrigger circuit designs typically call for. Full specifications, port sizing, and pilot ratio options for each variant are detailed on the individual product pages.

For related valve types used elsewhere in aerial and crane-adjacent hydraulic systems, see our guides to overcenter valves for truck-mounted crane outriggers and double acting counterbalance valves for aerial work platforms.

Leveling precision on an aerial work platform isn’t a cosmetic feature — it’s the foundation the ANSI A92.20 tilt-sensing and stability requirements are built on top of. Because outrigger and leveling cylinders can be pushed in either direction depending on ground slope and load position, they need bi-directional, pilot-controlled locking — which is exactly what separates a double pilot operated check valve from a single pilot or standard check valve in this application. Specifying the right valve, mounted correctly at the cylinder, with a leakage rating and pilot ratio matched to the machine’s load case, is a direct input into how reliably the platform holds level throughout a shift.