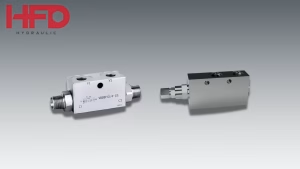
Double pilot operated check valves take hydraulic control to the next level by giving you pilot control in both directions – something you just can’t get with standard single pilot valves. These valves pack two pilot-controlled check valves into one unit, so you get independent control of flow in both directions plus rock-solid load holding no matter which way the pressure’s coming from.
In complex hydraulic systems where precise control of heavy loads is essential—such as mobile crane operations, heavy-duty presses, and vertical positioning systems—the double pilot operated check valve delivers unmatched versatility. Unlike single pilot valves that control flow in only one direction, these dual-control units manage both extension and retraction cycles with equal precision.
In this guide, we’ll break down everything you need to know about double pilot operated check valves – what makes them tick, where they work best, and when you absolutely need them in your hydraulic system.
Quick Overview: Double Pilot Operated Check Valve
What is a double pilot operated check valve?
A double pilot operated check valve combines two independent pilot-controlled check valves in a single housing, providing positive load holding and controlled flow release in both directions. Unlike a single pilot valve that controls only one direction, the double version manages both extension and retraction cycles — making it essential for applications where loads must be locked securely in either position.
Key features and functions:
- Bi-directional load holding – locks the cylinder in position whether extending or retracting, with leakage below 0.5 cc/minute at rated pressure
- Independent pilot circuits – pilot port A1 controls check valve A; pilot port B1 controls check valve B, with no cross-interference between circuits
- Fail-safe protection – both valves close instantly when pilot pressure is removed, preventing uncontrolled movement in either direction
- Cross-pilot configuration – pilot pressure is supplied from the opposite working port, ensuring the correct valve opens automatically during each cycle
- Compact integrated design – single housing eliminates external piping between two separate valves, reducing leak points and installation complexity
Example
In a mobile crane boom system, a double pilot operated check valve holds the boom securely at any raised position. When the operator shifts the directional valve to lower the boom, pilot pressure from port B opens check valve A — allowing controlled retraction while check valve B remains locked, preventing any unintended drop.
Summary
A double pilot operated check valve delivers complete bi-directional load holding, fail-safe protection, and precise positioning control — making it the preferred choice for cranes, heavy presses, vertical positioning systems, and any application where single-direction control is not sufficient.
What is a Double Pilot-Operated Check Valve?
A double pilot operated check valve combines two independent pilot-controlled check valves within a single assembly, each capable of controlling flow in opposite directions. This setup gives you a load-holding system that works both ways – you can control and lock your cylinder whether it’s extending or retracting.
The valve features four main ports: two working ports (A and B) that connect to the cylinder, and two pilot ports (A1 and B1) that receive control signals from the directional control valve. Each internal check valve responds independently to its respective pilot signal, allowing selective opening while maintaining positive closure of the opposite valve.
Key Construction Elements
Dual Check Valve Assembly: Two separate pilot-operated check valves share a common housing, with each valve controlling flow in one direction. The valves operate independently, ensuring that pilot pressure on one side doesn’t affect the closure capability of the opposite valve.
Independent Pilot Control Circuits: Each check valve has its own pilot piston and control chamber, sized to provide optimal pilot ratios for the specific application. This independence prevents cross-talk between control circuits and ensures reliable operation under varying load conditions.
Integrated Design Benefits: The single-housing design eliminates external piping between separate valves, reducing leak points, installation complexity, and system footprint while improving response times through reduced trapped volumes.
Understanding the Double Pilot Operated Check Valve Symbol
The double pilot operated check valve symbol follows ISO 1219 standards while incorporating elements that clearly distinguish it from single pilot variants and other hydraulic components.
Symbol Components Analysis
The symbol displays two check valve triangles pointing in opposite directions, representing the bi-directional control capability. Each triangle includes a spring symbol indicating the closing mechanism, while dashed pilot lines connect to each valve section, showing the independent pilot control paths.

Directional Indicators: The opposing triangle orientations immediately communicate the valve’s ability to control flow in both directions. This visual clarity helps engineers quickly identify the component’s function within complex hydraulic schematics.
Pilot Line Configuration: Two separate dashed lines represent the independent pilot control circuits. These lines typically connect to the opposite working ports of the main directional valve, creating the cross-pilot configuration essential for proper operation.
Port Identification Standards: Standardized port labeling (A, B for working ports; A1, B1 for pilot ports) ensures universal understanding across different manufacturers and international applications.
Circuit Integration Representation
In hydraulic circuit diagrams, the double pilot operated check valve symbol typically appears between the directional control valve and the cylinder, with pilot lines clearly showing the cross-connection pattern. This placement immediately communicates the valve’s role as a load-holding and flow control device.
What is a Double Check Valve Used For?
Double pilot operated check valves are essential when you need to hold loads in both directions, get precise positioning, and have safety features that go way beyond what single pilot or standard check valves can do.
Bi-Directional Load Holding
Heavy Press Applications: In metal forming presses, the double pilot operated check valve holds loads at any position during the forming cycle. Whether holding the ram at the top position during die changes or maintaining precise pressure during forming operations, both extension and retraction positions remain locked until pilot commands allow movement.
Mobile Crane Operations: Boom positioning requires secure holding in both raise and lower directions. The double pilot operated check valve prevents boom drift whether positioned high in the air or during precise load placement operations, maintaining operator safety and load control precision.
Vertical Positioning Systems: Manufacturing equipment with vertical axes, such as drilling machines or assembly systems, relies on double pilot operated check valves to prevent gravity-induced movement in either direction. This capability ensures precise positioning accuracy without continuous pump operation.
Fail-Safe Protection Systems
Dual-Direction Safety: Unlike single pilot valves that provide fail-safe protection in only one direction, double pilot operated check valves offer complete bi-directional protection. If hydraulic pressure fails, both valves close immediately, preventing uncontrolled movement in either extension or retraction directions.
Emergency Stop Functionality: In emergency situations, removing pilot pressure from both control circuits instantly locks the system in its current position. This immediate response capability proves essential in applications where any uncontrolled movement could cause equipment damage or personnel injury.
Advanced Control Applications
Synchronized Multi-Cylinder Systems: Double pilot operated check valves enable precise synchronization of multiple cylinders by providing independent control over each cylinder’s movement while preventing individual cylinders from drifting out of position.
Programmable Logic Integration: Modern automation systems utilize the independent pilot control capability to create complex motion profiles, allowing sophisticated positioning sequences that would be impossible with simpler valve configurations.
How Does a Pilot-Operated Check Valve Work?
The operational mechanics of double pilot operated check valves involve sophisticated interaction between dual independent control circuits, each managing flow and pressure relationships in opposite directions.
Dual-Circuit Operation Principles
Independent Control Mechanisms: Each internal check valve operates on the same pilot-to-open principle as single pilot valves, but with complete independence from its counterpart. Hit pilot port A1 with pressure and only check valve A opens, allowing flow from A to B while check valve B remains closed and locked in place.
Cross-Pilot Configuration: The system connects pilot port A1 to working port B of the directional valve, while pilot port B1 connects to working port A. This cross-connection setup means that when your directional valve shifts to extend the cylinder, the pilot pressure opens the right check valve at the same time while keeping the other one closed tight.
Sequential Operation Analysis
Extension Cycle: During cylinder extension, the directional valve sends high-pressure fluid to port A while port B connects to the tank. Simultaneously, the high pressure at port A feeds pilot port B1, opening check valve B and allowing free flow through the double pilot operated check valve. Check valve A remains closed, preventing backflow.
Retraction Cycle: When the directional valve reverses, high-pressure fluid flows to port B while port A connects to the tank. The high pressure at port B now feeds pilot port A1, opening check valve A for reverse flow while check valve B closes and locks.
Holding Position: When you center the directional valve, both pilot pressures drop back down to tank pressure. Both internal check valves close immediately, creating positive locks in both flow directions and preventing any movement regardless of external loads or minor system leakage.
Pressure Relationship Dynamics
Pilot Ratio Considerations: Each internal check valve typically features pilot ratios between 4:1 and 6:1, providing sufficient mechanical advantage to open against high back-pressure while maintaining sensitivity to pilot commands. The independent pilot ratios can be specified differently for each valve to accommodate asymmetric loading conditions.
Response Time Characteristics: The dual-circuit design provides faster response times than separate valve installations because pilot pressure changes occur simultaneously with directional valve shifts, eliminating the delay associated with pressure buildup in external pilot lines.

| DIN 2352 PILOT CHECK VALVE FOR DOUBLE-ACTING CYLINDER – VRDE | DOUBLE ACTING PILOT CHECK VALVE – VBPDE | DOUBLE FLANGEABLE PILOT CHECK VALVE – VRDL-FL | DOUBLE PILOT CHECK SHUT-OFF VALVE – VBPDL/R |
What is the Difference Between a Check Valve and a Pilot-Operated Check Valve?
The fundamental differences between standard check valves, single pilot operated check valves, and double pilot operated check valves center on control capability, application flexibility, and operational sophistication.
Control Capability Comparison
Standard Check Valve Limitations: Basic check valves provide only passive flow control, opening automatically when forward pressure exceeds cracking pressure and closing when reverse flow is attempted. They offer no external control capability and cannot provide controlled release of trapped pressure.
Single Pilot Operated Check Valve Advantages: These valves add pilot control for opening against back-pressure, enabling controlled release and load holding in one direction. However, they still function as standard check valves in the opposite direction, limiting their application in bi-directional load holding scenarios.
Double Pilot Operated Check Valve Superiority: The dual pilot design provides active control in both flow directions, enabling bi-directional load holding, controlled release, and precise positioning control that neither standard nor single pilot valves can achieve.
Application Flexibility Analysis
Load Holding Capabilities: Standard check valves may allow slight leakage under high back-pressure, causing load drift over time. Single pilot operated check valves stop drift in one direction, but you might still get a little leakage in the free-flow direction. Double pilot operated check valves provide positive sealing in both directions with leakage rates typically below 0.5 cc/minute at rated pressure.
Control Integration: Standard check valves can’t hook up to automated control systems for remote operation. Single pilot valves give you some integration, but only for controlling one direction. Double pilot operated check valves enable complete integration with programmable controllers, proportional valves, and advanced automation systems.
Performance Characteristics
Response Time Differences: Standard check valves respond immediately to pressure differentials but cannot be externally controlled. Single pilot valves respond to pilot commands in one direction while relying on pressure differential in the other direction. Double pilot operated check valves provide consistent, controlled response times in both directions through pilot command signals.
Safety Considerations: Standard check valves provide basic backflow prevention but offer no active safety features. Single pilot valves add fail-safe protection in the pilot-controlled direction. Double pilot operated check valves give you complete fail-safe protection going both ways, which makes them a must-have for critical safety applications.
Cost-Benefit Analysis
| Feature | Standard Check | Single Pilot | Double Pilot |
| Initial Cost | Low | Moderate | High |
| Installation Complexity | Simple | Moderate | Complex |
| Control Capability | None | One Direction | Both Directions |
| Load Holding Precision | Poor | Good | Excellent |
| Safety Features | Basic | Enhanced | Comprehensive |
| Maintenance Requirements | Minimal | Low | Moderate |
Selection and Sizing Guidelines
Proper selection of double pilot operated check valves requires careful analysis of system parameters, operating conditions, and performance requirements specific to bi-directional control applications.
Critical Specification Parameters
Flow Rate Requirements: Size the valve based on actual flow requirements rather than maximum system capacity. Oversized valves can cause control instability and poor response characteristics. Calculate flow rates for both extension and retraction cycles, as asymmetric cylinder designs may require different flow capacities in each direction.
Pilot Ratio Selection: Choose pilot ratios based on the maximum back-pressure conditions and available pilot pressure in your system. Higher pilot ratios (6:1 to 8:1) provide greater sensitivity but may reduce stability under rapid control changes. Lower ratios (3:1 to 4:1) offer more stable control but require higher pilot pressures for reliable operation.
Pressure Rating Considerations: Ensure the valve’s pressure rating exceeds maximum system pressure by appropriate safety margins. Consider pressure spikes during emergency stops or rapid direction changes, which can exceed normal operating pressure by 50-100%.
Environmental Factors
Temperature Range Requirements: Specify seal materials and spring alloys appropriate for your operating temperature range. Standard valves typically operate from -20°F to +200°F, while special materials extend this range to -40°F to +400°F for extreme applications.
Contamination Resistance: Applications with high contamination levels require valves with enhanced filtration protection and contamination-resistant seat materials. Consider integral filtration or upstream filtration requirements to maintain long-term performance.
Integration Considerations
Mounting Configuration: Choose between in-line, manifold-mounted, or flange-mounted configurations based on system layout and maintenance accessibility. Manifold mounting reduces external connections and improves reliability, while in-line mounting offers greater flexibility for retrofit applications.
Pilot Control Routing: Plan pilot line routing to minimize pressure drops and response delays. Keep pilot lines short and avoid restrictions that could impair valve response. Consider pilot pressure relief protection to prevent over-pressurization of pilot circuits.
Installation and Maintenance Best Practices
Proper installation and maintenance of double pilot operated check valves ensures optimal performance, reliability, and service life while preventing common operational problems.
Installation Guidelines
System Flushing Requirements: Before installation, thoroughly flush all hydraulic lines to remove contamination that could damage precision valve components. Use appropriate filtration (typically 10-micron or finer) to maintain fluid cleanliness throughout the system life.
Pilot Line Configuration: Install pilot lines with adequate support to prevent vibration-induced fatigue failures. Use proper routing techniques to avoid sharp bends or restrictions that could impair response times. Include pressure relief protection in pilot circuits to prevent over-pressurization damage.
Torque Specifications: Follow manufacturer torque specifications exactly during installation. Over-tightening can distort valve bodies and cause internal binding, while under-tightening may result in external leakage or pressure loss.
Preventive Maintenance Protocol
Inspection Schedule: Establish regular inspection intervals based on operating hours and duty cycle severity. Check for external leakage, pilot line condition, and response performance during normal operation cycles.
Performance Testing: Every so often, test how well it holds loads by pressurizing both sides of the valve and watching for any pressure drop over time. Acceptable leakage rates should remain below 1 cc/minute at rated pressure for quality valves.
Seal Replacement Intervals: Replace seals based on manufacturer recommendations and operating conditions. High-temperature applications may require more frequent seal service, while clean, moderate-temperature applications can extend service intervals significantly.
Troubleshooting Common Issues
Slow Response Problems: Usually indicate contaminated pilot orifices or damaged pilot seals. Give the pilot circuits a good cleaning and replace any pilot parts that are worn out. Check pilot line routing for restrictions or excessive length.
Internal Leakage: May result from contamination damage to seat surfaces or worn pilot components. Disassemble, clean, and inspect all internal components. Replace any damaged seals or worn metal components.
Erratic Operation: Often caused by air in pilot circuits or unstable pilot pressure supply. Bleed the air out of your pilot lines and make sure you’ve got proper pilot pressure regulation and filtering.
Advanced Applications and Future Developments
Double pilot operated check valves continue evolving to meet increasingly sophisticated application demands while incorporating new technologies that enhance performance and integration capabilities.
Emerging Application Areas
Renewable Energy Systems: Wind turbine pitch control systems utilize double pilot operated check valves for precise blade angle control with positive holding capability in both directions, even during power failures or extreme weather conditions.

Electric Vehicle Manufacturing: Battery pack assembly systems require precise positioning and secure holding during automated assembly processes, where double pilot operated check valves provide the bi-directional control necessary for complex assembly sequences.
Medical Equipment Integration: Advanced surgical tables and imaging equipment rely on double pilot operated check valves for precise positioning and absolute stability during procedures, where any movement could compromise patient safety or procedure accuracy.
Technology Integration Trends
Electronic Control Interface: Modern double pilot operated check valves increasingly incorporate electronic pilot control interfaces, allowing direct integration with PLC systems and proportional control for infinitely variable positioning accuracy.
Condition Monitoring Systems: Integrated sensors provide real-time feedback on valve position, pilot pressure, and performance characteristics, enabling predictive maintenance and performance optimization through data analysis.
Miniaturization Advances: Improved manufacturing techniques enable smaller valve designs without compromising performance, supporting integration into compact machinery and mobile equipment where space constraints are critical.
Future Development Directions
Smart Valve Technology: Next-generation valves will incorporate artificial intelligence for adaptive control algorithms that automatically adjust pilot ratios and response characteristics based on operating conditions and load requirements.
Enhanced Materials: Advanced composite materials and nano-coatings promise extended service life, improved contamination resistance, and operation in extreme environments previously impossible for conventional valve designs.
Wireless Control Integration: Development of wireless pilot control systems will eliminate hardwired pilot connections, simplifying installation and enabling remote control capabilities for hazardous or inaccessible applications.
Double pilot operated check valves represent the pinnacle of hydraulic load control technology, offering bi-directional precision control that single pilot and standard check valves cannot match. You get positive load holding, controlled release, and two-way fail-safe protection – that’s why they’re indispensable when you’re doing critical work in construction, manufacturing, and mobile equipment.
Investing in double pilot operated check valve technology pays off big time with better safety, more precision, less downtime, and greater automation possibilities. As hydraulic systems become increasingly sophisticated and safety requirements more stringent, these advanced components transition from optional upgrades to essential system elements.
When you understand what makes double pilot operated check valves unique, how to select the right ones, and what it takes to integrate them properly, you can pick the best components for your application and get maximum performance and reliability from your system. As technology continues to develop, these valves will keep offering more benefits with more advanced control systems.