A dump truck hydraulic control valve serves as the brain of the entire hydraulic lifting system, orchestrating the precise movement of the dump bed through controlled hydraulic fluid flow. These specialized valves are engineered to handle the demanding requirements of heavy-duty commercial vehicles, where tons of material must be lifted, held in position, and lowered with complete reliability and safety.
In the world of heavy machinery, the dump truck hydraulic control valve stands as a critical component that transforms raw hydraulic power into controlled, purposeful motion. Without this essential piece of equipment, dump trucks would be unable to perform their primary function of loading, transporting, and unloading materials efficiently across construction sites, mining operations, and transportation routes.
Quick Overview: Dump Truck Hydraulic Control Valve
What is a dump truck hydraulic control valve?
A dump truck hydraulic control valve is the central component that directs pressurized hydraulic fluid to the lift cylinders, controlling the raising, holding, and lowering of the dump bed. It translates the operator’s lever or switch input into precise hydraulic movement, handling loads at system pressures typically between 2,000 and 3,000 PSI.
Main types used in dump trucks:
- Monoblock valves – compact, all-in-one units suited for smaller to medium-sized dump trucks
- Sectional valves – modular design allowing customization for multiple hydraulic functions
- Directional control valves – control fluid flow direction for raising and lowering the bed; spring-return to neutral for safety
- Single-spool – for basic dump-only operations
- Multi-spool – for trucks with tailgates, side extensions, or auxiliary equipment
Example
On a construction site dump truck unloading gravel, the directional control valve opens to send pressurized fluid to the lift cylinders, raises the bed to the desired angle, then holds position using internal load-holding check valves until the operator lowers it — all with full control at every stage.
Summary
A dump truck hydraulic control valve manages fluid flow, pressure, and direction to ensure safe, controlled bed operation across construction, mining, and waste management applications.
What Does a Hydraulic Control Valve Do?
Hydraulic control valves function as sophisticated traffic controllers for pressurized fluid within hydraulic systems. These components regulate three fundamental aspects of hydraulic operation: flow rate, pressure levels, and directional movement of hydraulic fluid throughout the system.
The primary responsibility of these valves involves managing the precise distribution of hydraulic fluid under pressure, ensuring that the correct amount of force reaches the appropriate cylinders at the right time. They accomplish this through internal mechanisms that can either restrict, redirect, or completely stop the flow of hydraulic fluid based on operator input or system requirements.
In dump truck applications specifically, hydraulic control valves translate the operator’s simple lever or switch activation into complex hydraulic movements. When an operator starts the dumping process, the valve opens the right pathways to send pressurized fluid to the hydraulic cylinders. This creates enough force to lift thousands of pounds of material, and the operator stays in full control from start to finish.
How Does the Hydraulic System Work on a Dump Truck?
The hydraulic system on a dump truck operates through a carefully orchestrated sequence of components working in perfect harmony. The process begins with the engine-driven hydraulic pump, which draws fluid from the reservoir and pressurizes it to the required operating pressure, typically ranging from 2,000 to 3,000 PSI depending on the truck’s specifications.
Once pressurized, the hydraulic fluid travels through high-pressure hoses to reach the hydraulic control valve, where the operator’s input determines the fluid’s next destination. When the dump function is activated, the control valve opens specific passages that direct the pressurized fluid to the lift cylinders positioned beneath or alongside the dump bed.
As the hydraulic fluid enters the cylinder chambers, it forces the pistons to extend, creating the mechanical advantage necessary to lift the loaded dump bed. The control valve gives operators precise control during the entire process, so they can stop the bed at any angle they want or lower it slowly by sending the fluid back to the reservoir through the return lines.
The entire system operates as a closed loop, with the control valve serving as the central command center that determines when and how the hydraulic energy is applied to achieve the desired dumping action while incorporating safety features that prevent accidental or uncontrolled movement.
Types of Hydraulic Control Valves for Dump Trucks
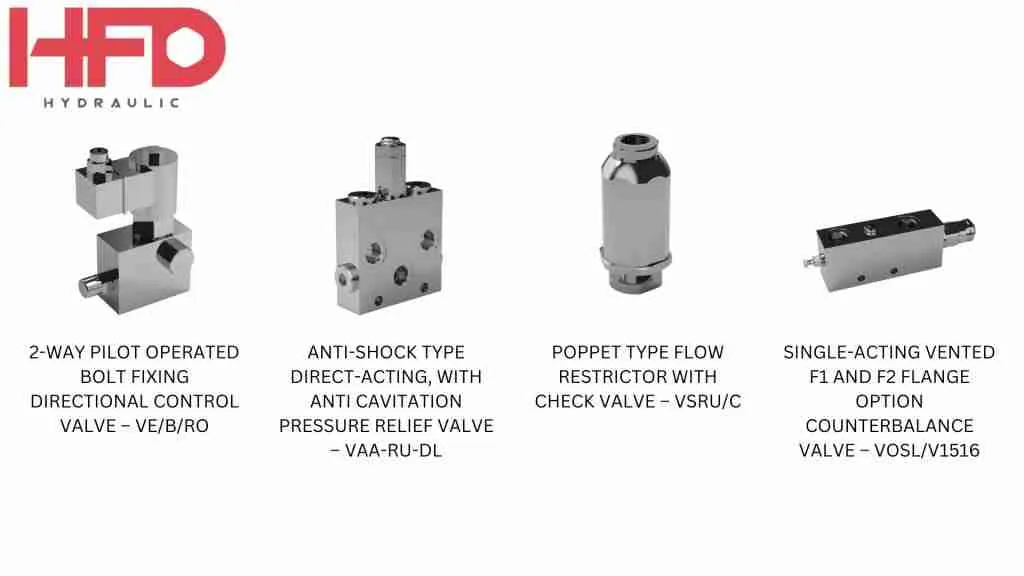
Dump truck manufacturers utilize several distinct types of hydraulic control valves, each designed to meet specific operational requirements and truck configurations. Monoblock valves are compact, all-in-one units where several valve functions are built into one housing. This saves space and makes installation easier, which is why they’re popular on smaller to medium-sized dump trucks.
Sectional valves are more flexible because of their modular design. Manufacturers can customize them by adding or removing sections depending on what the truck’s hydraulic system needs. This modular design really shines when trucks need to handle multiple jobs – running tailgates, powering other hydraulic tools, not just basic dumping.
Directional control valves are the backbone of dump truck hydraulic systems. They control which way the fluid flows to make sure it gets to the right cylinders when lifting or lowering the bed. These valves usually have springs that automatically snap back to the neutral position when the operator lets go, which adds an extra layer of safety.
Single-spool configurations work well for basic dump operations where only one hydraulic function is required, while multi-spool systems accommodate trucks with additional features such as tailgate operation, side extensions, or auxiliary equipment. The choice between single and multi-spool dump truck hydraulic valve systems depends on the specific operational requirements and the level of functionality needed for particular applications.
Key Features and Functions of a Dump Truck Hydraulic Valve
Flow control is one of the most important features in modern dump truck hydraulic valves. It lets operators adjust how fast the bed goes up or down depending on how heavy the load is and what the job requires. This precise flow control keeps everything running smoothly and prevents jerky movements that could make the load shift or put the operator at risk.
Load-holding is a crucial safety feature that uses internal check valves or pilot systems to stop the dump bed from suddenly dropping if something goes wrong with the hydraulics or the system loses pressure. This feature keeps both the operator and anyone working nearby safe from the dangers of a dump bed moving out of control.
Modern dump truck hydraulic valves come with pressure relief systems that automatically kick in to redirect excess pressure when things get overloaded. This keeps your costly hydraulic components safe from damage and maintains consistent performance no matter how much the loads change. These relief systems also help your hydraulic system last longer by preventing pressure spikes that could cause parts to fail early.
Manufacturers design these valves to be tough, using hardened steel construction, precisely machined internal parts, and specialized seals that can handle the brutal conditions found on construction sites and mining operations. Efficiency features such as optimized internal flow paths and minimal pressure drop ensure maximum hydraulic power reaches the lift cylinders while reducing fuel consumption and heat generation.
Common Applications and Importance in Dump Truck Operation
Construction sites are where you really see how important dump truck hydraulic control valves are – they make it possible to efficiently move concrete, asphalt, gravel, and construction debris. Reliable valve performance keeps projects on track and costs under control. That’s exactly why proper maintenance is crucial for construction productivity.
Mining operations place extreme demands on hydraulic control valves due to the massive loads and harsh environmental conditions encountered in these applications. The valves must consistently perform under conditions involving heavy ore loads, abrasive materials, and extended operating cycles that would quickly overwhelm lesser hydraulic components.
Transportation and waste management companies depend on hydraulic valves to give them the precise control they need for safe and efficient material handling. Whether transporting agricultural products, municipal waste, or industrial materials, the control valve’s ability to provide smooth, controlled dumping operations prevents material spillage and ensures safe unloading procedures.
When valves work reliably, it doesn’t just keep things running smoothly day-to-day – it actually saves money across the board by cutting down on maintenance expenses, reducing unexpected shutdowns, and helping entire fleets stay productive. Here’s the thing about hydraulic control valves: when they’re doing their job right, they protect the rest of your system. You’ll spend less on maintenance, your equipment will last longer, and over the truck’s lifetime, those savings can be pretty substantial.
Maintenance Tips for Hydraulic Control Valves on Dump Trucks
Regular inspection schedules should include detailed examination of valve housings for signs of external leakage, corrosion, or physical damage that could compromise valve performance. During visual inspections, you’ll want to look closely at connection points, mounting areas, and the overall condition of the valve body. Keep an eye out for places where environmental stuff like dirt or moisture might be collecting. Pay extra attention to spots where dirt, debris, or other contamination tends to build up.
Keeping your hydraulic fluid clean is key to making valves last longer. You’ll need to test the fluid regularly to check for contamination, see if it’s getting too thick or thin, and make sure the additives haven’t worn out. Dirty fluid wears out the inside parts of valves much faster, which hurts performance and eventually ruins the seals that keep everything working properly.
Cleaning procedures should encompass both external valve surfaces and internal system flushing to remove accumulated debris and contaminants. External cleaning prevents the buildup of materials that could interfere with valve operation, while system flushing removes internal contaminants that could damage precision-machined valve components.
Systematic leak detection involves monitoring all valve connections, seals, and internal passages for signs of fluid loss that could indicate developing problems. Catching small leaks early means you can fix them before they turn into big problems that shut down your equipment and cost a fortune to repair.
Keeping your filters clean is crucial for valve performance – they make sure only clean hydraulic fluid gets to your valves, which prevents dirt and debris from grinding away at the internal parts. Regular filter replacement schedules should be strictly maintained, with consideration given to more frequent changes in severe operating environments where contamination levels may be elevated.
Dump truck hydraulic control valves are really well-engineered components that keep these machines running safely and efficiently across every type of work site. Construction site, mine, anywhere there are heavy loads – these valves let operators control everything precisely and safely, with built-in protection for equipment and crew alike.
The more fleet managers and operators know about hydraulic control valves – the types, features, and maintenance needs – the better choices they’ll make when buying equipment and keeping it running. Proper valve maintenance and performance monitoring pays off in multiple ways – reliable operation, longer equipment life, and lower operating costs.