Quick Overview: “Dump truck valve” is not one part — it’s a system of several distinct valves working together. The main ones are the directional control valve (routes fluid to raise or lower the bed), pressure relief valve (protects the circuit from overpressure), check/load-holding valve (stops the bed from drifting down under load), counterbalance valve (regulates lowering speed), unloading valve (idles the pump when the bed isn’t moving), and end-of-stroke valve (prevents the cylinder from over-extending). Each has a different job, location, and failure mode.
What Does “Dump Truck Valve” Actually Mean?
Search for “dump truck valve” and you’ll get results for at least half a dozen different components — because the term is genuinely ambiguous. A dump truck’s hydraulic system isn’t built around a single valve; it’s built around a small circuit of valves, each handling one job in the sequence of raising, holding, and lowering the dump body.
That distinction matters for anyone specifying parts, diagnosing a problem, or sourcing replacements: asking a supplier for “the dump truck valve” without naming the type is like asking a mechanic for “the truck part.” This guide breaks down each valve type in the circuit, what it does, where it sits, and how to recognize one that’s failing.
How the Valves Work Together in the Hydraulic Circuit
A typical dump truck hydraulic circuit starts with a pump — usually driven off the power take-off (PTO) — that draws fluid from a reservoir and pushes it toward the lift cylinder. Between the pump and the cylinder sits the valve or valve bank that does the actual control work.
In the patented control architecture used across many dump-body hydraulic systems, an unloading valve pilots the system relief valve, either diverting pump output back to the reservoir under low back-pressure when the bed is idle, or directing it toward the lift cylinder when the operator calls for movement (U.S. Patent 4,202,175). A separate cylinder relief valve is piloted into an unloading mode during lowering, with a manually variable flow control valve giving the operator control over how fast the bed comes back down.
At the center of that circuit is the directional control valve, which shifts a spool between neutral, raise, and lower positions to route fluid to or away from the cylinder (U.S. Patent 4,029,359). In the neutral position, fluid entering the valve flows through an internal recess in the spool and straight back to the reservoir, bypassing the cylinder entirely — which is why a truck can idle with the pump running and the bed stationary without building unnecessary pressure. Shifting the lever moves the spool to the raise or lower position, redirecting that same flow to the appropriate side of the cylinder.
Most dump truck applications use a telescopic hydraulic cylinder rather than a single-stage cylinder, since the multi-stage design allows a long travel distance for the bed while collapsing to a compact length when stowed. Every valve in the circuit — from the directional valve down to the end-of-stroke valve — has to be matched to that cylinder’s stroke length, bore, and rated pressure, which is why valve specification is rarely a one-size-fits-all decision across different truck classes and body sizes.
For a full breakdown of how directional control valves are built and specified, see our Dump Truck Hydraulic Control Valve: The Complete Guide.
Dump Truck Valve Types at a Glance
| Valve Type | Function | Typical Location in Circuit | Common Failure Symptom |
| Directional control valve | Routes fluid to raise, hold, or lower the bed | Between pump and lift cylinder | Bed won’t raise/lower, or moves in wrong direction |
| Pressure relief valve | Diverts excess flow to protect the circuit from overpressure | Parallel to pump outlet | Sluggish lift, overheating fluid |
| Unloading valve | Idles the pump (low back-pressure) when the bed isn’t moving | Piloting the system relief valve | Pump runs hot when bed is idle |
| Check / load-holding valve | Prevents backflow so the bed holds position under load | At or near the cylinder port | Bed creeps or drifts down when raised |
| Counterbalance valve | Controls and limits lowering speed under load | At the cylinder’s return line | Bed drops too fast or jerks while lowering |
| End-of-stroke valve | Cuts flow as the cylinder nears full extension, preventing over-travel damage | At the top of the lift cylinder’s travel | Body bounces or over-extends at full lift |
| Flow control valve | Meters fluid flow to regulate operating speed | In-line, often adjustable | Inconsistent or jerky bed movement |
Directional Control Valve
The directional control valve is the component most people mean when they say “dump truck valve.” It shifts fluid flow between raise, hold, and lower positions in response to the operator’s lever or switch input, typically handling system pressures in the 2,000–3,000 PSI range in commercial dump truck applications. Monoblock and sectional configurations, single- and multi-spool designs, and manual, air-shift, or electro-hydraulic actuation are all variations on this same core function. We cover the specifics — including load-holding checks built into the valve body — in our complete guide to dump truck hydraulic control valves.
Pressure Relief Valve
The relief valve is the circuit’s safety margin. If system pressure exceeds a set threshold — from a stuck spool, a cold-start pressure spike, or an overloaded bed — the relief valve opens and routes excess flow back to the reservoir instead of letting pressure damage hoses, seals, or the pump itself. A relief valve that’s stuck closed can cause overheating and premature component wear; one stuck open will leave the truck unable to build enough pressure to lift a full load.
Unloading Valve
The unloading valve keeps the pump from working against full system pressure when the bed isn’t moving. It pilots the system relief valve to divert flow back to the reservoir under minimal back-pressure during idle periods, then redirects pump output to the cylinder the moment the operator calls for a raise or lower (U.S. Patent 4,202,175). This reduces heat generation and wear on the pump during the long stretches of a haul cycle when the bed is simply down and the truck is driving. For a closer look at how unloading valves function in a related mobile hydraulic application, see our piece on the accumulator unloading valve in excavators.
Check Valve / Load-Holding Valve
A check valve — often built directly into the directional control valve body or the cylinder port — allows flow in one direction only. In a dump truck circuit, its job is to prevent fluid from flowing back out of the cylinder once the bed is raised, so the load holds its position rather than settling under its own weight. A load-holding valve that’s worn or contaminated will let the bed creep downward over time, even with the control valve in the neutral or hold position.
Counterbalance Valve
Where a check valve holds position, a counterbalance valve manages controlled motion — specifically, it regulates how fast the bed lowers under the weight of the load, preventing the free-fall condition that can occur if gravity alone were driving the cylinder. It maintains back-pressure on the cylinder during lowering so the descent stays smooth and operator-controlled rather than abrupt.
End-of-Stroke Valve
The end-of-stroke valve is a mechanical safeguard near the top of the lift cylinder’s travel. As the cylinder approaches full extension, the valve progressively restricts flow, slowing the final inches of travel and preventing the kind of hard-stop impact that can damage the cylinder, hoses, or dump body structure. We go into cable actuation, stop-angle adjustment, and installation in detail in our article on end-of-stroke valves for dump trucks.
Flow Control Valve
Flow control valves meter the rate of fluid delivered to the cylinder, independent of pressure, to keep bed speed consistent across varying loads and conditions. In many circuits, a flow control valve works alongside the directional valve to give the operator fine control over lowering speed, complementing the counterbalance valve’s role in managing load-induced motion.
Why Valve Condition Is a Safety Issue, Not Just a Maintenance One
Dump body movement isn’t a minor mechanical concern. NIOSH reports that dump truck-related incidents contributed to the deaths of 809 construction and extraction workers in the United States between 2011 and 2020, with hazards including struck-by incidents, tip-overs, and crushing (NIOSH Publication No. 2023-137). Unintended or uncontrolled bed movement — the exact failure mode a worn check, counterbalance, or relief valve can produce — is a recognized contributor to crushing injuries during maintenance and loading operations.
OSHA’s construction standard, 29 CFR 1926.600(a)(3)(i), requires that elevated parts of heavy equipment, including raised dump bodies, be blocked, secured, or otherwise supported before workers are exposed to them, specifically to prevent unexpected movement during service (OSHA Safety and Health Information Bulletin). A hydraulic valve in good condition is what keeps the bed where the operator puts it in the first place; mechanical props and blocking are the required backup, not a substitute for valve integrity.
Choosing the Right Valves for a Dump Truck Build or Repair
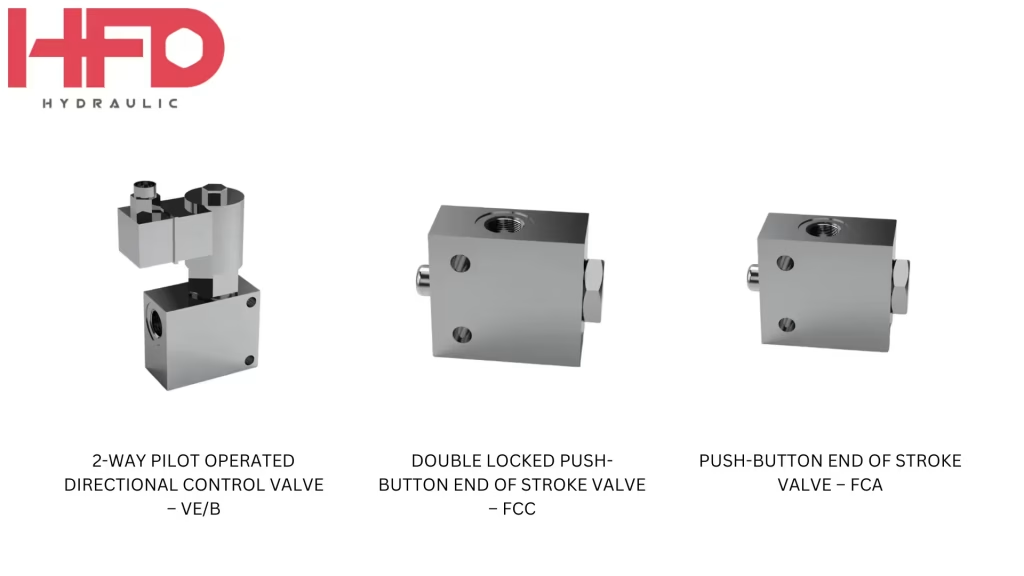
Because each valve type in the circuit does a different job, valve selection typically isn’t a single decision — it’s a matter of matching each position in the circuit to a component rated for the truck’s operating pressure, flow rate, and duty cycle. HFD Hydraulic manufactures several of the valve types covered in this guide for OEM and aftermarket use, including the VE/B series pilot-operated directional solenoid valve for electro-hydraulic control applications, along with the FCA push-button and FCC double-locked end-of-stroke valves for standard and heavy-duty applications, respectively. Anyone specifying or replacing valves should confirm pressure rating, port configuration, and actuation type (manual, air, or solenoid) against the truck’s existing circuit before ordering.
Routine inspection matters as much as initial selection. Because several valve types are load-holding or pressure-limiting components, wear in any one of them can produce similar symptoms — a bed that lowers unevenly could point to a worn counterbalance valve, a failing flow control valve, or an unrelated cylinder issue. Isolating the cause generally requires checking system pressure and flow at each stage rather than replacing parts by guesswork, which is also why OSHA’s blocking and support requirements matter regardless of how well-maintained the circuit is — mechanical support protects workers during the window between a developing issue and its diagnosis.
“Dump truck valve” covers directional control, relief, unloading, check, counterbalance, end-of-stroke, and flow control valves — each with a distinct role in raising, holding, and lowering the dump body safely. Knowing which valve is responsible for a given symptom is the first step in diagnosing a problem correctly, and understanding how they interact is essential for anyone specifying components for a new build or a repair.