If you operate an excavator, you already know that keeping your machine running smoothly isn’t just about getting the job done—it’s about protecting thousands of dollars in equipment from damage. One of the most important but often overlooked components in your excavator’s hydraulic system is the relief valve. Think of it as your machine’s insurance policy against catastrophic pressure problems that can leave you stuck on the job site with expensive repairs.
When you’re digging, lifting, or swinging heavy loads, your excavator’s hydraulic system is constantly building and releasing pressure. Without a properly functioning relief valve, that pressure has nowhere to go when it gets too high. The result? Blown seals, damaged hydraulic pumps, ruptured hoses, and in the worst cases, complete system failure that puts your equipment out of commission for days or even weeks. Now, let’s learn about hydraulic relief valve for excavators and how HFD Hydraulic got you covered.
Quick Overview: Hydraulic Relief Valve for Excavators
What does a hydraulic relief valve do on an excavator?
A hydraulic relief valve protects an excavator’s hydraulic system by automatically releasing excess fluid back to the tank when pressure exceeds a preset limit — preventing blown seals, damaged pumps, and ruptured hoses when the bucket hits solid rock, a cylinder reaches end of travel, or fluid overheats. Without a functioning relief valve, everyday pressure spikes that push a 3,000 PSI system to 4,000–5,000 PSI can trigger a cascade of component failures costing thousands in repairs and days of downtime.
Which HFD relief valve to use by excavator size:
- Mini excavators (1–6 tons) – VMD20 Direct Acting Relief Valve; compact, fast response, suited to lower flow rates and pressures of smaller machines
- Mid-size excavators (6–20 tons) – VMD20; handles pressure spikes common in general construction and excavation work with consistent performance
- Large excavators (20+ tons) – VMD150 Differential Acting Relief Valve; higher flow capacity and more precise pressure control for serious hydraulic power demands
- Rocky or demolition work (all sizes) – VAA-RU-DL Anti-Shock Relief Valve; built-in anti-cavitation and anti-shock features absorb sudden pressure spikes from hitting solid material
Example
An excavator digging in rocky soil hits an immovable boulder mid-stroke. System pressure spikes instantly from 3,000 PSI toward 5,000 PSI. The VAA-RU-DL relief valve opens in milliseconds, diverts excess fluid to tank, and absorbs the shock — the bucket stalls harmlessly against the rock while the pump, hoses, and cylinder seals remain undamaged.
Summary
Choose your excavator relief valve based on machine size and working conditions — standard direct-acting for general work, differential-acting for large machines, and anti-shock with anti-cavitation for demolition or rocky excavation where pressure spikes are frequent and severe.
Why Your Excavator Needs Quality Relief Valves
Every time you move your excavator’s boom, arm, or bucket, you’re creating hydraulic pressure that powers those movements. Under normal conditions, everything works fine. But what happens when you hit an immovable rock while digging? Or when your bucket reaches the end of its travel while still under load? Or when hydraulic fluid heats up on a hot summer day, causing pressure to spike?
These everyday situations create pressure spikes—sudden increases in hydraulic system pressure that can destroy components in seconds. Your excavator’s hydraulic cylinder might be rated for 3,000 PSI, but a pressure spike could momentarily push that to 4,000 or even 5,000 PSI. That’s when things break.
This is where relief valves save the day. When system pressure exceeds the valve’s preset limit, it automatically opens to release excess hydraulic fluid back to the tank. It’s like a pressure safety valve on a pressure cooker—it prevents dangerous pressure buildup before damage occurs.
On construction sites, excavators face brutal conditions. You’re constantly changing between light grading work and heavy digging in rocky soil. Your machine might be lifting heavy materials one minute and carefully positioning pipes the next. Each of these operations creates different pressure demands, and your relief valve is working behind the scenes to keep everything within safe limits.
Without reliable pressure protection, you’re gambling with your equipment every single day. A failed relief valve doesn’t just mean one broken component—it can trigger a cascade of failures throughout your hydraulic system. We’re talking about damaged hydraulic pumps (thousands in repairs), blown cylinder seals (more downtime), burst hydraulic lines (safety hazards), and overheating that cooks your expensive hydraulic oil.

Common Problems Excavator Operators Face
Let’s talk about the warning signs that your excavator’s relief valve might be failing. These are problems that operators notice every day, often without realizing the relief valve is the culprit.
Slow or Sluggish Movement: When your boom takes forever to lift or your bucket curls slower than usual, it’s frustrating. You might think the hydraulic pump is dying, but often the problem is internal leakage in a worn relief valve. When a relief valve doesn’t seat properly, it’s constantly bleeding off pressure that should be powering your cylinders. The result is weak, slow operation that kills your productivity.
Excavator Running Hot: If your hydraulic oil temperature gauge is climbing into the red zone, especially during normal work, your relief valve might be the problem. A stuck-open or leaking relief valve forces your hydraulic pump to work overtime, constantly generating flow that just gets dumped back to the tank. All that wasted energy turns into heat, and before you know it, your hydraulic oil is overheating. Hot oil loses its ability to protect components, leading to accelerated wear throughout your entire system.
Jerky or Erratic Operation: When your excavator’s movements aren’t smooth—maybe the swing function jerks instead of rotating smoothly, or the arm movement seems inconsistent—pressure control issues are usually to blame. A relief valve that’s opening and closing erratically can cause these frustrating control problems. One moment there’s full pressure, the next it’s bleeding off, creating that jerky, unpredictable movement that makes precision work impossible.
Strange Noises: Hydraulic systems should run relatively quietly. If you’re hearing whining, chattering, or squealing sounds coming from your excavator’s hydraulic system, it could indicate a relief valve problem. These noises often mean the valve is rapidly opening and closing, or that cavitation is occurring because pressure isn’t being controlled properly.
Pressure Loss Under Load: The most obvious sign of relief valve trouble is when your excavator loses power under heavy loads. You start digging into hard material and suddenly the boom drops or the bucket loses its curl force. This happens when a relief valve opens too early (wrong pressure setting) or stays open when it shouldn’t (worn components).
The tricky thing is that these signs can appear slowly. The excavator then loses performance over weeks or months. Many operators just adapt to the declining performance without realizing a simple relief valve replacement could restore their machine to like-new operation.
Choosing the Right Relief Valve for Your Excavator
Not all relief valves are created equal, and choosing the wrong one for your excavator can be just as problematic as having a failed valve. Here’s what you need to know.
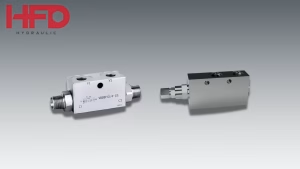
Size Matters: The relief valve needs to match your excavator’s size and hydraulic system capacity. A mini excavator (1-6 tons) has completely different requirements than a 30-ton machine. If you want the perfect balance of quick response and compact for small excavators, HFD VMD20 Direct Acting Relief Valve is the right choice. These machines typically operate at lower flow rates and pressures, making a direct-acting valve ideal.
Mid-size excavators that weigh around 6 to 20 tons handle more demanding work needing relief valves that can handle higher flow rates without causing pressure drops. Since the VMD20 is designed to handle pressure spikes, it works well in general construction and excavation work where pressure spikes are common.
For larger excavators (20+ tons), you’re dealing with serious hydraulic power. These machines need relief valves with higher flow capacity and more precise pressure control. The HFD VMD150 Differential Acting Relief Valve is built for heavy-duty applications where system pressures are higher and the consequences of failure are more severe.
Consider Your Working Conditions: If you’re working in tough environments—rocky soil, demolition sites, or any situation where you’re constantly hitting immovable objects—the HFD VAA-RU-DL Anti-Shock Relief Valve is worth considering. This valve includes anti-cavitation and anti-shock features specifically designed to handle the brutal pressure spikes that occur when your bucket hits solid rock or when you’re breaking through tough material.
What to Look for in Quality: When you’re shopping for a relief valve, don’t just look at price. The construction quality makes a huge difference in how long the valve lasts and how reliably it performs. HFD relief valves are manufactured with precision-machined components that maintain tight tolerances even after years of operation. The materials are selected to withstand contamination, temperature extremes, and the constant pressure cycling that excavators experience.
Cheap relief valves might save you money upfront, but they often use softer materials that wear quickly, looser tolerances that allow internal leakage, and springs that lose their tension over time. Within months, you’re dealing with the same problems all over again.
Adjustability Is Important: Most quality relief valves, including HFD’s product line, feature adjustable pressure settings. This is crucial because different operations require different pressure limits. Your excavator might need 3,000 PSI for normal digging but only 2,500 PSI when using certain attachments. Being able to adjust the relief valve setting means you can optimize performance for each application while still maintaining protection.

| DIRECT ACTING PRESSURE RELIEF VALVE – VMD20 | DIFFERENTIAL ACTING PRESSURE RELIEF VALVE — VMD150 | ANTI-SHOCK TYPE DIRECT-ACTING, WITH ANTI CAVITATION PRESSURE RELIEF VALVE – VAA-RU-DL |
HFD Hydraulic Relief Valves: Built for Real Work
Let’s talk about what makes HFD relief valves different from the cheaper alternatives you’ll find online or at discount suppliers.
Precision Manufacturing: Every HFD relief valve goes through precision machining processes that ensure consistent performance. The valve seats are lapped creating perfect sealing surfaces and the springs are manufactured to exact design specifications; and every component is tested before assembly. This attention to detail means HFD valves respond consistently to pressure changes and maintain their settings over time.
Real-World Durability: Excavators work in some of the harshest conditions imaginable—dirt, dust, extreme temperatures, constant vibration, and contaminated hydraulic oil. HFD relief valves are designed with these realities in mind. The seals are made from degradation resistant materials —degradation caused by heat and contamination. The internal components are hardened to resist wear from dirty hydraulic oil. The valve bodies are built to handle the constant vibration that would cause cheaper valves to fail.
Anti-Shock and Anti-Cavitation Technology: The VAA-RU-DL model incorporates features that specifically address excavator problems. The anti-shock design dampens the sudden pressure spikes that occur when you hit solid objects during digging. Instead of allowing that shock to transmit through your entire hydraulic system, the valve absorbs and dissipates it. The anti-cavitation feature prevents the formation of vapor bubbles that can damage hydraulic components when pressure drops suddenly.
Why Quality Matters: Here’s what you’re actually getting when you choose HFD over cheaper alternatives. First, reliability—HFD valves work correctly day after day, season after season. Second, consistent performance—the pressure settings don’t drift over time, so your excavator maintains its power and control. Third, longevity—these valves are built to last for years, not months. And fourth, peace of mind—you’re not gambling with your expensive excavator every time you start it up.
Simple Maintenance Tips to Extend Valve Life
Even the best relief valve needs proper care to perform at its best. Here are practical maintenance tips that every excavator operator should follow.
Watch for Warning Signs: Pay attention to how your excavator performs. Is the boom moving as quickly as it used to? Is the hydraulic oil temperature staying in the normal range? Are the controls as responsive as they were when the machine was new? These subtle changes often signal relief valve problems before complete failure occurs.
Check Hydraulic Oil Regularly: Contaminated or degraded hydraulic oil is the enemy of relief valves. Dirt particles can prevent the valve from seating properly, causing internal leakage. Check your hydraulic oil condition at every service interval. If it looks dark, milky, or has visible particles, change it immediately. Clean oil keeps relief valves working properly.
Monitor Operating Temperature: Overheating damages relief valves faster than almost anything else. If your excavator consistently runs hot, investigate immediately. It might be the relief valve causing the heat, or heat from other sources might be damaging the relief valve. Either way, letting it continue will lead to expensive failures.
Listen to Your Machine: Unusual noises from the hydraulic system deserve attention. Chattering, whining, or squealing sounds can indicate relief valve problems. Don’t ignore these warning signs—they’re telling you something needs attention before it fails completely.
Annual Professional Inspection: Once a year, have a qualified hydraulic technician inspect your relief valves. They can test the cracking pressure, check for internal leakage, and verify that the valves are functioning within specifications. This preventive inspection catches problems early when they’re cheap and easy to fix.
When to Replace Your Relief Valve
Sometimes repair isn’t an option—you need replacement. Here’s how to know when it’s time.
Obvious Failure Signs: If your excavator has completely lost function in a particular circuit, or if hydraulic oil is visibly leaking from the relief valve, replacement is clearly needed. These are emergency situations that require immediate attention.
Persistent Performance Problems: When you’ve checked everything else—hydraulic oil level, filter condition, pump operation—and your excavator still isn’t performing right, the relief valve is often the culprit. If adjusting the pressure setting doesn’t solve the problem, internal wear probably means replacement is necessary.
After Major Contamination Events: If your hydraulic system has been contaminated with dirt or water, relief valves should be replaced even if they seem to be working. Contamination damages the precision surfaces inside the valve, and those surfaces can’t be effectively cleaned once damaged.
Age and Hours: Relief valves don’t last forever. After several thousand operating hours, internal wear accumulates. Even if the valve hasn’t completely failed, replacing it proactively can prevent unexpected breakdowns. Many operators replace relief valves during major hydraulic system overhauls, even if they’re still functioning.
Choosing Between OEM and HFD: Relief valves from OEM or original equipment manufacturers are always an option, however, they are often more expensive than HFD relief valves. HFD relief valves meet or exceed OEM specifications while costing less. For most operators, HFD provides better value without compromising on quality or performance.
The replacement process itself isn’t overly complicated, but it requires proper procedures. The hydraulic system must be completely depressurized before starting work. The old valve is removed, the mounting surface cleaned, and the new valve installed with proper torque specifications. The pressure setting needs to be tested and adjusted to match the excavator’s requirements. Do this after installation.

Your excavator’s relief valves might be small components, but they play an oversized role in protecting your investment. From preventing catastrophic pressure damage to maintaining smooth, consistent operation, these valves are essential for any excavator that needs to perform reliably day after day.
The key takeaways are simple: choose quality relief valves sized correctly for your machine, pay attention to warning signs before they become failures, maintain your hydraulic system properly, and replace relief valves proactively rather than waiting for emergency breakdowns.
HFD Hydraulic offers a complete range of relief valves designed specifically for the demanding conditions excavators face. Whether you’re operating a compact mini excavator or a large production machine, there’s an HFD relief valve engineered to provide reliable pressure protection.
Don’t wait until a failed relief valve leaves you stuck on the job site with expensive repairs and lost productivity. Take a few minutes to inspect your excavator’s relief valves, verify they’re functioning properly, and replace any that show signs of wear or inadequate performance.
Ready to protect your excavator with reliable HFD relief valves? Visit our pressure relief valve catalog at hfdhydraulic.com or contact our technical team for help selecting the right valve for your specific excavator model and application. We’re here to help you keep your machine running at peak performance.