Quick Overview: How to Select a Counterbalance Valve
How do you select the right counterbalance valve for a hydraulic system?
Selecting the right counterbalance valve requires matching five key parameters to the application: load capacity, system-induced pressure characteristics, load dynamics, back pressure variability, and pilot ratio. The wrong selection causes load drift, system instability, excessive heat, or chattering — all of which can be traced back to a mismatch between valve design and application requirements.
Key selection criteria and what they determine:
- Single vs. double counterbalance valve – single for unidirectional loads (vertical cylinders); double for bidirectional loads (cranes, aerial platforms, boom lifts) where load forces can reverse direction
- Pilot ratio (3:1 to 5:1 typical) – higher pilot ratios for steady predictable loads; lower pilot ratios for fluctuating or dynamic loads; incorrect ratio causes chattering or instability on initial movement
- Set pressure (1.3x maximum load pressure) – must exceed maximum load-induced pressure; set too low causes valve to open under load pressure alone, too high wastes energy and causes heat
- Fully balanced valve – required when back pressure from proportional valves or regenerative circuits varies; eliminates pilot pressure instability caused by fluctuating downstream pressure
- Two-stage valve – required for highly dynamic applications with telescopic booms, pneumatic tires, or multiple articulating sections where standard valves cause instability on initial movement
Example
A telescopic handler with pneumatic tires experiences chattering and jerky boom movement when lowering a load — a classic symptom of a standard counterbalance valve being used in a high-instability application. Switching to a two-stage counterbalance valve with a lower pilot ratio eliminates the chatter, as the outer poppet provides initial counterbalancing pressure before the main poppet opens fully.
Summary
Start counterbalance valve selection with load direction (single vs. double), set pressure at 1.3x maximum load pressure, and pilot ratio matched to load stability — then upgrade to fully balanced designs for variable back pressure circuits and two-stage designs for dynamic applications with instability symptoms.
What Are Counterbalance Valves?
Counterbalance valves—sometimes called overcenter valves or load-holding valves—are critical components in hydraulic systems designed to control load position and movement. These specialized valves prevent loads from dropping or drifting when hydraulic pressure isn’t being actively supplied, ensuring both safety and operational precision.
One of their primary advantages is stabilizing loads through careful management of pressure and flow, even in extreme environmental conditions. By reducing instability, these valves significantly enhance both safety standards and productivity across various hydraulic applications.
Where Are Counterbalance Valves Used?

These versatile components serve crucial functions across numerous industries:
Cranes & Hoisting Equipment: Prevent catastrophic load drops during sudden pressure loss
Aerial Work Platforms: Maintain consistent system pressure and enable controlled platform lowering
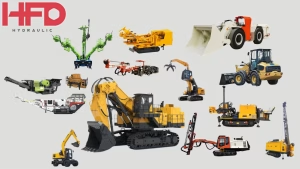
Excavators & Construction Machinery: Secure boom and arm positions to prevent unintended movements
Hydraulic Presses: Maintain precise pressure and prevent ram displacement
Elevators: Act as critical safety mechanisms that prevent free-falling cabins
Industrial Automation: Ensure consistent pressure and eliminate movement disruptions in automated processes
Essential Factors for Selecting the Right Counterbalance Valve
Understanding Load Management Requirements
Counterbalance valves operate between directional controls and cylinder ends (head or rod) to manage loads safely. They provide three distinct functions that ensure successful operation:
Load-Holding Capability
These valves prevent cylinders from experiencing unwanted downward drift—a function particularly critical in aerial platforms. This capability allows operators to set their preferred boom height and maintain that position indefinitely. The load rises through an integral free-flow check valve that permits directional flow to the cylinder while blocking reverse flow.
Load Control Precision
By preventing actuators from exceeding the pump’s speed capacity, counterbalance valves effectively harness and utilize energy generated by the load itself—improving overall system efficiency.
Safety Redundancy
When mounted directly to an actuator, load-holding valves provide critical protection against uncontrolled motion if hydraulic lines fail—an essential safety feature in many applications.
System-Induced Pressure Considerations
Equipment such as wheel loaders, hydraulic excavators, cranes, and telehandlers typically incorporate closed-center directional valves that require counterbalance valves. This design creates unique challenges when the machine encounters resistance (like rocks, soil, or other materials) during operation.
The interaction between closed components can generate significant induced pressure between directional and counterbalance valves. Without proper management, this pressure buildup can cause mechanical damage to the cylinder and related components.
Standard counterbalance valves display a problematic behavior pattern: they initially open but quickly close when pressure builds against the directional valve. Opening these valves requires substantial pilot pressure, and port reliefs on directional valves become functionally inoperative.
Modern Solution: Today’s industry standard addresses this challenge using fully balanced valves with atmospheric drains. While these valves effectively relieve pressure, they require protection against contamination to prevent external leakage.
Managing High System Instability
Engineers frequently encounter challenges with vehicles exhibiting high load dynamics, including:
– Equipment with slender or multiple booms
– Systems with wear pads that create variable frictional forces
– Vehicles with pneumatic tires
Common Examples:
– Concrete pumps with multiple articulating booms
– Rough-terrain forklifts
– Telescopic handlers with pneumatic tires
In telescopic boom systems, hydraulic cylinders function as capacitors that store energy during extension. When a piston reaches its maximum stroke, pressure peaks significantly. The counterbalance valve then resets, seals, and locks this pressure to maintain load control and stability despite variable operating pressures.
During load lowering, stored hydraulic energy signals the counterbalance valve, requiring less pilot pressure for activation. This rapid valve opening releases stored energy, which may temporarily cause instability or jerky movements as the boom retracts—highlighting the importance of proper valve selection and load adjustments for smooth operation.
Advanced Solutions for Dynamic Applications
While many vehicle engineers employ restrictive and semi-restrictive valves in highly dynamic applications, these solutions have significant drawbacks—primarily reduced efficiency and increased heat generation.
Two-Stage Counterbalance Valves: These provide superior stability compared to traditional valves. They maintain counterbalance pressure to prevent energy loss, using:
– A center poppet and inner spring for seamless operation
– An outer poppet that regulates pressure during energy release
– Automatic reseating capability if instability occurs
– Customizable pressure settings for specific application needs
With this design, engineers can establish fixed outer spring pressure while adjusting the inner spring for precise performance tuning. For example, setting the valve to 200 bar (3,000 psi) with counterbalance pressure between 35-70 bar (500-1,000 psi) for optimal operation.
Two-stage valves excel at mitigating sudden instability when cylinder movement begins by providing initial counterbalancing pressure—creating smoother operation in dynamic applications.

Handling Variable Back Pressure
Many proportional hydraulic systems generate back pressure that fluctuates during operation, necessitating specialized counterbalance valve implementation.
Cranes typically utilize meter-out proportional control valves specifically designed to regulate flow and pressure with precision. These systems create constantly varying back pressure between directional and counterbalance valves to ensure smooth operation during all phases of load manipulation.
Regenerative systems further complicate pressure management by redirecting flow from the rod end to the cylinder’s bore side. While this significantly increases extension speed, it creates continuous back pressure fluctuations that present additional challenges for counterbalance valve systems.
When standard or partially-balanced valves are used in these applications, variable back pressure can cause instability by altering the pilot pressure required to open the poppet. For these scenarios, fully balanced relief valves provide superior pressure fluctuation control.
Fully Balanced Valve Advantages
Fully balanced valves utilize pressure from the valve to the spring chamber, but critically, they vent this pressure either:
– To atmosphere
– Through a separate drain port
This venting eliminates pilot pressure variability, resulting in stable counterbalancing regardless of system pressure fluctuations.
For mobile hydraulic applications, four-ported counterbalance valve configurations offer significant advantages over three-ported, atmospherically vented alternatives. The additional port enables proper drainage into the hydraulic reservoir, preventing external contaminants from entering the valve assembly—a common cause of seal deterioration, internal corrosion, and fluid leakage that compromises system performance and longevity.
If three-port fully balanced valves are preferred, consider models with sintered bronze filters for venting. These provide superior protection against spring chamber contamination and hydraulic system integrity.
Pilot Ratio Selection
The pilot ratio significantly impacts valve performance and should be carefully matched to application requirements:
Higher pilot ratios work well with steady, predictable loads
Lower pilot ratios are better suited for fluctuating or unpredictable loads
While pilot ratio doesn’t necessarily affect working pressure (since normal operating pressure typically exceeds the pilot pressure needed for full valve opening), it dramatically influences system stability during rapid load pressure changes.
When load pressure increases unexpectedly, operators must apply additional pilot pressure. Higher pilot-ratio counterbalance valves provide greater mechanical advantage and improved responsiveness with flatter, more linear pressure-response curves. This design enables faster opening when sudden load pressure increases occur, ensuring quicker reaction times, enhanced stability, and smoother operation in high-performance hydraulic systems.
If instability symptoms persist (such as audible squealing or bouncing during initial movement), changing the valve design type may be necessary. Fortunately, most valve designs feature compatible mounting patterns, simplifying retrofitting into existing actuators or manifolds.
Final Recommendations for Optimal Valve Selection
To select the ideal counterbalance valve for your application:
Thoroughly assess critical parameters:
– Load capacity requirements
– System-induced pressure characteristics
– Load dynamics expectations
– Back pressure variability
– Optimal pilot ratio for your specific application
Choose specialized valve types for challenging applications:
– Two-stage valves for highly dynamic applications
– Fully balanced valves for systems with variable back pressure
Ensure system compatibility:
– Verify compatibility with actuator specifications
– Confirm cylinder design integration
– Validate overall hydraulic system design requirements
Implement proper maintenance protocols:
– Regular valve inspection
– Contamination prevention measures
– Leakage monitoring systems
Seek expert consultation for complex applications:
– Hydraulic system specialists can provide application-specific guidance
– Manufacturer guidelines offer valuable selection parameters
– Custom valve configurations may be necessary for unique operational requirements
By carefully considering these factors and working with experienced hydraulic professionals, you can ensure your counterbalance valve selection provides optimal performance, safety, and reliability for your specific application requirements.
For more complex applications, consult hydraulic system experts like HFD Hydraulic or refer to manufacturer guidelines. Custom configurations may be required to meet specific operational needs and we can assist you with that!