What Is a Hydraulic Check Valve?
Quick Overview: Hydraulic Check Valve Selection Guide
How do you select the right hydraulic check valve?
Selecting the right hydraulic check valve requires matching the valve type, pressure rating, cracking pressure, port size, and leakage tolerance to the specific circuit requirements. Standard check valves block reverse flow automatically with no external signal. Pilot-operated check valves (POCVs) add a pilot port that allows controlled reverse flow on demand — making them essential for load holding, cylinder locking, and regenerative circuits where a standard check valve is insufficient.
Main types and when to use each:
- Poppet-type check valve (VUR) – high-pressure circuits requiring reliable low-leakage backflow prevention; rated up to 500 bar
- In-line check valve (SY-RD, SY-RV) – straightforward line installation for pump outlet protection and general backflow prevention
- Bidirectional check valve (VRC) – circuits requiring controlled flow management in both directions
- Single pilot-operated check valve – single-acting cylinder circuits requiring load holding with pilot-controlled release
- Double pilot-operated check valve – double-acting cylinder circuits requiring bidirectional pilot control in one compact body
Example
A crane clamping circuit uses a double pilot-operated check valve to lock the cylinder in position under full load when the control lever is released. When the operator commands retraction, pilot pressure opens the valve — allowing controlled release while the standard check function prevents any unintended drift in the opposite direction.
Summary
Choose a standard hydraulic check valve for passive backflow prevention and pump protection. Upgrade to a pilot-operated check valve when the circuit requires positive load holding, cylinder locking under load, or controlled reverse flow as part of normal system operation.
A hydraulic check valve is the gatekeeper of your hydraulic circuit. Fluid moves through in one direction, and when it tries to reverse, the valve shuts it down automatically. It requires no external signal or manual operation — the valve opens and closes in response to the pressure differential of the fluid itself.
This simple function makes the hydraulic check valve one of the most fundamental components in fluid power engineering. Skip it, and things go wrong fast. A stopped pump or a shifting load is all it takes for pressure to bleed back, actuators to drift, and the whole system to start behaving unpredictably.
Check valves are found in virtually every type of hydraulic application — from mobile construction equipment and industrial machinery to agricultural systems and marine hydraulics.
How a Hydraulic Check Valve Works
The operating principle is straightforward. When inlet pressure exceeds the valve’s cracking pressure (the minimum pressure required to open the valve), the internal mechanism — typically a poppet, ball, or spool — lifts off its seat and allows fluid to flow through. When pressure drops or reverses, the mechanism reseats, blocking flow.
Standard hydraulic check valves are designed to open at relatively low pressure — usually somewhere between 0.3 and 6 bar (about 4.4 to 87 psi), depending on the design and what the application demands. The specific value matters in system design because it affects how quickly the valve responds and how much back-pressure is introduced into the circuit.
Key operating characteristics include:
- Opening response: Near-instantaneous once cracking pressure is reached
- Sealing: Metal-to-metal or elastomer-seated contact, depending on leakage requirements
- Pressure rating: Standard industrial hydraulic check valves are typically rated from 250 bar up to 500 bar and beyond for high-pressure applications
- Flow direction: Always unidirectional in standard check valves
Types of Hydraulic Check Valves
Not all check valves are built the same. Different applications call for different configurations — pressure rating, flow capacity, mounting method, and the level of control you need all factor into which hydraulic check valve actually belongs in your system.
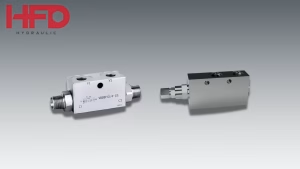
Poppet-type check valves are the most common in hydraulic systems. A conical or spherical poppet seats against a machined orifice to seal the reverse-flow port. They provide reliable, low-leakage sealing and handle high pressures well. HFD’s Poppet Type Check Valve – VUR is a standard example of this design.
Ball-type check valves use a ball bearing as the sealing element. They are simple, compact, and suitable for moderate-pressure hydraulic lines. They are common in low-cost, general-purpose applications.
In-line check valves are body-mounted directly into the hydraulic line, making them easy to install and replace without disturbing the overall circuit layout. HFD’s In-Line Check Valve – SY-RD and Non Return Check Valve – SY-RV fall into this category.
Bidirectional check valves are a specialized variant that allow controlled flow in both directions under certain conditions. HFD’s BidirectionalCheck Valve – VRC serves applications where dual-direction flow management is required.
Direct-operated check valves use a spring-loaded mechanism for positive closure. HFD’s Direct Operated Check Valve – C5V is designed for systems where a defined cracking pressure and reliable reset behavior are needed.
Pilot-operated check valves (POCVs) are an advanced variant discussed in detail in the next section.
The Pilot-Operated Check Valve: When Basic Isn’t Enough
A standard hydraulic check valve does one thing well: it blocks reverse flow. But in many applications, you actually need to allow reverse flow under specific, controlled conditions — for example, when releasing a load from a locked cylinder or retracting an actuator in a holding circuit.
This is where the pilot-operated check valve (POCV) becomes essential.
A pilot-operated check valve functions like a standard check valve in the forward direction. The difference is a separate pilot port. When pilot pressure is applied to this port, it mechanically opens the poppet against the return flow, allowing fluid to pass in the normally blocked reverse direction. Remove the pilot signal, and the valve reseals.
This makes POCVs the preferred choice in applications that require load holding with on-demand release, such as:
- Hydraulic cylinders holding suspended loads (cranes, lifts, forestry equipment)
- Clamping circuits in manufacturing presses and injection molding machinery
- Mobile equipment where actuator drift under load is a safety concern
- Regenerative circuits that require controlled reverse flow
Single vs. double pilot-operated check valves In single-acting circuits — where only one direction requires controlled reverse flow — a single pilot-operated check valve is sufficient. It provides a pilot-controlled opening in one direction while maintaining standard check behavior in the other.
In double-acting cylinder circuits, where both ports need bidirectional pilot control, a double pilot-operated check valve houses two pilot-controlled check mechanisms in a single body. This eliminates the need for two separate valves and reduces plumbing complexity.
HFD Hydraulic manufactures both configurations across a range of sizes, pressure ratings, and mounting styles:
- Single Pilot Check Valves — for single-acting cylinder circuits requiring load holding with pilot-controlled release
- Double Pilot Check Valves — for double-acting cylinder circuits requiring bidirectional pilot control in a compact, single-body design
The full range of HFD’s pilot-operated check valves — including DIN 2352 and DIN 2353 connection types, bolt-connection variants, shut-off configurations, and flanged designs — is available on the HFD Pilot Operated Check Valves product page.
HFD Hydraulic offers a full range of pilot-operated check valves for both single and double-acting circuits. Browse the Single Pilot Check Valves and Double Pilot Check Valves to find the right configuration for your application.
Standard Check Valve vs. Pilot-Operated Check Valve: Key Differences
| Feature | Standard Check Valve | Pilot-Operated Check Valve |
| Flow direction | One-way only | One-way + reverse on pilot signal |
| Reverse flow control | Not possible | Yes, via pilot pressure |
| Complexity | Simple | More complex, requires pilot line |
| Load holding | Passive (pressure-dependent) | Active (positive mechanical lock) |
| Typical applications | Backflow prevention, pump protection | Load holding, locking cylinders, regenerative circuits |
| Cost | Lower | Higher |
The right choice depends on whether your application requires a strict one-way flow only or whether controlled reverse flow is part of normal system operation.

How to Select the Right Hydraulic Check Valve
Choosing the correct hydraulic check valve for an application requires matching several technical parameters to system requirements. The following factors should be evaluated:
1. Flow rate and port size Match the valve’s rated flow capacity (typically expressed in L/min or GPM) to the system’s maximum flow. Undersizing causes excessive pressure drop; oversizing can affect response sensitivity.
2. Operating pressure Ensure the valve’s maximum working pressure rating meets or exceeds system peak pressure. High-pressure circuits (above 300 bar) require valves rated accordingly.
3. Cracking pressure Select a cracking pressure appropriate to the circuit. In pump outlet protection, a higher cracking pressure may be acceptable. In servo or low-back-pressure circuits, a low cracking pressure minimizes energy loss.
4. Mounting and connection type In-line (pipe-thread or compression fitting) or manifold-mounted configurations each have installation implications. DIN 2353 and DIN 2352 compression-fitting standards are common in European specification hydraulic circuits.
5. Leakage tolerance Metal-seated poppets provide near-zero leakage but are sensitive to contamination. Elastomer-seated designs offer better sealing against minor contamination but have a lower pressure and temperature ceiling.
6. Temperature range Seal materials must be compatible with both the hydraulic fluid type and the operating temperature range of the application.
7. Does the circuit require load holding with controlled release? If yes, a pilot-operated check valve is the appropriate choice — not a standard hydraulic check valve.
HFD Hydraulic carries several standard check valve configurations suited to different circuit requirements. The Poppet Type Check Valve – VUR is a reliable choice for high-pressure applications, while the In-Line Check Valve – SY-RD offers straightforward line installation. For circuits that require flow management in both directions, the Bidirectional Check Valve – VRC is worth considering.
Common Applications
Hydraulic check valves appear across virtually every sector that uses fluid power:
Construction and mobile equipment: Used in pump outlet lines to prevent fluid siphoning when the engine stops, and in boom and arm circuits to prevent actuator drop.
Industrial machinery: Found in clamping, pressing, and lifting circuits to maintain pressure after the pump unloads, reducing energy consumption during hold phases.
Agricultural equipment: Used in cylinder circuits on loaders, balers, and implements to maintain position without continuous pump engagement.
Material handling: Integrated into scissor lifts, pallet jacks, and forklifts, often in combination with pilot-operated variants to allow controlled lowering under load.
Marine and offshore: Applied in deck machinery, stabilizer systems, and hatch cover drives where reliable one-way flow control is required in corrosive environments.
Sourcing Considerations for Wholesale Buyers
For procurement teams and distributors, hydraulic check valves are a high-turnover line item — but specification errors are common and costly. A few sourcing principles to keep in mind:
Standardization reduces inventory complexity. Where possible, consolidate around a small number of port sizes, cracking pressures, and connection types. This reduces the number of SKUs your stocking program needs to carry.
Verify pressure ratings against system maximums, not averages. Pressure spikes in hydraulic circuits can exceed steady-state values significantly. A valve rated for average operating pressure may fail during transient conditions.
Material compatibility is non-negotiable. Body materials (carbon steel, stainless steel, brass) must be matched to the fluid type and environment. A carbon steel valve installed in a marine or high-humidity environment without appropriate surface treatment will corrode.
Pilot-operated check valves require attention to pilot pressure ratios. The pilot pressure needed to open a POCV against a given load pressure is determined by the valve’s pilot ratio (typically 1:3 to 1:4.5). This must be verified against the available pilot supply in the circuit.
HFD Hydraulic’s full range of hydraulic check valves and pilot-operated check valves is available for inquiry directly through the HFD team.
Summary
The hydraulic check valve is one of the most fundamental components in fluid power — simple in concept, but consequential in application. Selecting the right type, understanding cracking pressure and flow capacity, and knowing when a standard check valve is insufficient (and a pilot-operated check valve is needed) are the practical decisions that determine whether a hydraulic circuit performs reliably or becomes a maintenance problem.
For systems that need more than passive backflow prevention — load holding with controlled release, cylinder locking under load, or double-acting circuit protection — HFD’s single and double pilot-operated check valves provide the controlled functionality that standard hydraulic check valves cannot.