Industrial hydraulic systems face a critical challenge: maintaining optimal pressure levels across different circuits and components. When a system operates at maximum pressure throughout, sensitive components risk damage, energy efficiency plummets, and equipment lifespan decreases. The solution lies in a precisely engineered component called a hydraulic pressure reducing valve.
A hydraulic pressure reducing valve automatically reduces higher inlet pressure to a steady, controlled outlet pressure in specific branches of the system. These specialized valves protect sensitive components from overpressure damage, improve system efficiency, and enable multiple circuits to operate at different pressure levels from a single pump. Understanding how hydraulic pressure reducing valves work and when to apply them is essential for engineers, equipment designers, and maintenance professionals working with industrial machinery.
In this comprehensive guide, we’ll explore everything you need to know about hydraulic pressure reducing valves, from their operating principles and types to practical applications and selection criteria, helping you optimize your hydraulic system performance.
Quick Overview: Hydraulic Pressure Reducing Valve for Industrial Machinery
What is a hydraulic pressure reducing valve and how does it work in industrial machinery?
A hydraulic pressure reducing valve automatically reduces higher inlet pressure to a controlled, stable outlet pressure in secondary circuit branches — protecting sensitive components from overpressure damage while allowing one pump to supply multiple circuits at different pressure levels. Unlike relief valves that are normally closed and sense upstream pressure, pressure reducing valves are normally open and sense downstream pressure, throttling flow to maintain the target outlet pressure regardless of inlet fluctuations.
Key types and specifications (HFD VRPRL series):
- Direct-acting – compact, lower cost, suited to flows up to 20 L/min in auxiliary and pilot circuits; simpler maintenance but higher pressure override at elevated flow
- Pilot-operated – handles high-capacity industrial circuits with minimal pressure override; preferred for excavators, presses, and machine tool applications requiring precision across the full flow range
- VRPRL 38 – 20 L/min, G3/8 ports, aluminium body to 210 bar or steel body to 350 bar; 0.83–1.75 kg
- VRPRL 12 – 50 L/min, G1/2 ports, same pressure ratings; suited to excavator steering, loader transmission controls, and industrial power units
- External drain port required – must connect directly to reservoir with no back pressure; blocked drain causes outlet pressure to rise to inlet levels
Example
A hydraulic press performing metal forming requires 3,000 PSI for the forming cylinders but only 500 PSI for the workpiece clamping circuit. A VRPRL pressure reducing valve installed in the clamping branch maintains 500 PSI downstream regardless of main system pressure — protecting the workpiece from damage without requiring a second pump or separate power unit.
Summary
A hydraulic pressure reducing valve is the correct component when a secondary circuit needs to operate at lower pressure than the main system — always specify based on downstream flow requirement, required pressure range, body material for pressure rating, and ensure a properly drained external drain line for correct operation.
Understanding Hydraulic Pressure Reducing Valves
A hydraulic pressure reducing valve maintains lower pressure in secondary branches of a hydraulic system while the main system pressure is determined by a relief valve or pump setting. Unlike relief valves that protect against overpressure by dumping fluid to tank, pressure reducing valves actively regulate downstream pressure during normal operation.
The fundamental design consists of three main components. The valve housing encapsulates all working parts and provides the fluid flow path. A pressure spring maintains the spool position and determines the pressure setpoint. The piston spool moves to open or close valve ports, regulating fluid flow based on downstream pressure feedback.
Hydraulic pressure reducing valves are unique among pressure control devices because they are normally open. This means fluid flows freely through the valve until the set pressure is reached downstream. All other pressure valves, including relief and counterbalance valves, are normally closed and only activate under specific conditions.
Another distinguishing characteristic is that pressure reducing valves sense pressure downstream of themselves, not upstream. A relief valve monitors inlet pressure and opens when that pressure exceeds its setting. A hydraulic pressure reducing valve monitors outlet pressure and throttles flow to maintain that pressure at the desired level regardless of inlet pressure fluctuations.
The valve operates through a spring-loaded mechanism that responds to downstream pressure changes. When downstream pressure is below the setpoint, the valve remains fully open, allowing maximum flow. As downstream pressure approaches the setpoint, the spool begins to throttle, restricting flow to maintain the target pressure. If downstream pressure tries to exceed the setpoint due to external forces or thermal expansion, the valve closes further and bleeds excess pressure through a drain line to tank.
When Industrial Systems Need Pressure Reduction
Multiple scenarios in industrial hydraulics demand pressure regulation. Understanding these applications helps engineers recognize when to specify hydraulic pressure reducing valves in system design.
Multi-actuator circuits frequently require different operating pressures. Consider a hydraulic press with both high-force forming cylinders and low-force clamping cylinders. The forming operation might require 3000 psi while clamping needs only 500 psi to avoid damaging workpieces. Rather than sizing all cylinders for maximum pressure or installing multiple pumps, engineers install a hydraulic pressure reducing valve in the clamping circuit to provide the lower pressure required.
Machine tool applications often incorporate pressure reduction for precise control. CNC lathes use hydraulic chucks that must secure workpieces with consistent clamping force. Excessive pressure damages delicate parts or causes dimensional inaccuracy. A hydraulic pressure reducing valve maintains stable clamping pressure regardless of main system pressure variations during cutting operations.
Construction and earthmoving equipment rely heavily on pressure reduction. Excavators, wheel loaders, and bulldozers use high pressure for primary work functions like digging and lifting. However, auxiliary functions such as steering, cab tilt, and attachment operation require lower pressure. Installing hydraulic pressure reducing valves in these secondary circuits protects components while improving operator control and system efficiency.
Mobile equipment brake and clutch systems represent critical applications. These systems demand precise, consistent pressure for safe operation. Main hydraulic system pressure can vary significantly based on engine speed and load demand. A hydraulic pressure reducing valve ensures brake and clutch actuation occurs at the correct pressure every time, regardless of source pressure fluctuations.
Energy efficiency provides another compelling reason for pressure reduction. Operating circuits at unnecessarily high pressure wastes energy through heat generation and increased parasitic losses. By reducing pressure in circuits that don’t require maximum force, hydraulic pressure reducing valves cut energy consumption, reduce cooling requirements, and extend component life throughout the system.
Types of Hydraulic Pressure Reducing Valves
Hydraulic pressure reducing valves come in two fundamental designs, each suited to specific flow requirements and application demands. Understanding the differences helps engineers select the optimal valve type.
Direct-acting pressure reducing valves feature simple, compact construction ideal for lower-capacity applications. The valve consists of a spring-loaded spool that responds directly to downstream pressure. When outlet pressure rises above the spring setting, the spool moves to restrict flow, creating a pressure drop across the valve. These valves typically handle flows up to 20 gallons per minute and work best in circuits with relatively steady demand.
The advantages of direct-acting valves include compact size, lower cost, and straightforward adjustment. Their simple design means fewer parts to maintain and good reliability in clean fluid conditions. However, they exhibit limitations in high-flow applications. Pressure override increases with flow rate, meaning actual outlet pressure rises above the setpoint as flow increases. They also tend to be more sensitive to inlet pressure variations and may experience stability issues at very low flows.
Pilot-operated pressure reducing valves provide superior performance for industrial applications requiring high flow capacity and precise pressure control. These valves use a pilot assembly to sense downstream pressure and control the main spool position hydraulically. The pilot valve directs pressure to a control chamber, modulating main valve opening based on outlet pressure feedback.
The pilot-operated design offers significant advantages. It maintains accurate outlet pressure across a wide flow range, from zero flow to maximum rated capacity. Pressure override remains minimal even at high flows. The valve responds quickly to load changes and provides excellent stability. These characteristics make pilot-operated hydraulic pressure reducing valves the preferred choice for demanding industrial applications.
Pilot-operated valves come in different configurations. Some incorporate integral pressure relief to protect against downstream overpressure from external sources. Others include check valves allowing free reverse flow, useful in circuits where actuators need to return quickly without restriction. Adjustable pilot assemblies enable field tuning to match specific application requirements.
Cartridge-style pressure reducing valves offer installation flexibility and space savings. These valves install directly into manifold blocks, eliminating the need for external piping between components. Cartridge hydraulic pressure reducing valves are particularly popular in mobile equipment and compact industrial machinery where space is limited.
HFD Hydraulic specializes in manufacturing high-quality pressure reducing valves specifically designed for demanding industrial and mobile equipment applications. Their product line combines proven hydraulic technology with modern manufacturing precision to deliver reliable pressure control solutions.
VRPRL Series: Pressure Reducing Valve with Relieving
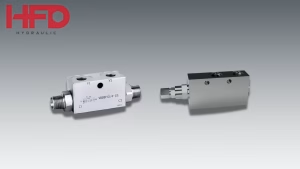
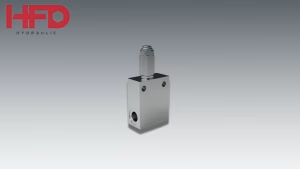
The HFD VRPRL series represents the company’s flagship hydraulic pressure reducing valve line, engineered to maintain consistent downstream pressure while automatically relieving excess pressure to prevent system overload. This dual-function design protects sensitive components and enhances overall system safety.
The VRPRL series comes in two body material options to match application requirements. The aluminum body version handles pressures up to 210 bar (3,050 psi), ideal for mobile equipment and weight-sensitive applications. The steel body construction supports pressures up to 350 bar (5,100 psi) for demanding industrial applications requiring maximum strength and durability.
HFD offers the VRPRL in two flow capacities. The VRPRL 38 size handles nominal flows of 20 liters per minute (5.3 US GPM) with G3/8 or SAE8 port connections, perfect for compact auxiliary circuits in agricultural machinery, material handling equipment, and small industrial presses. The larger VRPRL 12 size accommodates 50 liters per minute (13.2 US GPM) with G1/2 or SAE10 ports, suitable for higher-capacity applications like excavator steering, loader transmission controls, and industrial power units.
Both valve sizes weigh remarkably little considering their robust construction. The VRPRL 38 weighs just 0.83 kg (1.83 lb) in aluminum or 1.75 kg (3.86 lb) in steel. The VRPRL 12 weighs 1.20 kg (2.64 lb) in aluminum or 2.58 kg (5.69 lb) in steel, making installation straightforward even in space-constrained environments.

VRPRL/U Series: Enhanced Pressure Control
The VRPRL/U variant offers the same pressure reducing and relieving capabilities with an optimized internal configuration for applications demanding enhanced stability and response. This model maintains identical pressure ratings, flow capacities, and port configurations as the standard VRPRL, giving engineers flexibility in matching valve characteristics to specific circuit dynamics.
Operating temperature range spans -40°C to 100°C (-40°F to 212°F), accommodating extreme environmental conditions found in outdoor mobile equipment and industrial facilities with minimal climate control. The valves work with mineral-based hydraulic oils across viscosity ranges from 10 to 200 cSt, compatible with most industrial hydraulic fluids.
HFD designs these hydraulic pressure reducing valves to maintain ISO 18/16/13 cleanliness standards, suitable for modern hydraulic systems with tight tolerances. The integral relieving function automatically diverts excess downstream pressure back to tank, eliminating the need for separate relief valves in many applications and reducing system complexity.
Quality control at HFD ensures every VRPRL and VRPRL/U valve meets performance specifications before shipment. Each valve undergoes pressure testing at maximum rated pressure, leakage verification on all ports and sealing surfaces, and flow testing across the operating range. This rigorous process gives engineers confidence that catalog performance translates directly to field operation.
The VRPRL series incorporates practical features simplifying installation and maintenance. Field-adjustable pressure settings allow calibration without disassembly. External drain ports facilitate proper tank connection. Port configurations follow common industrial standards for direct replacement compatibility. Multiple mounting orientations provide installation flexibility in crowded manifolds or tight equipment spaces.
For OEM customers and equipment manufacturers, HFD offers technical support for valve selection, circuit design consultation, and application-specific recommendations. Their engineering team assists in determining optimal valve sizing, pressure settings, and port configurations to match specific machinery requirements.
Installation and Maintenance Best Practices
Installing hydraulic pressure reducing valves correctly helps them work better and last longer. Sticking to best practices helps you avoid the usual problems that can mess up your system.
Always install pressure reducing valves in the correct orientation. Most valves have arrows showing which way the fluid should flow—usually from the inlet to the outlet. Reverse installation renders the valve non-functional. It won’t work if you install it backwards. Put the valve somewhere you can easily reach it when you need to adjust or service it. Vibration-prone locations should be avoided or isolation mounts used to prevent fatigue damage.
The drain port connection is critical for proper operation. Hydraulic pressure reducing valves must have an external drain line connected to the reservoir with no back pressure. Never connect the drain to a line with restriction or pressure. Make sure the drain line is at least as big as the valve’s drain port, and slope it gently downward toward the tank. Inadequate drainage causes outlet pressure to rise above the setpoint, negating the valve’s function.
Install pressure gauges at both inlet and outlet ports for commissioning and troubleshooting. Permanent gauge installations help maintenance personnel quickly verify valve operation during routine checks. Use gauges with ranges appropriate to expected pressures. A gauge with too high a range won’t provide adequate resolution for accurate readings.
Adjust the hydraulic pressure reducing valve after installation with the system operating under normal flow conditions. Set outlet pressure while actuators are moving at typical speeds, not static. This ensures proper pressure during actual work cycles. Make adjustments gradually, allowing the system to stabilize between changes. Lock the adjustment mechanism after achieving the desired setpoint to prevent inadvertent changes during operation.
Filtration protects pressure reducing valves from contamination damage. Install system filtration upstream of all pressure control valves. Maintain fluid cleanliness to ISO 18/16/13 or better for reliable valve operation. Contamination damages sealing surfaces, causes erratic operation, and eventually leads to valve failure. Regular filter element changes and periodic fluid analysis prevent contamination-related problems.
Routine maintenance extends valve life and maintains system performance. Inspect external drain lines for leakage and proper flow to tank. Check adjustment lock mechanisms for security. Monitor pressure gauge readings during operation to detect valve drift or malfunction early. Many industrial facilities incorporate pressure check procedures into preventive maintenance schedules to catch degradation before it causes downtime.
Common Applications Across Industries
Hydraulic pressure reducing valves serve critical functions across diverse industrial sectors. Understanding typical applications helps engineers recognize opportunities to improve system performance through proper pressure control.
Manufacturing operations use pressure reduction extensively. Injection molding machines employ hydraulic pressure reducing valves to control mold clamping force independently of injection pressure. Press brakes in metal fabrication regulate back gauge positioning pressure separately from forming ram pressure. Assembly line automation applies reduced pressure for part feeding, clamping, and fixture actuation while maintaining high pressure for primary work functions.
Construction equipment relies on multiple pressure zones for efficient operation. Excavators use high pressure for bucket and boom cylinders but reduced pressure for swing brake release and pilot controls. Wheel loaders maintain maximum pressure for lift and tilt functions while operating auxiliary hydraulics at lower pressure. Hydraulic pressure reducing valves enable this multi-pressure architecture from a single pump, reducing system complexity and cost.
Agricultural machinery incorporates pressure reduction in numerous applications. Tractors use reduced pressure for implement positioning while maintaining high pressure for three-point hitch lift capacity. Combine harvesters regulate header float pressure independently of drive system pressure. Self-propelled sprayers control boom height and fold cylinders at reduced pressure while operating the high-pressure pump for chemical application.
Material handling equipment benefits from precise pressure control. Forklifts use hydraulic pressure reducing valves in steering circuits to provide consistent operator feel regardless of engine speed or hydraulic system load. Overhead cranes regulate hoist brake release pressure for smooth, controlled load handling. Conveyor systems employ reduced pressure for accumulation and product handling while maintaining high pressure for drive functions.
Testing and simulation equipment requires stable, repeatable pressure conditions. Hydraulic test stands use pressure reducing valves to subject components to specific pressure levels during qualification testing. Automotive brake testing equipment relies on precise pressure control to simulate real-world brake actuation. Aerospace component testing demands extremely stable reduced pressure, often with multiple hydraulic pressure reducing valves creating several test zones from one high-pressure source.

Troubleshooting Common Issues
Even properly selected and installed hydraulic pressure reducing valves can develop problems. Knowing what usually goes wrong and why makes it easier to figure out the problem and get things running again.
If the outlet pressure is running higher than it should be, there’s probably something wrong with the drain line. Check for restricted, plugged, or pressurized drain lines. Check that the drain goes straight to the tank below the fluid level with nothing blocking it along the way. Look for crushed hoses or plugged fittings. If the drain is blocked, the valve can’t dump the extra pressure, so the outlet pressure climbs up to match the inlet.
Outlet pressure lower than setpoint often results from worn or damaged internal sealing. As valve spools wear, internal leakage increases, causing pressure drop. This typically develops gradually over thousands of operating hours. Contaminated fluid accelerates wear. Inspect system filtration and fluid condition. Valve rebuilding or replacement restores proper operation.
Erratic outlet pressure fluctuation points to contamination or air in the system. Dirt particles lodge between the spool and bore, causing the valve to stick intermittently. Air bubbles create compressibility, leading to unstable pressure control. Check system filtration, drain lines for siphoning air, and reservoir level. Flush the system and replace hydraulic fluid if heavily contaminated.
Excessive noise from the hydraulic pressure reducing valve indicates cavitation or turbulent flow. Cavitation occurs when pressure drops below fluid vapor pressure, causing bubble formation and collapse. Ensure adequate inlet pressure and check for restrictions upstream. Verify the valve isn’t oversized for actual flow rates. Noise can also result from resonance in piping. Add dampening, change pipe routing, or install isolation mounts.
Slow system response with pressure reducing valve installed suggests undersized valve capacity. If the valve throttles excessively to maintain outlet pressure, flow to downstream actuators becomes restricted. This manifests as slow cylinder speeds or reduced actuator force. Calculate actual system flow requirements and verify valve capacity. Upgrade to a larger valve if needed. Also check for partially closed isolation valves or clogged filters causing artificial restriction.
Maximizing Industrial System Performance
Hydraulic pressure reducing valves play an essential role in modern industrial hydraulics, enabling engineers to optimize system performance, improve energy efficiency, and protect sensitive components. These valves allow multiple circuits to operate at their ideal pressure levels from a single hydraulic power source, reducing complexity and cost compared to multiple pump solutions.
Proper valve selection requires careful analysis of flow requirements, pressure ranges, and application demands. Direct-acting hydraulic pressure reducing valves serve well in compact applications with moderate flow. Pilot-operated designs handle high-capacity industrial circuits where precision and stability are paramount. Consider environmental factors, fluid compatibility, and maintenance access during the selection process.
HFD Hydraulic pressure reducing valves deliver the performance and reliability that demanding industrial applications require. With proven designs, quality construction, and comprehensive technical support, HFD provides pressure control solutions for construction equipment, manufacturing machinery, agricultural implements, and material handling systems. Their valves meet the rigorous demands of industrial hydraulics while offering the flexibility to adapt to custom requirements.
Whether designing new equipment, upgrading existing machinery, or troubleshooting performance issues, proper application of hydraulic pressure reducing valves enhances system capability and longevity. These valves protect expensive components, improve operator control, reduce energy waste, and enable sophisticated multi-pressure hydraulic architectures that would otherwise require complex, costly alternatives.
Contact HFD Hydraulic today to discuss your pressure reducing valve requirements and discover how their engineered solutions can enhance your hydraulic system’s efficiency, reliability, and performance across your industrial equipment applications.

Frequently Asked Questions
What is the difference between a pressure reducing valve and a pressure relief valve? A hydraulic pressure reducing valve actively regulates outlet pressure during normal operation by throttling flow, while a relief valve only opens when pressure exceeds a setpoint to protect the system. Reducing valves are normally open and sense downstream pressure; relief valves are normally closed and sense upstream pressure.
Can I use a pressure reducing valve in reverse flow direction? Standard hydraulic pressure reducing valves block reverse flow unless they incorporate an integral check valve. If your application requires reverse flow, specify a pressure reducing valve with built-in check valve or install a separate check valve in parallel. Always verify the valve datasheet for reverse flow capability.
Why does my pressure reducing valve need a drain line? The drain line allows the valve to bleed off excess downstream pressure to tank when regulating. Without proper drainage, outlet pressure will rise to inlet pressure levels, defeating the valve’s purpose. The drain must connect directly to tank with no back pressure or restrictions.