Quick Overview: Hydraulic Relief Valve
What is a hydraulic relief valve?
A hydraulic relief valve is a safety component that protects hydraulic systems from destructive overpressure by opening when pressure exceeds a preset limit, allowing excess fluid to bypass to the reservoir. Unlike valves that control flow direction or volume, its sole purpose is pressure protection — keeping the system operating within safe limits regardless of load changes or malfunctions.
Main types of hydraulic relief valves:
- Direct-acting – simple spring-loaded design with quick response; handles flow rates up to 40 GPM and pressures up to 5,000 PSI, ideal for smaller systems
- Pilot-operated – uses a small pilot valve to control a larger main valve, handling flow rates up to 1,000+ GPM with precise regulation in larger systems
- Adjustable – allows operators to modify the pressure setpoint via a threaded screw, suited for systems with changing pressure requirements
- Inline – mounts directly in the hydraulic line for localized protection of specific circuit branches or components, common in mobile equipment
Example
In an excavator, a hydraulic relief valve protects the boom and bucket circuits from sudden pressure spikes when the bucket strikes an immovable object — opening instantly to divert excess fluid to the reservoir and preventing hose bursts or cylinder damage.
Summary
A hydraulic relief valve is the last line of defense against overpressure, protecting pumps, cylinders, hoses, and seals from damage while ensuring safe and reliable system operation across mobile, industrial, and high-pressure applications.
What is a Hydraulic Relief Valve?
A hydraulic relief valve is an important safety component designed to protect hydraulic systems from possible destructive overpressure conditions.. Acting as an automatic pressure control device, it opens when system pressure exceeds a predetermined setpoint, allowing excess hydraulic fluid to bypass to the reservoir or return line. This avoids devastating system failures, equipment damage, and potential safety hazards.
Unlike other valve types that primarily control flow direction or volume, a hydraulic relief valve serves as the ultimate pressure guardian, ensuring your hydraulic system operates within safe parameters regardless of load variations, temperature changes, or system malfunctions.
How a Hydraulic Relief Valve Works
The fundamental operating principle of a hydraulic relief valve centers on pressure-responsive flow diversion. When system pressure remains below the valve’s set point, the valve stays closed, allowing normal fluid circulation. However, once pressure surpasses the limit, the valve opens proportionally to redirect the extra fluid away from the main circuit.
This pressure-sensing mechanism typically employs a spring-loaded poppet or spool that responds to hydraulic force. As pressure builds against the valve component, it overcomes the spring force. This created an opening that allows fluid to escape. The valve regulates its opening size based on pressure gap, providing precise pressure control while maintaining system efficiency.
The beauty of this system lies in its automatic operation—no external power source or manual intervention is required. The hydraulic relief valve constantly monitors system pressure and responds immediately to pressure spikes. This ensures safe and efficient system operation even under quick-changing load conditions.
Types of Hydraulic Relief Valves
Direct-Acting Relief Valves

| DIRECT ACTING PRESSURE RELIEF VALVE – VMD20 | CETOP STANDARD WITH DIRECT ACTING PRESSURE RELIEF VALVE – PBL | ANTI-SHOCK TYPE DIRECT-ACTING, WITH ANTI CAVITATION PRESSURE RELIEF VALVE – VAA-RU-DL |
Direct-acting relief valves have a simple, robust design where system pressure acts directly against a spring-loaded valve element. These valves are reliable and have quick response times that makes them ideal for smaller hydraulic systems or applications requiring immediate pressure response. They typically handle flow rates up to 40 GPM and pressures up to 5,000 PSI.
Pilot-Operated Relief Valves

| PILOT OPERATED ELECTRIC VENTING PRESSURE RELIEF VALVE – VMP/VE | PILOT OPERATED PRESSURE RELIEF VALVE – VMPP/B/L |
Pilot-operated relief valves employ a small pilot valve to control a larger main valve, providing better control accuracy and higher flow capacity. The pilot stage senses system pressure and controls the main valve’s operation, allowing these valves to handle significantly higher flow rates (up to 1,000+ GPM) while maintaining precise pressure regulation. They are needed in larger hydraulic systems where accurate pressure control is crucial.
Adjustable Hydraulic Pressure Relief Valve
An adjustable hydraulic pressure relief valve allows operators to modify the pressure setpoint according to system requirements. This flexibility is very important in applications where pressure requirements change based on operating conditions, load variations, or different operational modes. The adjustment mechanism usually uses a threaded screw that increases or decreases spring preload, affecting the valve’s pressure directly.
Adjustability becomes crucial in systems that operate multiple attachments with different pressure requirements, seasonal applications with varying demands, or during system commissioning and testing phases where optimal pressure settings need determination through actual operation.
Inline Hydraulic Pressure Relief Valve
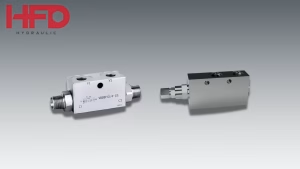
An inline hydraulic pressure relief valve mounts directly in the hydraulic line, providing localized pressure protection exactly where needed. These valves stand out in applications that require pressure protection for specific circuit branches, individual actuators, or critical system components. Their compact design and direct installation feature make them ideal for mobile equipment, where space limitations and weight concerns are paramount.
Inline configurations offer some advantages like reduced plumbing complications, faster pressure response due to proximity to protected parts, and the capacity to provide customized pressure settings for different circuit branches within the same system.
Applications of Hydraulic Relief Valves
Mobile Equipment Applications

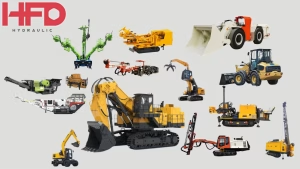
Construction machinery, agricultural equipment, and material handling vehicles rely heavily on hydraulic relief valves for safe operation. In excavators, these valves protect boom, bucket, and swing circuits from pressure spikes during sudden load changes or when hitting immovable objects. Agricultural tractors use relief valves to protect implement circuits, three-point hitch systems, and power steering components from damage during field operations.
Industrial Machinery Applications

Manufacturing facilities employ hydraulic relief valves in injection molding machines, hydraulic presses, and automated assembly equipment. These applications often require precise pressure control to maintain product quality while protecting expensive machinery from pressure-related damage. Relief valves ensure consistent performance during varying production demands and protect against pressure buildup during emergency stops.
High-Pressure Environment Applications

Oil and gas operations, mining equipment, and heavy industrial applications operate at extreme pressures where relief valve performance becomes critical for both safety and equipment protection. These environments demand relief valves capable of handling pressures exceeding 10,000 PSI while maintaining accurate pressure control and reliable operation in harsh conditions including extreme temperatures, corrosive environments, and continuous duty cycles.
Key Considerations When Selecting a Hydraulic Relief Valve
Pressure Rating and Flow Capacity
Selecting the appropriate pressure rating requires careful analysis of maximum system pressure plus a safety margin. The valve should be rated for at least 1.25 times the maximum expected system pressure to prevent premature opening during normal pressure variations. Flow capacity must accommodate the full pump output plus any additional flow from system compression or thermal expansion.
Material Compatibility
Hydraulic fluid compatibility directly affects valve longevity and performance. Petroleum-based fluids work well with standard steel and cast iron valve bodies, while synthetic fluids may require specialized sealing materials. Water-based fluids demand corrosion-resistant materials like stainless steel or specialized coatings to prevent degradation.
Size and Installation Requirements
Physical size constraints often dictate valve selection, particularly in mobile applications where space and weight are limited. The installation type—whether tank-mounted, manifold-mounted, or inline hydraulic pressure relief valve configuration—affects both performance and maintenance accessibility. Consider service access requirements and the impact of valve location on system response time.
Benefits of Using a Hydraulic Relief Valve
Preventing Catastrophic System Failures
The primary benefit of hydraulic relief valves lies in their ability to prevent system destruction from overpressure conditions. Without proper pressure protection, hydraulic systems can experience component failures ranging from seal blowouts and hose bursts to complete pump or cylinder destruction. These failures frequently create dangerous situations and result in costly downtime, repairs, and potential injury.
Enhancing Equipment Longevity
Consistent pressure control significantly extends component life throughout the hydraulic system. By avoiding pressure spikes and maintaining ideal operating conditions, relief valves lessen wear on pumps, cylinders, valves, and sealing components. This protection means longer service intervals, reduced maintenance costs, and improved system reliability.
Supporting Consistent Hydraulic Pressure Control
Modern hydraulic systems demand precise pressure control for optimal performance. Relief valves provide the foundation by establishing maximum system pressure limits and maintaining consistent operating conditions. This stability allows other system components to operate within their design limits, improving overall system efficiency and performance.
Installation Tips for Hydraulic Relief Valves
Best Practices for System Positioning
Install relief valves as close as possible to the pressure source to minimize pressure spikes and ensure rapid response to overpressure conditions. For inline hydraulic pressure relief valve installations, position the valve upstream of critical components requiring protection. Avoid installing relief valves in dead-end circuits or locations where thermal expansion could cause pressure buildup without flow circulation.
Ensure adequate clearance around the valve for maintenance access and consideration of fluid discharge during valve operation. The discharge port should connect to the reservoir or return line with minimal back pressure to prevent interference with valve operation.
Common Installation Mistakes to Avoid
Never install relief valves downstream of restrictive components like flow control valves or small orifices, as this can prevent proper valve operation. Avoid using relief valves as primary flow control devices, as this leads to energy waste and excessive heat generation. Don’t ignore valve orientation requirements—many relief valves must be installed in specific positions for proper operation.
Ensure proper pipe sizing for both inlet and outlet connections. Undersized connections can create pressure drops that affect valve performance and accuracy. Always use appropriate thread sealants or O-ring seals to prevent external leakage while avoiding contamination of the hydraulic fluid.
Maintenance and Troubleshooting
Signs of a Failing Hydraulic Pressure Relief Valve
Recognizing early warning signs prevents system failures and costly repairs. Pressure spikes beyond normal operating ranges often indicate relief valve problems, whether from contamination, wear, or adjustment issues. External leakage around the valve body suggests seal wear or improper installation, while internal leakage may cause pressure drops and system inefficiency.
Unusual noise during valve operation, including chattering or squealing, typically indicates contamination, wear, or improper adjustment. Temperature increases in the relief valve area suggest internal leakage and energy waste that requires immediate attention.
Routine Maintenance Checks
Monthly visual inspections should include checking for external leakage, verifying secure mounting, and ensuring clear access to adjustment mechanisms. Quarterly maintenance involves testing valve operation by gradually increasing system pressure to verify proper opening and closing points. Annual maintenance requires complete valve inspection, including disassembly if possible, cleaning of internal components, and replacement of worn seals.
Maintain detailed documentations of pressure settings, maintenance activities, and any performance issues. These records help identify trends and predict maintenance needs while also giving valuable troubleshooting information.
Adjusting an Adjustable Hydraulic Pressure Relief Valve Safely
Safety must be the primary concern when adjusting relief valve settings. Always depressurize the system completely before beginning adjustment procedures. Use calibrated pressure gauges to ensure accurate setting and make adjustments gradually in small increments.
Start with the valve set slightly below the desired pressure and gradually increase the setting while monitoring system response. Test the adjusted setting under actual operating conditions to verify proper performance. Document the final setting and date of adjustment for maintenance records.
Never exceed the valve’s maximum rated pressure during adjustment, and always follow manufacturer specifications for adjustment procedures and torque requirements.
The Importance of Reliable Pressure Protection
Hydraulic relief valves represent one of the most important components in any hydraulic system as the last line of defense against potentially disastrous overpressure conditions. Their role is beyond simple pressure limitation to surround system protection, performance optimization, and operational safety.
The proper selection, installation, and maintenance of hydraulic relief valves—whether direct-acting, pilot-operated, adjustable hydraulic pressure relief valves, or inline hydraulic pressure relief valve configurations—directly impacts system reliability, component longevity, and operational efficiency. As hydraulic systems become more and more advanced and operate under more demanding conditions, the importance of reliable pressure protection continues to grow.
Investing in quality relief valves and properly maintaining them ensures optimal system performance while protecting valuable equipment and preventing costly failures. Whether you’re specifying components for a new system or upgrading existing equipment, prioritizing proper pressure protection through well-selected and maintained hydraulic relief valves is essential for safe, efficient, and reliable hydraulic system operation.