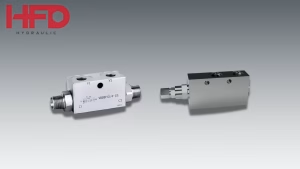
A hydraulic safety valve is a critical protective device designed to automatically limit pressure within hydraulic systems by releasing excess fluid when predetermined pressure thresholds are exceeded. These valves are your first line of defense when things go wrong – they help prevent major system breakdowns, protect your equipment from damage, and keep everyone safe.
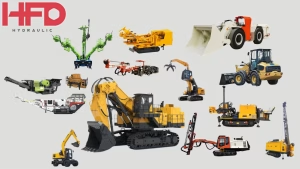
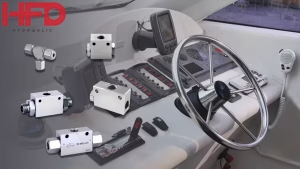
In modern industrial applications, hydraulic safety valves are indispensable components that ensure reliable operation across diverse sectors. You’ll find these valves everywhere – in manufacturing plants they’re built into injection molding machines and hydraulic presses, and construction companies use them in their excavators, cranes, and other heavy lifting equipment. The aerospace sector utilizes these valves in aircrqaft landing gear systems, and marine applications depend on them for steering mechanisms and cargo handling equipment. Oil and gas companies use these valves in their drilling rigs and pipeline networks too, where keeping pressure under control is absolutely critical for everyone’s safety.
Quick Overview: Hydraulic Safety Valve Types, Functions, and Selection
What is a hydraulic safety valve and what types are available?
A hydraulic safety valve is a spring-loaded pressure control device that automatically opens to release excess fluid when system pressure exceeds a preset threshold — protecting pumps, cylinders, hoses, and seals from overpressure damage. It closes automatically once pressure returns to safe levels. The three main types are direct-acting, pilot-operated, and spring-loaded, each suited to different flow rates, pressure ranges, and response time requirements.
Main types and when to use each:
- Direct-acting (VMD20, VAA-RU-DL) – system pressure acts directly on a spring-loaded poppet; fastest response, simplest design, suited for mobile equipment and smaller systems where immediate pressure relief is critical
- Pilot-operated – small pilot valve triggers the main valve using system pressure; handles higher flow rates with greater precision; preferred for large industrial systems, steel mills, and high-capacity hydraulic power units
- Spring-loaded – most common configuration; adjustable spring tension sets the relief pressure; versatile across pressure ranges and flow requirements in hydraulic power units and machine tools
- Anti-shock with anti-cavitation (VAA-RU-DL) – direct-acting design with built-in anti-cavitation port; correct choice for mobile equipment experiencing frequent sudden pressure spikes from impacts or load changes
Example
An excavator bucket striking solid rock causes an instant pressure spike from 3,000 PSI toward 5,000 PSI. A VAA-RU-DL direct-acting anti-shock safety valve opens in milliseconds — diverting excess fluid to tank and absorbing the pressure spike before it can rupture hoses or damage cylinder seals — then closes automatically as pressure normalizes.
Summary
Set hydraulic safety valves 10–25% above normal operating pressure, select direct-acting types for fast response in mobile equipment, pilot-operated for high-flow industrial systems, and always inspect quarterly to verify the valve opens at its set pressure — a safety valve that fails to open is more dangerous than no protection at all.
What Does a Hydraulic Safety Valve Do?
The primary function of a hydraulic safety valve centers on protecting hydraulic components from excessive pressure that could lead to system failure or equipment damage. When system pressure rises beyond safe operating limits, the valve automatically opens to release pressurized fluid back to the reservoir or a low-pressure return line.
This automatic pressure relief mechanism operates through a spring-loaded mechanism that responds instantly to pressure spikes. As pressure builds within the system, it exerts force against the valve’s closing element. Once the pressure exceeds the valve’s preset threshold, it overcomes the spring force, causing the valve to open and discharge fluid until pressure returns to safe levels. The valve then automatically closes, allowing normal system operation to resume.
A hydraulic safety relief valve differs slightly in terminology but serves the same essential function. While “safety valve” typically refers to compressible fluid applications, “relief valve” is often used for incompressible liquids like hydraulic fluid. However, in hydraulic systems, these terms are frequently used interchangeably, as both describe valves that prevent overpressure conditions through automatic fluid discharge.
What Is the Purpose of a Safety Valve in Hydraulics?
Hydraulic safety valves do a lot more than just release pressure when things get too intense. Unlike flow control valves that regulate fluid volume or directional valves that control fluid path, safety valves specifically focus on pressure limitation and system protection.
What they’re really there for is to keep your expensive hydraulic components from getting wrecked when the pressure gets out of hand. Pumps, cylinders, motors, and other system elements have maximum pressure ratings that, when exceeded, can result in seal failure, component cracking, or complete mechanical breakdown. Safety valves prevent these costly failures by maintaining pressure within design parameters.
Hydraulic safety valves are also really important for making sure your system runs efficiently. By stopping those sudden pressure surges that can make your equipment act up or damage parts, safety valves ensure your system runs consistently without problems. This steady operation means you’ll get better productivity, less time with your system down, and you won’t have to spend as much on maintenance over the years.
Operator safety constitutes perhaps the most important purpose of hydraulic safety valves. Without functional pressure protection, hydraulic systems pose significant risks including fluid injection injuries from high-pressure leaks, equipment ejection due to sudden pressure release, and potential fires from hot, pressurized fluid contacting ignition sources. A properly functioning safety valve significantly reduces these hazards by preventing dangerous overpressure conditions.
Hydraulic Safety Valve Types
Direct-Acting Safety Valves
Direct-acting safety valves feature the simplest design among hydraulic safety valve types. In these valves, system pressure acts directly against a spring-loaded poppet or ball. When pressure exceeds the spring’s preset force, the valve opens immediately to relieve excess pressure.

| ANTI-SHOCK TYPE DIRECT-ACTING, WITH ANTI CAVITATION PRESSURE RELIEF VALVE – VAA-RU-DL | CETOP STANDARD WITH DIRECT ACTING PRESSURE RELIEF VALVE – PBL | DIRECT ACTING PRESSURE RELIEF VALVE – VMD20 |
The biggest advantage of direct-acting valves is that they react quickly and you can count on them to work when you need them. They don’t need any outside signals or complicated parts to work, which makes them perfect when you need pressure relief right away. These valves work exceptionally well in smaller hydraulic systems where precise pressure control isn’t critical, such as mobile equipment, small industrial machines, and basic hydraulic circuits.
Pilot-Operated Safety Valves
Pilot-operated safety valves provide superior accuracy and control for complex hydraulic systems. These valves use a small pilot valve to control how the main valve works. The pilot valve responds to system pressure and, when the set pressure is reached, triggers the main valve to open.

| SINGLE PILOT OPERATED CHECK VALVE FLANGEABLE – VBPSF | SINGLE ACTING, SHUT-OFF PILOT OPERATED CHECK VALVE – VBPSL/R | SINGLE ACTING PILOT OPERATED CHECK VALVE – VBPSL/T |
This design offers several advantages over direct-acting types. Pilot-operated valves can handle higher flow rates while maintaining precise pressure settings, making them suitable for large-scale industrial applications. They also seal better and don’t create as much pressure drop when they’re closed. Manufacturing plants with high-capacity hydraulic systems, steel mills, and large construction equipment commonly employ pilot-operated safety valves.
Spring-Loaded Safety Valves
Spring-loaded safety valves are the type you’ll see most often in hydraulic systems. These valves use carefully calibrated springs to set when they’ll open – the stronger the spring, the higher the pressure needed to trigger the valve. The spring’s compression can often be adjusted to modify the relief pressure setting.
Spring-loaded valves are really versatile and can be set up for different pressure ranges and flow needs. They work consistently even when temperatures change and are pretty straightforward to maintain and service. You’ll commonly find them in hydraulic power units, machine tools, and regular industrial hydraulic systems where you need dependable pressure protection.
Understanding the Hydraulic Safety Valve Symbol
The standard hydraulic safety valve symbol in schematic diagrams consists of a square or rectangular body with an arrow indicating flow direction and a spring symbol showing the valve’s spring-loaded nature. The symbol typically includes a diagonal line with an arrow pointing toward the tank or return line, representing the pressure relief path.
In hydraulic circuit diagrams, the safety valve symbol is usually positioned between the pressure line and the return or tank line. The spring symbol shows that the valve stays closed under normal conditions and only opens when the system pressure gets strong enough to push against the spring. Some symbols may include additional markings showing adjustability, such as an arrow through the spring symbol, indicating that the relief pressure can be modified.

Variations in the hydraulic safety valve symbol depend on the specific type and function. Pilot-operated valves may show a smaller pilot valve symbol connected to the main valve symbol. Relief valves designed for specific applications might include additional notation indicating their purpose, such as thermal relief or sequence valve functions. Technicians and engineers need to understand these symbols since they tell you important stuff about how your system is protected and how it operates.
Main Factors to Consider When Selecting a Hydraulic Safety Valve
Pressure Settings and System Requirements
Proper pressure setting represents the most critical factor in hydraulic safety valve selection. You need to set the valve’s relief pressure higher than what your system normally runs at, but lower than the maximum pressure your weakest component can handle. Typically, safety valves are set 10-25% above normal operating pressure, providing adequate protection while avoiding nuisance openings during normal operation.
The pressure characteristics of your system also affect which valve you should choose. Applications with frequent pressure spikes require valves with fast response times, while systems with gradual pressure increases may accommodate valves with slower response characteristics. Think about whether your system runs at steady pressure or if the pressure jumps around when you’re picking out valve specs.
Flow Capacity and Response Speed
Flow capacity determines the valve’s ability to relieve pressure effectively when opened. The valve must have sufficient capacity to handle the maximum flow rate that could cause overpressure conditions. This typically involves calculating the pump flow rate and any potential flow from other system components during pressure relief situations.
Response speed affects how quickly the valve reacts to pressure increases. Direct-acting valves generally provide faster response than pilot-operated types, but pilot-operated valves may offer better accuracy. Applications requiring immediate pressure relief, such as mobile equipment or systems with rapid pressure changes, benefit from fast-responding valve designs.
Material and Durability Considerations
The operating environment significantly impacts material selection for hydraulic safety valves. Corrosive environments require stainless steel or specially coated materials, while high-temperature applications need materials that maintain spring properties and sealing effectiveness at elevated temperatures.
Fluid compatibility is equally important. Different hydraulic fluids may require specific seal materials and valve body materials to prevent degradation or failure. Consider factors such as fluid temperature range, chemical composition, and potential contamination when selecting valve materials.
Maintenance and Inspection Requirements
Make sure you can easily get to your valve for maintenance and inspections when you’re choosing and installing it. Valves requiring frequent adjustment or servicing should be positioned where technicians can safely reach them. Consider whether the valve design allows for in-line maintenance or requires system shutdown and component removal.
Documentation and traceability requirements may dictate valve selection in certain industries. Applications requiring certified pressure relief capabilities may need valves with calibration certificates and regular testing documentation to maintain compliance with safety standards.
Best Practices for Maintenance and Safety
Routine Inspection Schedules
Establishing regular inspection schedules prevents pressure-related failures and ensures continued system protection. Monthly visual inspections should check for external leakage, corrosion, or physical damage to the valve body and connections. These inspections help identify potential problems before they compromise system safety.
Quarterly functional testing verifies that safety valves operate at their intended relief pressure. This testing usually means slowly raising the system pressure while you watch to see at what point the valve opens. Any deviation from the set pressure indicates the need for adjustment or valve replacement.
Annual comprehensive inspections should include disassembly and examination of internal components. Springs, seals, and valve seats require inspection for wear, corrosion, or damage that could affect valve performance. Replace worn components according to manufacturer specifications to maintain reliable operation.
Common Signs Requiring Service
There are several warning signs that tell you your hydraulic safety valve needs to be looked at right away. Continuous or intermittent fluid leakage from the valve discharge port indicates seal failure or contamination preventing proper valve closure. This problem doesn’t just waste your hydraulic fluid – it can also mess with how well your system is protected from pressure spikes.
Chattering or rapid opening and closing during pressure relief events suggests improper pressure setting, worn valve components, or contamination in the valve mechanism. This condition can cause additional wear and may indicate the valve isn’t providing adequate pressure protection.
When your pressure gauge shows readings that are consistently above the valve’s set opening pressure, it’s a clear sign the valve has failed. This is a dangerous situation that needs immediate attention – you need to service or replace that valve right away to prevent equipment damage or safety issues.
Valve Life Extension and Safety Tips
Proper system filtration significantly extends hydraulic safety valve life by preventing contamination-related wear and malfunction. Install appropriate filtration upstream of safety valves and maintain filter elements according to manufacturer recommendations.
Avoid using safety valves as primary pressure control devices. Frequent operation reduces valve life and may compromise protection capability. Instead, use pressure-reducing valves or load-sensing systems for normal pressure control, reserving safety valves for emergency protection only.
Make sure your team knows how safety valves work and understands the dangers of working with pressurized hydraulic systems. Ensure technicians understand proper lockout/tagout (LOTO) procedures when servicing safety valves and emphasize the importance of maintaining these critical safety devices in proper working condition.
Hydraulic safety valves are like the guardians of your hydraulic system – they protect your valuable equipment and keep operators safe by controlling pressure reliably. You really can’t overstate how important they are in today’s industrial settings – they prevent major breakdowns and keep your systems running efficiently.
The selection of appropriate safety valve types—whether direct-acting, pilot-operated, or spring-loaded—depends on specific system requirements, operating conditions, and performance expectations. Understanding these differences enables informed decisions that optimize both protection and system performance.
Keep up with regular maintenance, install them properly, and follow what the manufacturer says – that’s how you make sure these important safety devices keep protecting your system for years to come. Set up regular inspection schedules and learn to spot signs that your valve is wearing out – this prevents surprise failures that could put your system at risk.
If you’re dealing with specialized equipment or complex hydraulic systems, it’s worth talking to valve manufacturers or hydraulic experts – they can help you pick the right safety valve and keep it running properly. Their expertise ensures proper valve specification, installation, and ongoing maintenance practices that maximize both safety and system reliability.