Many hydraulic engineers and procurement specialists use “unloader valve” and “relief valve” interchangeably. In practice, these are two different pressure control devices with different purposes, different pilot configurations, and very different consequences for system efficiency if one is substituted for the other. This article explains both valves, how they differ, and when each one belongs in your hydraulic circuit.
Quick Overview
- Hydraulic unloader valve — diverts pump flow to tank at near-zero pressure during idle/standby using a remote pilot
- Pressure relief valve — limits maximum system pressure using an internal pilot; stays closed under normal operation
- Key difference — pilot type: unloader valves sense downstream/accumulator pressure; relief valves sense inlet pressure
- Energy impact — a misapplied relief valve keeps the pump under full pressure during standby, converting wasted energy into heat
- Common applications — unloader valves belong in hi-low circuits and accumulator systems; relief valves belong in every hydraulic circuit as the pressure ceiling
- HFD product — VEP/FL series — CETOP face-mounting hi-low unloading valve, rated up to 350 bar (5,100 psi), available in four sizes
What Is a Hydraulic Unloader Valve?
A hydraulic unloader valve is a pressure control valve that diverts pump flow back to tank at minimal pressure once the system reaches a preset threshold. Its job is not to protect the system from overpressure — it is to allow the pump to run at near-zero load during idle or standby conditions, while downstream pressure is held by a check valve and accumulator, or by circuit geometry.
An unloader valve is a pressure control valve that works on the principle of hydraulic force as opposed to spring force alone. The key feature that distinguishes it from a relief valve is its pilot configuration: an unloader valve uses a remote pilot, whereas a pressure relief valve uses an internal pilot.
In practical terms, this means the unloader valve does not sense its own inlet pressure. It senses pressure from another point in the circuit — typically downstream of a check valve, from an accumulator circuit, or from the high-pressure side of a dual-pump system. When that remote signal reaches the set point, the valve opens and dumps pump flow to tank at very low back pressure.
A hydraulic unloading valve diverts pump flow to tank after the set pressure is reached, letting the pump run with minimal load while system pressure is maintained.
What Is a Hydraulic Relief Valve?
A pressure relief valve’s main job is protection, not control. Its primary function is to limit the maximum pressure in a hydraulic circuit, protecting components from damage if pressure builds beyond a safe threshold.
When pressure in the circuit climbs past the valve’s setting, the relief valve opens and lets fluid bypass to the tank — then shuts again once pressure drops back down. This means a relief valve can bypass fluid anytime — or all the time — without intervention.
Unlike an unloader valve, a relief valve operates on internal pilot pressure. It senses the pressure directly at its inlet and responds when that pressure exceeds the spring setting. It does not distinguish between an idle condition and an actual overpressure event — it simply reacts to the pressure it sees.
Under normal conditions, a relief valve just sits there doing nothing — and that’s exactly the point. It only opens when pressure climbs too high, acting as the circuit’s last line of defense against overpressure damage.
Side-by-Side: Key Technical Differences
| Hydraulic Unloader Valve | Pressure Relief Valve | |
| Primary function | Pump unloading / energy efficiency | System overpressure protection |
| Pilot type | Remote (external) pilot | Internal pilot |
| Normal operating state | Opens during idle/standby | Closed during normal operation |
| Pressure sensing point | Downstream / accumulator side | Inlet port |
| Flow to tank pressure | Near-zero (approx. 20 psi) | At or near full system pressure |
| Typical application | Hi-low circuits, accumulator systems | All hydraulic circuits as safety device |
| Energy impact when bypassing | Minimal — pump runs at low load | High — pump works against full pressure |
The Pilot Difference: Why It Changes Everything
The distinction in pilot type is not a minor technical detail — it is what determines whether the pump is unloaded efficiently or kept under pressure unnecessarily.
When pressure in the working circuit climbs past the valve’s set point, that signal travels through the remote-pilot port and triggers the unloading spool to act. Pressure drop on the front side of the unloading spool lowers back force, and pilot pressure from the high-pressure circuit forces the main poppet open at approximately 20 psi, allowing all high-volume pump flow to go to tank at little or no pressure drop.
This is fundamentally different from how a relief valve responds. A relief valve must hold the full pressure differential across its seat to stay open. An unloading valve requires only a very small control pressure to push the spool and open the valve port, whereas a relief valve needs a higher control pressure for the same action. The result is that when a pump is unloaded through a properly configured unloader valve, the power consumed by the pump drops dramatically — as opposed to a relief valve scenario where the pump continues working against high pressure.
What Happens When You Use a Relief Valve Instead of an Unloader Valve?
This is the most common and costly mistake in hydraulic system design. Swapping in a relief valve where an unloading valve should be is one of the most common and costly mistakes in hydraulic system design. The pump stays loaded against full system pressure the entire time, and that energy has to go somewhere: straight into heat.
When a fixed-displacement pump operates against high pressure through a relief valve during standby, all of that energy converts to heat. Many fixed-volume pump circuits depend on this bypassing capability during the cycle, and some even bypass fluid during idle time — and a system designed this way can run hot even with a heat exchanger installed.
By using an unloading valve, pump load is reduced during idle conditions, achieving heat reduction and energy savings because the prime mover load is lowered. In standby mode, the hydraulic unloading valve can reduce the energy consumption of the hydraulic pump by about 80%, while also reducing the heat generated by the system due to high pressure.
In short: a relief valve used as a standby bypass device is technically functional but operationally wasteful. The system stays safe but runs inefficiently, wears faster, and costs more to operate.
Where Each Valve Belongs in a Circuit
The relief valve belongs in every hydraulic circuit as the system’s pressure ceiling. It is the last line of defense against component failure from overpressure — for example, when an actuator reaches end of stroke, when a load spikes unexpectedly, or when a directional control valve is centered. Relief valves are used in circuits to protect components from excess pressure due to heat or external forces where pressure buildup in a blocked flow circuit could damage an actuator or be a safety hazard.
The hydraulic unloader valve belongs in circuits where the pump must continue running during periods when no work is being done, and where that standby period should not be penalized energetically. The two most common configurations are:
1. Hi-Low (Two-Pump) Circuits
In high-low pump circuits, the unloading valve acts to unload the large-volume pump during load operation of the small-volume pump — in the same manner as accumulator unloading, but triggered by the pressure generated by the high-pressure pump rather than by accumulator charge. This allows a machine to rapid-traverse with high flow at low pressure, then transition to high-pressure, low-flow work without reconfiguring the pump arrangement.
2. Accumulator Circuits
In accumulator circuits, when the system pressure reaches the maximum cut-out pressure, the unloading valve diverts pump delivery to the reservoir at low pressure, automatically unloading the pump. When accumulator pressure drops to the cut-in pressure, the valve directs pump delivery back to the accumulator and hydraulic system.
Both circuits rely on the unloader valve’s remote pilot signal — the accumulator or high-pressure circuit pressure — to trigger opening, not the pump outlet pressure itself. A relief valve cannot replicate this behavior because it has no remote sensing capability in its standard configuration.
Can One Valve Do Both Jobs?
In some applications, yes. Some unloading-relief valves combine both functions: in standby mode they open fully to unload the pump, and in active mode they operate like a relief valve to regulate pressure. Such composite valves are useful in systems with frequent stop-start cycles, such as injection molding machines. These combination valves simplify circuit design where both functions are required in the same pressure circuit but add cost and require careful specification to ensure both pressure settings are correctly sequenced.
For most standard industrial and mobile hydraulic circuits, however, the two valves serve distinct roles and are specified separately.

HFD Hydraulic Unloader Valve Options
HFD Hydraulic manufactures unloading valves for both hi-low circuit configurations and accumulator circuit applications.
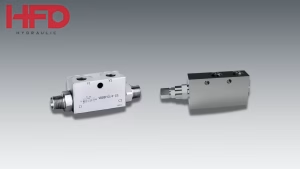
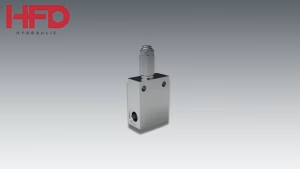
The VEP/FL series is HFD’s CETOP face-mounting hi-low unloading valve, designed to manage high and low-pressure operations in a single hydraulic circuit, directing flow between high- and low-pressure lines to optimize energy usage during pressure transitions. Available in four sizes (VEP/FL 6-38, 10-12, 16-34, and 16-100), the valve’s pressure rating depends on body construction: aluminum bodies are rated to 210 bar (3,050 psi), while steel bodies handle up to 350 bar (5,100 psi). Nominal flow scales by model, with the largest variant (VEP/FL 16-100) handling up to 100 l/min (26.4 US gpm) through its work port. The valve operates across a temperature range of -40°C to 100°C (-40°F to 212°F), is compatible with mineral-based hydraulic oil at viscosities from 10 to 200 cSt, and supports a maximum contamination level of ISO 4406 18/16/13.
This makes the VEP/FL suited to two-pump systems where the large-volume pump must be unloaded automatically once the small-volume, high-pressure pump takes over — the same hi-low principle described in HFD’s two-pump high-low unloading valve systems guide.
For accumulator-based unloading, HFD’s accumulator unloading valve handles the automatic charge-and-hold cycle discussed in the accumulator unloading valve in excavators guide.
Both valve families operate on the remote-pilot principle described above — they respond to downstream circuit pressure, not inlet pressure, which is what allows the pump to be fully unloaded rather than held against system pressure during standby.
Full dimensional drawings, port size charts, and pressure-drop performance curves for each VEP/FL size are available on the VEP/FL product page. For circuit-specific sizing guidance, contact the HFD Hydraulic team directly.
Choosing the Right Valve
The hydraulic unloader valve and the pressure relief valve are related in structure but serve opposite purposes in a circuit. The relief valve sets the system’s pressure ceiling and protects against damage. The unloader valve manages pump load during standby and protects against wasted energy and heat buildup.
Neither can substitute for the other without consequence. A system running a relief valve where an unloader valve belongs will operate safely — but inefficiently, and at higher operating cost over time. A system without a relief valve but with an unloader valve has no overpressure protection, which is a safety risk.
Specifying both correctly, and understanding which circuit condition each one is designed to handle, is a basic requirement of sound hydraulic system design.