A hydraulic valve for log splitter serves as the control center for your wood splitting operation, directing the flow of hydraulic fluid to create the immense force needed to split logs efficiently. This key part controls how well your log splitter works, so it’s important to know how it functions, how to maintain it, and when to replace it.
The hydraulic log splitter valve works in conjunction with your machine’s pump, cylinder, and hydraulic fluid to create a system capable of generating thousands of pounds of splitting force. Whether you’re dealing with hardwood or softwood, the proper functioning of your hydraulic valve ensures consistent performance and safe operation.
Quick Overview: Hydraulic Valve for Log Splitter
What does a hydraulic valve do on a log splitter?
A hydraulic valve for a log splitter controls the direction, flow, and pressure of hydraulic fluid to the splitting cylinder — directing it to extend the ram for splitting, retract it for the next log, and hold it in neutral between operations. It works with the pump, cylinder, and hydraulic fluid to generate thousands of pounds of splitting force, and includes built-in pressure relief protection that automatically backs off if the ram hits an immovable object.
Main types of hydraulic valves for log splitters:
- Manual control valve – lever or handle operated; direct tactile control over ram speed and position; most reliable and affordable due to simple mechanical design
- Electric control valve – solenoid-actuated by switch or button; easier operation for users with limited hand strength; supports additional safety features and automated functions
- Proportional control valve – variable flow control allowing ram speed adjustment per log; highest precision but greater complexity and cost
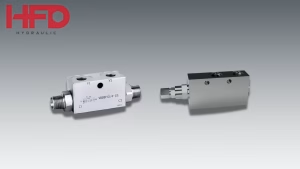
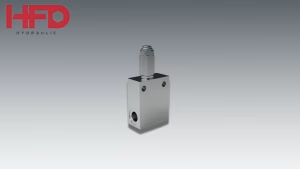
- Pressure relief valve (VMD20, VMP) – safety device that diverts flow at a set pressure limit, protecting the cylinder and pump if the ram stalls against a hard knot or dense hardwood
Example
A firewood producer splitting dense oak with a 4-inch bore cylinder at 3,000 PSI generates approximately 37,700 pounds of splitting force. When the ram hits a particularly hard knot and pressure spikes beyond the relief valve setting, the VMD20 pressure relief valve opens automatically — diverting fluid to tank and protecting the pump and cylinder from overload damage.
Summary
Choose a manual valve for simplicity and reliability in standard log splitting, an electric valve for ease of operation or automation, and always verify that your pressure relief valve is correctly set to approximately 10% above normal operating pressure to protect the system during overload conditions.
How Does a Log Splitter Hydraulic Valve Work?
How a hydraulic valve for log splitter works is actually pretty clever—it uses pressurized fluid and precise mechanical parts working together. When you engage the control lever or switch, the valve redirects pressurized hydraulic fluid from the pump to the cylinder, causing the piston to extend and apply splitting force to the log.
During the splitting cycle, the hydraulic log splitter valve maintains precise control over fluid flow direction. In the forward position, fluid flows to the cap end of the cylinder, extending the ram. When you move the control to the reverse position, the valve redirects fluid to the rod end of the cylinder, retracting the ram back to its starting position.
The valve comes with safety features like pressure relief valves that stop your log splitter from working too hard and breaking. These safety features make sure that if you hit a really tough log, the system will back off automatically instead of breaking something inside. Most modern hydraulic valves for log splitters feature a neutral position that stops all fluid flow, allowing the ram to hold its position under load. This comes in really handy when you’re lining up logs or need to make quick adjustments while splitting.
What is the Hydraulic Pressure for a Log Splitter?
The hydraulic pressure for a log splitter typically ranges from 2,500 to 3,500 PSI (pounds per square inch), with most residential and commercial units operating at around 3,000 PSI. This pressure level provides the optimal balance between splitting force and system reliability.
Professional-grade log splitters may operate at higher pressures, sometimes reaching 4,000 PSI or more, depending on the application and log size requirements. The hydraulic valve for log splitter must be rated to handle these pressure levels safely while maintaining precise control over fluid flow.
The relationship between pressure and splitting force is determined by the cylinder bore size. A 4-inch bore cylinder operating at 3,000 PSI generates approximately 37,700 pounds of splitting force, while a 5-inch bore cylinder at the same pressure produces around 58,900 pounds of force.
It’s crucial that your hydraulic log splitter valve is properly matched to your system’s pressure rating. Using an under-rated valve can result in premature failure, safety hazards, and poor performance.
Types of Hydraulic Valves for Log Splitters
Manual Control Valves
Manual hydraulic valves for log splitters require physical operation through a lever or handle. These valves offer direct control over the splitting process and are typically more affordable and reliable due to their simple mechanical design. The operator has complete control over ram speed and can make precise adjustments during the splitting process.
Electric Control Valves
Electric hydraulic log splitter valves use solenoids to control fluid flow, activated by switches or buttons. These systems provide easier operation, especially for users who may have difficulty operating manual controls. Electric valves can also incorporate additional safety features and automated functions.
Proportional Control Valves
Advanced proportional valves allow for variable flow control, enabling operators to adjust ram speed based on the specific requirements of each log. This type of hydraulic valve for log splitter provides the most precise control but comes at a higher cost and complexity.

| DIRECT ACTING PRESSURE RELIEF VALVE – VMD20 | CROSS LINE RELIEF VALVE – VAU | CETOP STANDARD WITH DIRECT ACTING PRESSURE RELIEF VALVE – PBL |
Key Components of a Hydraulic Log Splitter Valve
Spool Assembly
The spool is the internal component that physically redirects hydraulic fluid flow within the valve body. High-quality spools are precision-machined and feature tight tolerances to minimize internal leakage and ensure responsive operation.
Valve Body
The valve body houses all internal components and provides the mounting points for hydraulic connections. Bodies are typically constructed from cast iron or steel and must withstand system operating pressures while resisting corrosion.
Spring Assembly
Springs return the valve spool to its neutral position when control force is removed. Proper spring tension ensures reliable operation and consistent feel during valve operation.
Seals and O-Rings
Quality seals prevent hydraulic fluid leakage and maintain system pressure. Regular inspection and replacement of these components is essential for optimal performance of your hydraulic valve for log splitter.

Installation and Setup Guidelines
Mounting Considerations
Proper mounting of your hydraulic log splitter valve ensures optimal performance and longevity. The valve should be securely fastened to prevent vibration and positioned for easy access to controls and service points. Consider orientation requirements specified by the manufacturer, as some valves are designed for specific mounting positions.
Hydraulic Line Connections
Use appropriate fittings and hydraulic hose rated for your system pressure when connecting the valve to your pump and cylinder. Ensure all connections are properly tightened and use thread sealant where specified to prevent leaks.
Control Linkage Setup
For manual valves, proper adjustment of control linkages ensures smooth operation and prevents binding. The control should move freely through its full range without excessive force or slack.
Maintenance and Troubleshooting
Regular Maintenance Tasks
Maintaining your hydraulic valve for log splitter involves regular inspection of seals, checking for external leakage, and ensuring smooth control operation. Clean external surfaces regularly to prevent contamination from entering the system during service.
Common Problems and Solutions
Slow or erratic ram movement often indicates internal valve wear or contaminated hydraulic fluid. External leakage typically points to failed seals or loose connections. If your hydraulic log splitter valve becomes difficult to operate, check for binding in the control linkage or internal contamination.
Fluid Contamination Issues
Contaminated hydraulic fluid is the leading cause of valve failure. Regular fluid changes and proper filtration help prevent premature wear and maintain smooth operation. Always use manufacturer-recommended hydraulic fluid specifications.
Performance Optimization
Flow Rate Considerations
The flow rate through your hydraulic valve for log splitter directly affects cycle time and overall productivity. Higher flow rates reduce cycle time but may require larger, more expensive system components. Balance flow rate with your specific application requirements and budget constraints.
Pressure Settings
Proper pressure relief valve settings protect your hydraulic log splitter valve and other system components from damage due to overload conditions. Set relief pressure approximately 10% above normal operating pressure for optimal protection.
Temperature Management
Hydraulic fluid temperature affects system performance and component life. Ensure adequate cooling capacity and consider adding a hydraulic cooler if your system operates in high-temperature environments or under heavy continuous use.
Safety Considerations
Pressure Relief Systems
Every hydraulic valve for log splitter should incorporate adequate pressure relief protection. This safety feature prevents catastrophic failure and protects operators from injury due to system over-pressurization.
Operational Safety
Always follow manufacturer safety guidelines when operating equipment with hydraulic log splitter valves. Maintain proper body position, use appropriate personal protective equipment, and never attempt to service pressurized systems.
Emergency Procedures
Understand emergency shutdown procedures and ensure all operators know how to quickly stop the splitting process if necessary. Regular safety training helps prevent accidents and equipment damage.

| LIGHT RELIEF VALVE – VMP | PILOT OPERATED PRESSURE RELIEF VALVE – VMPP/B/L | TYPE-G CROSS LINE RELIEF VALVE – VAU-G |
Selecting the Right Hydraulic Valve
Capacity Requirements
Choose a hydraulic valve for log splitter based on your specific capacity requirements, including log size, wood species, and production volume. Consider future needs when making your selection to avoid premature system upgrades.
Budget Considerations
Balance initial cost with long-term reliability and maintenance requirements. While premium valves cost more initially, they often provide better performance and longer service life, reducing overall operating costs.
Compatibility Factors
Ensure your selected hydraulic log splitter valve is compatible with your existing pump, cylinder, and control systems. Consider mounting requirements, port sizes, and control interface compatibility.
Understanding the operation and maintenance requirements of your hydraulic valve for log splitter ensures reliable performance and safe operation. Regular maintenance, proper installation, and appropriate component selection contribute to years of trouble-free wood splitting capability. Whether you’re maintaining an existing system or planning a new installation, prioritizing quality components and proper setup procedures will maximize your investment in log splitting equipment.
Need a quotation? Contact us for a free quote!