Industrial conveyor systems are among the most continuous-duty applications in hydraulic engineering. Whether moving bulk materials across a processing facility, feeding components through an assembly line, or transferring goods between workstations in a distribution center, hydraulic conveyors run constantly — and inconsistent speed control is one of the fastest ways to compromise both throughput and safety.
In-line flow control valves sit at the center of that challenge. Installed directly in the hydraulic line, they govern how quickly fluid reaches the motor or cylinder driving the conveyor, translating directly into belt or chain speed. Getting that speed consistent and controllable — across varying loads, temperatures, and operating cycles — is the job these valves do every shift, every day.
Quick Overview: In-Line Flow Control Valves for Conveyor Systems
What is an in-line flow control valve for conveyor systems?
An in-line flow control valve for conveyor systems is a valve installed directly in the hydraulic line to govern how quickly fluid reaches the motor or cylinder driving the conveyor belt or chain — translating directly into consistent belt speed. In conveyor applications, poppet-type flow restrictors with integrated check valves are preferred because they provide near-zero leakage when closed, stable flow control under back-pressure variation, and free unrestricted flow in the return direction.
Key functions and specifications (HFD VSRU/C):
- Restricted direction (A to B) – poppet restricts flow to a set rate, governing conveyor motor speed precisely and consistently across load changes
- Free flow direction (B to A) – integrated check valve allows unrestricted return flow, preserving cycle efficiency and enabling reverse jog without removing the valve
- Port sizes – G1/4 through G1½, covering 30–210 L/min (7.9–55.5 US gpm) for most industrial conveyor motor sizing
- Pressure rating – 350 bar at smaller port sizes, 230 bar at G1½
- Temperature range – −40°C to +100°C; handles cold-start conditions in unheated facilities and elevated temperatures in high-cycle applications without performance drift
Example
On an accumulation conveyor in a distribution center, a VSRU/C is installed at each zone’s actuator feed line. The poppet restricts flow to control how quickly each zone engages — preventing the pressure spike that causes product jolts or belt judder at zone transitions — while the check valve allows clean, unrestricted retraction when the zone releases.
Summary
An in-line flow control valve with an integrated check valve is the correct choice for hydraulic conveyor circuits where consistent motor speed, directional flow restriction, and minimal leakage during hold or stop conditions are all required in a single compact component.
What Makes Conveyor Applications Demanding for Flow Control
A conveyor system sounds straightforward: move material from point A to point B. In practice, the hydraulic demands are more varied. A belt conveyor carrying loose bulk material must maintain steady speed even as the load changes — a sudden surge of material on an incline section creates a heavier drive demand, and if the hydraulic motor speeds up or lurches in response, product spills or belt tracking issues follow.
Accumulation conveyors add another layer of complexity. In these systems, zones of the conveyor stop independently to hold product while upstream zones continue moving. The hydraulic actuators controlling each accumulation zone need reliable one-direction restriction with free return flow — exactly the operating principle of a flow restrictor with an integrated check valve.
Temperature also matters more in conveyor applications than is often acknowledged. Facilities running 24/7 will see significant hydraulic fluid temperature swings between startup and steady-state operation, and between seasons. A valve that performs well at 60°C but drifts at 20°C will produce inconsistent conveyor speeds that are difficult to diagnose.
The Role of the Poppet Mechanism
Most flow restrictors use a needle-and-seat design where a tapered needle closes against a seat to vary the orifice opening. Poppet-type restrictors work differently. The poppet — a ball or conical element — seats directly against a machined bore, creating a seal that is essentially zero-leakage when closed and highly repeatable in its controlled-open position.
For conveyor systems, this matters in two ways. First, the minimal internal leakage means that when a conveyor zone is commanded to hold position or stop, it actually stops rather than slowly drifting under residual flow. Second, the poppet’s behavior under varying back pressure is more stable than a needle design, which can deflect slightly under high back-pressure conditions and alter the effective orifice size.
Featuring the VSRU/C: Poppet Type Flow Restrictor with Check Valve
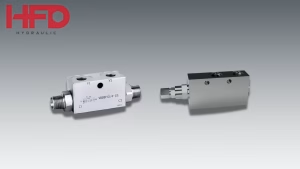
HFD Hydraulic’s VSRU/C brings together poppet-type restriction and an integrated check valve in a single in-line body — a combination well-suited to the directional demands of conveyor hydraulics.

The check valve allows free flow in the reverse direction (B to A), which means the return stroke or back-drive of a hydraulic actuator is unrestricted, preserving cycle efficiency. In the controlled direction (A to B), the poppet restricts flow to the set rate, governing actuator speed precisely. This is the operating pattern needed in conveyor drive circuits where motor speed needs to be controlled in one direction while return or freewheeling flow should not be impeded.
The VSRU/C is available in seven port sizes from G1/4 through G1½, covering nominal flows from 30 l/min up to 210 l/min (7.9 to 55.5 US gpm) in the restricted direction — a range that covers most industrial conveyor motor sizing. Pressure ratings reach 350 bar (5,100 psi) at the smaller port sizes, stepping down to 230 bar (3,300 psi) at the larger ends, comfortably within the operating envelope of most industrial conveyor hydraulic circuits.
The temperature range of -40°C to 100°C (-40°F to 212°F) means the VSRU/C handles both cold-start conditions in unheated facilities and elevated operating temperatures in high-cycle applications without performance drift. Fluid viscosity compatibility ranges from 10 to 200 cSt, covering standard mineral-based hydraulic oils across seasonal temperature variation.
Installation is straightforward. The threaded body drops directly into the hydraulic line without additional mounting hardware, which is particularly useful when adding flow control to an existing conveyor circuit during a retrofit or maintenance window.
Where to Apply In-Line Flow Control on a Conveyor Circuit
For a hydraulic belt or chain conveyor, the most common placement is in the motor inlet line to control drive speed. The VSRU/C’s check valve allows free flow when the drive direction is reversed for tensioning or belt tracking adjustments — useful in facilities that need occasional reverse jog capability without removing the flow control from circuit.
On accumulation conveyors, the VSRU/C is appropriate at each zone’s actuator feed line, where the restriction governs how quickly the zone engages and the check valve allows clean, unrestricted retraction. This prevents the pressure spike on engagement that can jostle product or cause belt judder at zone boundaries.
On incline conveyors, poppet-type valves offer an additional benefit: when the drive circuit loses pressure unexpectedly, the poppet’s near-zero internal leakage resists backward drift under gravity load, buying time for a proper load-holding valve to respond — or reducing the severity of any downslope movement in a fail scenario.
Selecting the Right VSRU/C Size
Port size selection should be based on the maximum flow rate in the restricted direction rather than the line size alone. Undersizing the valve creates excessive pressure drop across the restrictor, generating heat and reducing efficiency. Oversizing produces a valve operating near its fully-open position, where small adjustments have large flow effects and stable control becomes difficult.
HFD Hydraulic’s team can assist with sizing based on your conveyor motor’s flow demand and the system’s operating pressure range. The seven available port sizes provide enough granularity to make a well-matched selection for most conveyor applications.

In-line flow control valves are not a complex component — but the right design choice makes a measurable difference in how a conveyor system behaves over its service life. The poppet mechanism in the VSRU/C addresses the two issues that matter most in high-cycle conveyor applications: leakage and stability. Combined with integrated check valve function, wide port size availability, and a broad temperature and pressure range, it is a practical, reliable choice for engineers specifying hydraulic conveyor circuits. To learn more about the VSRU/C or discuss your conveyor system requirements, contact HFD Hydraulic directly.