Choosing between a pilot operated check valve and a counterbalance valve can make or break your hydraulic system’s performance. While both valves handle load holding and prevent unwanted cylinder movement, they serve fundamentally different purposes. Understanding when to use each type will save you from costly mistakes, equipment damage, and safety hazards.
This comparison breaks down the critical differences between these two load control valves, helping you select the right solution for your application.
Quick Overview: Pilot Operated Check Valve vs Counterbalance Valve
What is the difference between a pilot operated check valve and a counterbalance valve?
A pilot operated check valve is a non-modulating on/off valve designed exclusively for static load holding — it is either fully open or fully closed, with near-zero leakage. A counterbalance valve is a modulating motion control valve that combines load holding with dynamic flow control, allowing smooth, controlled movement of loads under gravity. Both prevent cylinder drift, but only the counterbalance valve can safely control an overrunning load in motion.
Key differences at a glance:
- Pilot operated check valve – on/off only; excellent for static clamping, horizontal positioning, and long-term zero-leak holding; causes dangerous ratcheting if used on vertical descending loads
- Counterbalance valve – modulating; essential for vertical load lowering, over-center loads, crane booms, and any application where gravity creates an overrunning load during descent
- Leakage – pilot check valves offer near-zero leakage (under 1 drop/minute); counterbalance valves have slightly higher leakage but provide controlled motion that pilot checks cannot
- Cost – pilot check valves cost 30–50% less than counterbalance valves; the cost difference is irrelevant if motion control is required
- Setting – counterbalance valves must be set to approximately 1.3x maximum load pressure; pilot checks require no pressure adjustment
Example
A mobile crane boom uses a counterbalance valve — not a pilot check valve — because the boom must lower smoothly under gravity. A pilot operated check valve in this application would cause the boom to ratchet down in jerky, uncontrolled steps as pilot pressure repeatedly builds and collapses, creating dangerous shock loads on cylinders, fittings, and seals.
Summary
Use a pilot operated check valve for static load holding where the load stays stationary until released. Use a counterbalance valve whenever the load moves under gravity — if the load is in motion and gravity is a factor, a counterbalance valve is not an optional upgrade but a required safety component.
Understanding the Core Difference
The fundamental distinction comes down to one critical capability: motion control.
Pilot operated check valves are non-modulating, on/off valves designed exclusively for static load holding. They operate in only two states—fully open or fully closed. These valves excel at position holding and preventing cylinder drift but cannot meter oil flow through them.
Counterbalance valves are modulating motion control valves that combine load holding with dynamic flow control. They have the ability to maintain actuator movement at a desired flow rate as well —this prevents loads from running away due to external forces like gravity. This modulation capability makes them essential for controlling overrunning loads.
Think of it this way: a pilot operated check valve is like a deadbolt lock—it’s either locked or unlocked. A counterbalance valve functions more like a variable-speed brake that can slow movement while still allowing controlled motion.
How Each Valve Works
Pilot Operated Check Valve Function
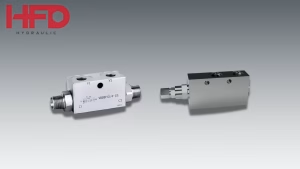
A pilot operated check valve allows free flow in one direction through an internal check valve. The check valve lets fluid flow into the rod-end port to raise the load, while the counterbalance valve prevents the load from dropping when no pressure is applied to the cap end of a cylinder.

| DOUBLE ACTING PILOT CHECK VALVE – VBPDE | Single Pilot Operated Check Valve – VBPSE | DOUBLE PILOT OPERATED HYDRAULIC CHECK VALVE FLANGEABLE – VBPDE-FL |
In order for the trapped fluid to be released, pilot pressure acts on a pilot piston with a larger surface area than the main poppet. This pilot ratio—typically between 3:1 and 8:1—creates mechanical advantage. If your system has 1,000 PSI back-pressure holding the valve closed, only 250 PSI pilot pressure opens it with a 4:1 pilot ratio. The problem occurs when lowering vertical loads. When trying to lower a load being acted on by gravity, the pilot operated check valve may cause severe ratcheting of the actuator and resultant shock in the hydraulic system. This happens because the load tries to drop faster than the pump can supply oil, causing the pilot pressure to drop, which closes the valve abruptly, then reopens when pressure builds—creating jerky, uncontrolled movement.
Counterbalance Valve Operation
A counterbalance valve combines both the features of a reverse free-flow check valve and a pilot-operated relief valve. During load raising, the integrated check valve permits unrestricted oil flow into the cylinder.
The sophisticated control happens during lowering. The external pilot line acts on a surface area typically three times that which the internal pilot pressure acts on, with common ratios of 3:1 or 4:1. Both the pilot pressure and load-induced pressure work together to overcome the spring setting.

| DOUBLE ACTING LOAD SENSITIVE COUNTERBALANCE VALVE – VODL | SINGLE ACTING COUNTERBALANCE VALVE – VOSL/SC | COUNTERBALANCE DOUBLE OVERCENTER VALVE – VBCD-DE |
Here’s the critical difference: counterbalance valves exhibit modulating behavior influenced by both load pressure and pilot pressure, resulting in an inverse pilot ratio where lighter loads demand increased pilot pressure, whereas heavier loads require less pilot pressure.
This inverse relationship creates smooth, controlled lowering. If the load tries to drop too fast, pressure drops in the external pilot line, causing the counterbalance valve’s spool to partially close, preventing uncontrolled drop of the load.
When to Use Pilot Operated Check Valves
Pilot operated check valves work best in specific load-holding scenarios where motion control isn’t required:
Clamping Applications – Holding workpieces firmly in position during machining operations where the clamp remains stationary until released.
Horizontal Cylinder Positioning – Maintaining cylinder position in horizontal applications where gravity isn’t a factor and controlled lowering isn’t needed.
Static Load Holding – Applications requiring zero-leak holding for extended periods, such as holding press rams at top position during die changes.
Hose Failure Protection – Preventing cylinder collapse if hydraulic lines rupture, though the load must already be stationary.
Lower Cost Requirements – Budget-conscious applications where the simpler valve design provides adequate functionality.
The most essential advantage of pilot operated check valves is their almost zero leakage rate —often less than 1 drop per minute at rated pressure. This makes them superior for long-term position holding where even minimal drift is unacceptable.
When Counterbalance Valves Are Essential
Counterbalance valves become necessary whenever loads are in motion, particularly with overrunning load conditions:
Vertical Load Lowering – Crane booms, excavator arms, dump truck beds, and any application where gravity creates an overrunning load during descent.
Over-Center Loads – Mobile equipment where loads transition from resisting to assisting movement, such as boom cylinders that go from fighting gravity to being pulled by it.
Precise Speed Control – Manufacturing processes requiring consistent cylinder speed regardless of load variations, such as press operations or injection molding.
Variable Load Applications – Systems where load weight changes during the cycle, requiring automatic adjustment to maintain smooth motion.
Safety-Critical Motion – Applications where uncontrolled movement poses significant danger, such as aerial work platforms or vehicle lifts.
Whenever uncontrolled movement can occur from an overrunning load, a counterbalance valve should be used, as pilot-operated check valves cannot control an overrunning load.
Application Suitability Matrix
| Application Type | Pilot Check Valve | Counterbalance Valve | Best Choice |
| Horizontal clamping | Excellent | Adequate | Pilot Check |
| Vertical load holding (static) | Excellent | Good | Pilot Check |
| Vertical load lowering | Poor (ratcheting) | Excellent | Counterbalance |
| Over-center loads | Unsuitable | Excellent | Counterbalance |
| Long-term position holding | Excellent (zero leak) | Good | Pilot Check |
| Variable speed control | Unsuitable | Excellent | Counterbalance |
| Hose burst protection | Good (static only) | Excellent | Counterbalance |
| Press hold position | Excellent | Good | Pilot Check |
| Mobile crane boom | Poor | Excellent | Counterbalance |
| Manufacturing press lowering | Poor | Excellent | Counterbalance |
Cost and Complexity Comparison
Initial Investment Pilot operated check valves cost significantly less—typically 30-50% the price of comparable counterbalance valves. This makes them attractive for budget-conscious applications, though using them inappropriately can lead to much higher costs through system damage and downtime.
Counterbalance valves command premium pricing due to their sophisticated modulating design, precision internal components, and adjustable spring mechanisms. However, for load-holding and motion control, a counterbalance valve is worth the extra cost.
Installation Complexity Both valves should be mounted as close as possible to the actuator in order to minimize trapped volume and improve response. Pilot operated check valves have simpler installation with straightforward pilot line connections.
Counterbalance valves require proper setting adjustment. To properly set the counterbalance valve, adjust its spring to its highest setting and raise the load, then very slowly turn the adjustment in the opposite direction. Technical knowledge and careful attention is needed in this tuning process.
Maintenance Requirements Pilot operated check valves need minimal maintenance due to their simpler design with fewer moving parts. Periodic inspection for contamination and seal condition typically suffices.
Counterbalance valves require more attention. Contamination can cause the internal check valve or spool to stick open, and when this occurs, service people often assume drifting is caused by the cylinder’s piston seals leaking. Regular inspection of the modulating spool, spring adjustment, and internal check valve prevents performance degradation.
Common Selection Mistakes
Using Pilot Checks for Vertical Loads The most common error is installing pilot operated check valves on vertical cylinders that need to lower loads under control. This causes the load to ratchet down as cylinder pressure is repeatedly built and released at the pilot opening pressure. The resulting shock loads damage seals, fittings, and cylinder rods while creating dangerous working conditions.
Oversizing Based on Cost Some engineers select pilot operated check valves simply because they cost less, without considering whether the application involves motion control. This “poor man’s counterbalance valve” approach leads to system failures and safety issues.
Ignoring Pilot Ratio Requirements High pilot ratios (R ≥ 8:1) allow load lowering with reduced pilot pressure for faster machine operation and energy saving, best suited for applications where load induced pressures remain approximately constant during motion. Low pilot ratios (R ≤ 4:1) require higher pilot pressure but permit more precise and smooth control of motion, recommended for applications where the geometry determines high changes of load induced pressure during motion.
Conversion Considerations
Upgrading from Pilot Check to Counterbalance If your system exhibits ratcheting motion, excessive shock loads, or inability to control descent speed, upgrading from pilot operated check valves to counterbalance valves solves these issues.
The conversion requires:
- Replacing the valve body with a counterbalance valve of appropriate flow capacity
- Installing pilot pressure adjustment mechanism
- Reconfiguring pilot line connections if necessary
- Properly setting the spring adjustment for your specific load conditions
- Testing under actual operating conditions with safety precautions
Physical Mounting Compatibility Many counterbalance valves are available in mounting configurations compatible with pilot operated check valve installations, simplifying the retrofit process. However, ensure adequate space for the adjustment mechanism and verify port sizes match your existing plumbing.
System Pressure Considerations Counterbalance valves are normally set at 1.3 times the maximum load pressure to ensure the valve will reseat under the heaviest load conditions. Verify your system pressure provides sufficient margin above the required setting pressure.
Making the Right Choice
The decision between pilot operated check valves and counterbalance valves ultimately comes down to whether your application requires motion control during operation.
For static load holding applications—clamping, horizontal positioning, holding presses at top position—pilot operated check valves provide superior zero-leak performance at lower cost.
For applications that involve vertical load lowering, over-center loads, or variable speed requirements, counterbalance valves are not optional upgrade but important safety components. Counterbalance valves are also useful in scenarios where uncontrolled movement can’t be avoided because of overrunning load. When in doubt, remember this simple rule: if the load is in motion and gravity is a factor, you need a counterbalance valve. The modest additional investment prevents equipment damage, extends component life, and ensures operator safety—making it the only responsible choice for motion control applications.
Need help? You may browse product catalog and contact us for a free quote!