When hydraulic systems demand precise flow control at higher pressures and flow rates, direct-acting solenoid valves often fall short. Electromagnetic coils simply can’t generate enough force to shift larger spools against substantial system pressures. Pilot-operated directional solenoid valves solve this by using the system’s own hydraulic pressure to do the heavy lifting while maintaining electrical control convenience.
This guide explores how pilot-operated directional solenoid valves work, their advantages over direct-acting designs, and how to select the right valve for demanding applications. We’ll focus on the HFD Hydraulic VE/B/RO series, which exemplifies modern pilot-operated valve design with integrated emergency features and compact bolt-mounting configurations.
Quick Overview: Pilot-Operated Directional Solenoid Valves
What is a pilot-operated directional solenoid valve?
A pilot-operated directional solenoid valve uses a two-stage actuation system — a small solenoid controls a compact pilot valve, which then uses system hydraulic pressure to shift the larger main spool. This allows a 10–15 watt solenoid to control valves handling hundreds of liters per minute at up to 350 bar, making it the correct choice when direct-acting solenoid valves lack the force to shift larger spools at high system pressures.
Key advantages and specifications (HFD VE/B/RO series):
- Two-stage actuation – pilot solenoid draws only 10–20W; system pressure does the heavy lifting to shift the main spool regardless of operating pressure
- VE/B/RO 14 – 20 L/min; suited to smaller single-acting cylinders up to 80mm bore in light tippers and lift gates
- VE/B/RO 38 – 40 L/min; suited to mid-size dump trucks and industrial tipping equipment with cylinders up to 125mm bore
- Max pressure – 350 bar; provides safety margin above typical mobile equipment operating range of 150–250 bar
- Emergency manual override – mechanically bypasses the electrical system; allows operators to lower a raised dump bed even if the truck’s electrical system fails
- Shift time – 30–60 milliseconds; faster than direct-acting designs in high-pressure applications despite the two-stage design
Example
A dump truck with a raised bed and a failed electrical system would be stranded with the load elevated — a serious safety hazard. The VE/B/RO series emergency manual override allows the operator to manually shift the pilot valve and lower the bed in a controlled manner without any electrical power, preventing dangerous situations at job sites or on public roads.
Summary
Use a pilot-operated directional solenoid valve over a direct-acting design when system pressure exceeds 150 bar, flow requirements exceed 40 L/min, or when emergency manual override is required — the two-stage design delivers reliable high-pressure actuation with lower power consumption and faster response than direct-acting equivalents at these operating conditions.
How Pilot-Operated Valves Work
A pilot-operated directional solenoid valve uses a two-stage actuation system. Instead of the solenoid directly moving the main spool, it controls a small pilot valve that directs pressurized hydraulic fluid to shift the main spool. This design splits the work into two stages: the pilot section uses a small solenoid to control a tiny valve requiring minimal force, which then routes system pressure to chambers on either end of the main spool, creating powerful hydraulic forces needed to shift the larger spool.
The pilot section contains a small directional control valve operated by a compact solenoid coil. When energized, this pilot valve connects the pressure port to one of two pilot chambers while connecting the opposite chamber to tank. Because it only controls pilot flow—typically 1-2 L/min—the solenoid force requirements remain minimal even at high system pressures. This small solenoid might draw only 10-15 watts, yet it can control a main valve handling hundreds of liters per minute.
The main spool uses hydraulic pressure acting on its end surfaces rather than direct solenoid force. When pilot pressure enters one chamber, it creates a powerful hydraulic force that easily overcomes spring pressure and any pressure differential across the spool. The pilot chambers at each end of the main spool have substantially larger surface areas than the pilot valve orifices. This area difference creates hydraulic amplification—a small pilot pressure generates large forces on the main spool.
The pilot pressure system typically requires only 5-10 bar to reliably shift the main spool, regardless of whether the main system operates at 50 bar or 350 bar. This pressure independence makes pilot-operated valves highly reliable across varying operating conditions. Internal pressure balancing passages ensure that main system pressure doesn’t create excessive forces that could prevent spool movement or cause sluggish response.
Key Advantages
Pilot-operated valves deliver several critical performance benefits:
Higher Flow Capacity – These valves handle flow rates from 40 L/min to over 300 L/min without requiring impractically large solenoids. The VE/B/RO series offers models rated at 20 L/min and 40 L/min—ideal for single-acting cylinders in construction, agricultural, and material handling equipment.
Lower Power Consumption – Small pilot solenoids typically draw 10-20 watts, compared to 40-100 watts for large direct-acting valves. This reduced consumption means less heat generation, longer coil life, and lower operating costs—particularly valuable in battery-powered mobile equipment.
Reliable High-Pressure Operation – Direct-acting valves struggle when system pressure creates forces opposing spool movement. Pilot-operated valves remain unaffected because they use the system’s own pressure for actuation, operating equally well at 100 bar or 350 bar.
Faster Response – Despite using two stages, pilot-operated valves often shift faster than direct-acting designs in high-pressure applications. Modern designs achieve shift times of 30-60 milliseconds even with large spool masses and high flow capacities.
The VE/B/RO Series: Specialized Design for Single-Acting Applications
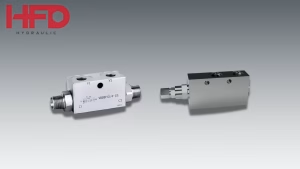
The HFD Hydraulic VE/B/RO series represents a specialized category designed specifically for controlling single-acting hydraulic cylinders in dump trucks, tippers, lift gates, and similar equipment. These valves combine the power advantages of pilot operation with features specifically tailored for single-acting applications.
Two-Way Configuration with Emergency Override
The VE/B/RO series employs a 2-way, 2-position valve configuration optimized for single-acting cylinder control. In the normal position, the valve blocks flow, maintaining cylinder position even under load. This closed-center design prevents cylinder drift and holds loads securely. When the solenoid energizes, the valve opens, allowing hydraulic fluid to flow to the cylinder for extension or retraction under load weight.
The integrated emergency manual override is a critical safety feature that allows manual valve actuation even when electrical power is unavailable. This mechanical override bypasses the electrical system entirely, manually shifting the pilot valve to open the main spool. In dump truck applications, for example, this enables operators to lower a raised bed even if the truck’s electrical system fails, preventing hazardous situations where loads remain elevated indefinitely. The override mechanism is easily accessible yet protected from accidental activation.
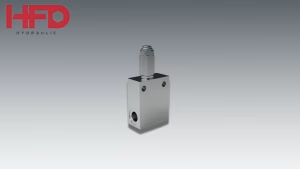
Despite their pilot-operated design, the VE/B/RO series maintains a compact footprint through efficient internal layout. The pilot section mounts directly atop the main valve body, minimizing overall height while ensuring easy solenoid coil replacement. The bolt-mounting configuration allows direct attachment to manifolds or equipment frames without complex mounting brackets, making these valves particularly suitable for space-constrained mobile equipment installations.
Specifications and Performance
The VE/B/RO series offers two flow ratings to accommodate different cylinder sizes and application speeds:
VE/B/RO 14 – Handles 20 L/min, suitable for smaller single-acting cylinders found in light-duty tippers, small lift gates, and auxiliary equipment functions. This flow rate provides adequate speed for cylinders with bore diameters up to 80mm while maintaining precise control. It’s ideal for applications where controlled, moderate-speed movement is required.
VE/B/RO 38 – Delivers 40 L/min capacity for larger cylinders requiring faster cycle times. This flow rating works well for mid-size dump trucks, larger lift gates, and industrial tipping equipment with cylinders up to 125mm bore diameter. The higher flow capacity enables faster cycle times that improve productivity in commercial applications.

Both models operate reliably at pressures up to 350 bar, providing substantial safety margin above typical system pressures of 150-250 bar. This high pressure rating ensures long service life even in demanding applications with frequent pressure spikes that occur during load changes or when cylinders reach end-of-stroke positions. At rated flow, pressure drop remains under 10 bar, indicating efficient internal design that minimizes energy waste and heat generation. This low pressure drop means more of the pump’s energy goes into useful work rather than heating the hydraulic fluid.
Installation and Circuit Design
Proper circuit design and installation ensure optimal valve performance.
Pilot Pressure and Tank Connections
Most pilot-operated valves take pilot pressure internally from the main pressure port, eliminating external pilot supply lines. The VE/B/RO series uses this internal pilot configuration for simplified installation. When system pressure drops below minimum pilot requirements (typically 5-10 bar), the valve may not shift reliably.
The tank port must connect to a properly sized reservoir with minimal backpressure. Size tank lines for low velocity—2-3 feet per second maximum—to minimize pressure drop that could impair valve performance.
Port Configuration
The VE/B/RO series uses straightforward port designations: the pressure port (P) connects to the pump, the work port (A) connects to the cylinder, and the tank port (T) returns fluid to the reservoir. The bolt-mounting design with O-ring sealed face connections eliminates threaded fittings at the valve body, reducing leak points and installation time.
Electrical Installation
Proper electrical setup ensures reliable operation and long coil life.
Voltage and Coil Selection
The VE/B/RO series typically offers coil options for 12VDC, 24VDC, 110VAC, and 220VAC. DC coils are standard in mobile equipment, while AC coils appear in stationary applications. Select voltage to match your control system, accounting for voltage drop in long cable runs. Calculate actual voltage at the coil terminals under load to verify it remains within rated tolerance.
Continuous Duty and Heat Management
The VE/B/RO series uses continuous-rated coils (100% duty cycle), allowing the valve to maintain position indefinitely. However, ensure adequate ventilation around the valve, especially in enclosed spaces or when mounting multiple valves closely. Standard coils handle ambient temperatures up to 50°C; high-temperature options extend this to 70°C or higher.
Protection Circuits

Install a diode across DC coils to suppress voltage spikes generated during de-energization. For AC coils, use a varistor or RC snubber circuit. Mount protection devices close to coil terminals for maximum effectiveness. Include appropriately rated fuses or circuit breakers sized slightly above the coil’s rated current to allow for inrush while protecting against shorts.
Valve Selection Guide
Flow Rate Calculation
Calculate maximum flow based on cylinder size and desired speed. For single-acting cylinders, only the extend portion requires pump flow. Use the formula: Q = (A × V) / 1000, where Q is flow in liters per minute, A is cylinder area in square centimeters, and V is desired velocity in centimeters per second.
Example: A 100mm bore cylinder (area = 78.5 cm²) extending at 5 cm/sec requires 23.5 L/min. The VE/B/RO 38 with 40 L/min capacity provides comfortable margin. Select a valve with rated flow 20-30% above your calculated requirement for lower pressure drop and extended valve life.
Pressure Rating
Choose valves rated at least 1.5 times maximum system pressure to account for pressure spikes. The VE/B/RO series’ 350 bar rating provides excellent margin for most mobile equipment operating at 150-250 bar.
Environmental Factors
Consider temperature range, vibration, and contamination. Standard seals operate from -20°C to +50°C; Viton seals are available for high-temperature applications. The bolt-mounting design provides excellent vibration resistance when properly torqued. Use filtration rated at 25 microns or finer to prevent fluid contamination damage.
Installation Best Practices
Mounting and Clearance
Mount valves with the solenoid upward when possible to allow moisture drainage and facilitate coil replacement. Provide approximately 100mm clearance above the VE/B/RO series coil housing. Ensure the mounting surface is flat, clean, and rigid with surface finish better than 3.2 Ra for proper O-ring sealing.
Torque and Tightening
Use a torque wrench to achieve specified values—typically 25-30 Nm for VE/B/RO mounting bolts. Apply torque in three stages using a diagonal pattern: 30% of final torque, then 70%, finally 100%. This progressive approach ensures even seal compression and prevents distortion.
Electrical Connections
Keep connections clean, tight, and protected from moisture. The DIN 43650 connectors provide good environmental sealing when properly mated. For spray or immersion exposure, apply silicone sealant around the connector base. Route cables to avoid sharp bends, pinch points, and heat sources while allowing slack for thermal expansion.
Maintenance and Troubleshooting
Routine Maintenance
Monitor hydraulic fluid condition every 500-1000 operating hours for mobile equipment. Replace fluid when contamination exceeds acceptable levels. Inspect system filtration regularly and replace elements per manufacturer recommendations. Check for external leakage at valve mounting surfaces and electrical connections.
Common Issues
Slow or erratic shifting – Check system pressure meets minimum pilot requirements. Contamination in pilot passages reduces pilot flow. Cleaning or replacing the pilot section typically resolves this.
Failure to shift – Verify solenoid coil receives proper voltage using a multimeter. Low voltage from undersized wiring or poor connections prevents adequate coil force. If voltage is correct, the coil may have failed or the pilot spool may be stuck.
External leakage – Check mounting bolt torque, as vibration can loosen bolts over time. If torque is correct, seals may be worn and require replacement.
Internal leakage – Worn main spool lands or valve body bore allow cylinder drift. Contamination accelerates this wear. Severely worn valves require replacement.
Safety Considerations
Emergency Override Operation
Before activating the VE/B/RO series emergency manual override, ensure the area beneath and around the load is clear. The override typically provides uncontrolled descent—loads may descend quickly. After using the emergency override, return the lever to its normal position before restoring electrical power to prevent unexpected valve operation.
Pressure Protection
Always install properly sized pressure relief protection in cylinder circuits. The relief valve should locate on the cylinder side of the directional control valve to protect against blockage. Set relief pressure 10-20% above maximum working pressure but below the component ratings.
Maintenance Safety
Never service pilot-operated directional solenoid valves while the system contains pressure. Establish lockout-tagout procedures, operate cylinders through full travel to eliminate trapped pressure, then relieve any remaining pressure before disconnecting components.

Pilot-operated directional solenoid valves provide an efficient solution for controlling high-flow, high-pressure hydraulic systems with electrical signals. By using system pressure for actuation while maintaining compact electrical control, these valves deliver performance, reliability, and efficiency for demanding applications.
The HFD Hydraulic VE/B/RO series demonstrates specialized valve design addressing specific application requirements. The combination of pilot-operated technology, emergency manual override, and optimized single-acting cylinder control makes these valves ideal for mobile equipment, industrial tipping applications, and systems requiring reliable flow control with emergency backup operation.
Proper selection, installation, and maintenance ensure pilot-operated directional solenoid valves deliver years of trouble-free service in challenging hydraulic applications.