Refuse collection trucks are among the most hydraulically demanding vehicles in daily municipal and commercial service. A rear-loader compactor running a full shift may complete several hundred compaction cycles before returning to the depot. Each cycle drives the packer blade cylinder to near-maximum extension, compressing waste into the hopper body. The ejection cylinder makes its full stroke every time the truck tips at the transfer station or landfill.
At that frequency, even minor inefficiencies in cylinder control accumulate into serious mechanical problems. A cylinder that repeatedly contacts its mechanical hard stop under pressure loads its seals, mounting pins, and the compactor body frame with forces they were not designed to absorb as a matter of routine. Over weeks and months, the result is premature seal failure, cracked mounting brackets, and increased pump wear from sustained high-pressure bypass events.
The solution is a valve that responds directly to the cylinder’s own physical position — not pressure signals, not electrical sensors, not operator reaction time. A push-button end of stroke valve does exactly that. This article covers how the valve works, why it fits refuse compactor hydraulics well, how it integrates into the circuit, and what the HFD FCA valve offers for this application.
Quick Overview: Push-Button End of Stroke Valve for Refuse Compactor Trucks
- A push-button end of stroke valve stops hydraulic flow when a cylinder rod or bracket physically depresses the valve button at full extension.
- In refuse compactor trucks, the valve protects the compaction ram and ejection blade cylinder from seal damage and structural overload caused by repeated end-of-stroke pressure spikes.
- The HFD FCA valve handles up to 300 bar and 60 l/min, with a 7 mm maximum stroke, steel body, and NBR seals for mineral oil systems.
- It installs in the pressure line feeding the cylinder and provides automatic flow cutoff without electronic sensors, external cables, or operator input.
What Makes a Push-Button End of Stroke Valve Different
End of stroke valves stop hydraulic flow when a cylinder or moving component reaches a defined position in its travel. Several actuation types exist across different applications.
A cable-actuated end of stroke valve uses tension in a cable connected to a tipping body. As the body rises, the cable pulls the valve spool closed — a configuration well suited to the curved arc of a dump truck body. A slider or lever-type valve responds to a cam or mechanical arm moving alongside the actuator.
A push-button end of stroke valve works through direct physical contact. The valve’s button projects outward from the body. When a bracket, rod, or actuating plate — mounted to the moving component — travels into contact with that button, it depresses it through the valve’s stroke, closing the internal flow path and stopping oil supply to the cylinder. When the cylinder retracts, the contact breaks, the spring-loaded button releases, the valve reopens, and the circuit is ready for the next cycle.
This mechanism suits applications where:
- The actuator travels in a consistent, linear path
- A fixed contact point can be precisely positioned relative to the valve button
- There is no need for external cable routing through enclosed or confined spaces
- Repeatability at the stop point matters more than adjustable mid-stroke control
For a complete overview of end of stroke valve configurations, actuation types, and selection principles, refer to: End of Stroke Valves: Complete Guide for Hydraulic Systems
Why Refuse Compactor Trucks Need This Protection
How the Compaction Circuit Works
A rear-loader refuse compactor uses a hydraulic packer blade to compress waste as it is loaded from the hopper into the body. The blade is driven by one or two hydraulic cylinders mounted within the compactor body structure. On each cycle, the cylinders extend to push the blade forward through its full travel range, then retract to the starting position for the next load.
A separate ejection cylinder runs the full length of the body and pushes the compacted load out through the rear gate when the truck tips at the disposal site. This cylinder also travels to near-maximum extension on every ejection cycle.
Both cylinders operate to the limit of their designed stroke on a regular, predictable basis. That regularity is both the opportunity and the risk.

The Failure Modes Without End-of-Stroke Control
Seal damage from end-of-stroke pressure spikes. When a cylinder reaches its mechanical hard stop with pump flow still being delivered, system pressure rises sharply until the relief valve opens. In a compactor running hundreds of cycles per day, this spike occurs at the end of every single extension stroke. Repeated exposure to these pressure events accelerates seal wear, leading to internal and external leakage well ahead of the cylinder’s expected service life.
Structural overload at mounting points. At mechanical hard stop, force is transmitted into the cylinder’s mounting brackets, pins, and the compactor body’s structural frame rather than through the cylinder’s designed load path. Weld fatigue, pin wear, and bracket cracking develop gradually and are often attributed to general wear until the root cause is identified.
Accelerated pump and relief valve wear. If the circuit relies on the system relief valve to absorb excess energy every time the cylinder bottoms out, both the relief valve and the pump undergo repeated high-load events. This shortens the service interval for both components and increases unplanned downtime.
Cycle inconsistency from operator variation. In manual or semi-manual systems, operators may shorten cycles to increase throughput, allowing the cylinder to retract before a relief event — or, under time pressure, hold the control longer than necessary. A mechanical end-of-stroke valve removes this variable entirely.
The HFD FCA Push-Button End of Stroke Valve
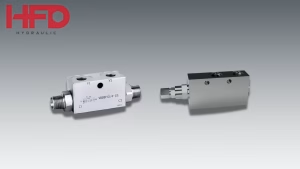
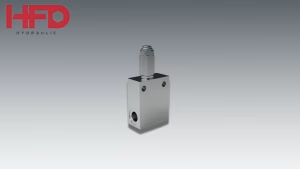
HFD Hydraulic offers the Push-Button End of Stroke Valve – FCA, a Walvoil-design valve engineered for precise hydraulic position control in mobile and industrial equipment.
Technical Specifications
| Parameter | FC02A | FC03A |
| Maximum pressure | 300 bar (4,350 psi) | 300 bar (4,350 psi) |
| Maximum flow | 30 l/min (7.9 US gpm) | 60 l/min (15.9 US gpm) |
| Port size | G3/8 | G1/2 |
| Maximum stroke | 7 mm (0.27 in) | 7 mm (0.27 in) |
| Body material | Steel | Steel |
| Seals | NBR | NBR |
| Temperature range | −40°C to +100°C (−40°F to +212°F) | Same |
| Weight | 0.75 kg (1.65 lb) | 0.77 kg (1.70 lb) |
| Fluid compatibility | Mineral-based hydraulic oil | Same |
| Max contamination level | ISO 4406: 18/16/13 | Same |
| Fluid viscosity range | 10–200 cSt | Same |
Source: HFD Hydraulic — Push-Button End of Stroke Valve FCA product page
Choosing Between FC02A and FC03A
The two variants share the same body dimensions, pressure rating, stroke length, and actuation mechanism. The only differences are flow capacity and port size.
FC02A (G3/8, 30 l/min) suits compactor systems with smaller bore cylinders or lower-displacement pumps. If the compaction circuit operates at under 25 l/min during the extension stroke, this variant covers the requirement with margin.
FC03A (G1/2, 60 l/min) is the appropriate choice for full-size rear-loader and side-loader compactors with larger bore cylinders. The G1/2 port minimizes restriction at the valve connection and keeps pressure drop low during the working stroke, where flow demand is highest.
When in doubt between variants, the larger FC03A is the safer selection — over-sizing flow capacity has no mechanical downside in this circuit position, while under-sizing creates avoidable pressure loss on every cycle.
Steel Body Advantage in Compactor Environments
Compactor trucks operate in some of the harshest environments of any mobile hydraulic equipment. Compactor trucks are rough on hardware — between the muck, the washdowns, and the constant vibration, external components wear faster than on most other mobile equipment. The FCA’s steel body provides greater resistance to impact and corrosion than cast iron alternatives, particularly at the valve mounting points which are subject to vibration-induced fatigue over the truck’s service life.
How the FCA of HFD Hydraulic Integrates Into the Compactor Hydraulic Circuit
The FCA is positioned in the pressure line feeding the cap-end port of the compaction cylinder — the port that receives flow during the extension (packing) stroke.
Circuit Integration — Step by Step
- The operator commands the packing stroke. The directional control valve (DCV) shifts, routing pump flow toward the compaction cylinder.
- Flow passes through the FCA valve at port P and exits at port A, continuing to the cylinder cap end. The packer blade advances.
- As the blade approaches its maximum designed travel position, an actuating bracket mounted to the blade frame — or directly to the cylinder rod end assembly — moves into alignment with the FCA’s push button.
- The bracket makes contact with the button and depresses it through its 7 mm stroke. The FCA valve closes, stopping oil flow to the cylinder.
- Pressure in the line between the DCV and the FCA rises briefly. The system relief valve opens and routes flow back to tank, or an unloading circuit handles the excess flow. The cylinder holds position.
- The operator shifts the DCV to retract. The rod-side port opens to pump flow; the cap-end port connects to tank. The cylinder retracts, drawing the blade back.
- As the blade moves away from the valve, the contact breaks. The button extends under spring force. The FCA reopens. The circuit is ready for the next cycle.
Circuit Design Notes
Relief valve setting: Because the FCA closes while the pump continues to run (briefly), the system relief valve must be correctly set to handle this condition. The recommended practice is to set the relief valve 50–100 bar above normal compaction operating pressure, while remaining below the maximum rated pressure of all circuit components. This is standard practice for any end-of-stroke application.
Return line: The FCA only controls the P-to-A flow path (extension stroke). The retraction circuit is unaffected and functions normally through the directional control valve.
Multiple cylinders: On compactors with two packer blade cylinders operating in parallel, an FCA valve is required on each cylinder’s cap-end line to provide consistent end-of-stroke protection across both actuators.
For context on directional control valves used upstream of this circuit position, see: Hydraulic Directional Control Valve Guide and Pilot Operated Directional Solenoid Valves
Installation Considerations
Actuating Bracket Design and Alignment
The bracket or rod that contacts the FCA push button must be:
- Rigidly attached to the moving component (packer blade frame or cylinder rod-end bracket) with no flex or play in the mounting
- Aligned so contact is made at the center of the button face — angled contact accelerates button wear and can cause the valve to close incompletely
- Sized so the full 7 mm button stroke is achieved before the cylinder reaches its mechanical hard stop, not simultaneously with it
A flat contact pad is preferred over a sharp edge or point on the actuating bracket. Distributed contact load reduces localized wear on the button face and extends service life.
Valve Mounting Location
Mount the FCA to a fixed structural member of the compactor body. Avoid surfaces subject to flexing or high vibration amplitude, such as thin sheet metal panels or unsupported frame sections. Use fasteners torqued to the manufacturer’s specification. In high-vibration environments, thread-locking compound on the mounting fasteners is a sound precaution.
Mount it somewhere accessible. Port connections that require panel removal to inspect tend not to get inspected.
Fluid Compatibility Confirmation
The FCA’s NBR seals are rated for mineral-based hydraulic oil, which is standard in refuse compactor systems. If the customer’s circuit uses a biodegradable or fire-resistant fluid, confirm seal compatibility with the fluid supplier before specifying the FCA.
Maintenance and Troubleshooting
The FCA valve has no complex internals and minimal wear surfaces under normal operating conditions. Routine maintenance requirements are straightforward.
Periodic inspection points:
- Check the button face and actuating bracket contact pad for wear at regular service intervals. Uneven wear patterns imply misalignment and should be corrected before button travel is compromised.
- Inspect hydraulic port connections for seepage at every scheduled service. Small leaks indicate loose fittings or degraded O-rings at the port threads.
- Verify that the actuating bracket remains securely fastened and has not shifted position due to frame flex or fastener loosening.
- Confirm that the button returns fully to its extended position after each cycle retraction. A button that stays partially depressed indicates contamination in the valve body or internal spring fatigue.
Common problems and responses:
| Symptom | Likely Cause | Corrective Action |
| Cylinder does not stop at end of stroke | Button not being fully depressed — bracket misaligned or shifted | Re-align and re-secure actuating bracket |
| Cylinder stops before reaching full stroke | Bracket contacting button too early | Adjust bracket position to delay contact |
| Pressure spike audible at end of stroke | Relief valve setting too close to operating pressure | Increase relief setting within component limits |
| Hydraulic leak at valve body | Loose port fittings or worn O-rings | Re-torque fittings; replace O-rings if leak persists |
| Button does not return after retraction | Contamination in valve body | Flush circuit; inspect valve for debris ingress |

A push-button end of stroke valve provides automatic, position-based flow cutoff triggered by direct physical contact at the cylinder’s end-of-stroke position. For refuse compactor trucks — where packer blade and ejection cylinders complete hundreds of full-stroke cycles per shift — this protection directly reduces seal wear, structural fatigue, and pump loading caused by repeated end-of-stroke pressure events.
The HFD FCA valve is available in two flow variants (FC02A at 30 l/min and FC03A at 60 l/min), rated to 300 bar, with a compact steel body and NBR seals suited to mineral oil service. Its direct-contact push-button mechanism requires no cable routing, no external tension adjustment, and no electronic components — delivering consistent end-of-stroke protection through the full service life of the vehicle.