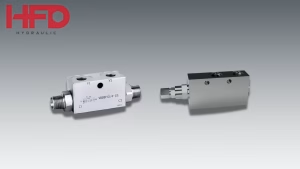
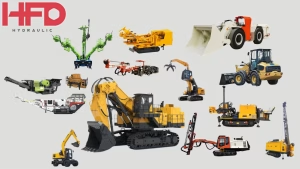
Mobile hydraulic equipment operates in demanding environments where reliability isn’t optional. From construction sites to mining operations, shuttle valves serve as critical components ensuring machines respond correctly while maintaining safety and efficiency under extreme conditions.
Quick Overview: Shuttle Valves in Mobile Hydraulics
How are shuttle valves used in mobile hydraulic equipment?
Shuttle valves in mobile hydraulics automatically route pressure from whichever circuit has the highest pressure to a priority function — steering, braking, or load sensing — without electronics, sensors, or operator input. This purely mechanical pressure selection makes them the preferred safety and efficiency component across construction, agricultural, forestry, and mining equipment operating in extreme environments.
Key applications by industry:
- Construction (excavators, wheel loaders) – steering priority circuits ensure steering receives adequate pressure even when boom and bucket circuits demand maximum flow simultaneously
- Agriculture (combine harvesters, tractors) – load-sensing shuttle valve networks identify the highest demand across multiple simultaneous functions and signal the pump to match output, reducing fuel consumption by up to 18%
- Forestry (harvesters, forwarders) – coordinate 10–15 simultaneous hydraulic functions in harvester heads across extreme temperatures from −40°C to +50°C with no electronics to fail from vibration or contamination
- Mining (haul trucks, LHD machines) – dual brake circuit redundancy; shuttle valve instantly switches to backup circuit if primary fails, maintaining braking on 200–400 tonne trucks on steep haul roads
Example
An Arizona copper mine documented 17 primary brake circuit failures across their haul truck fleet over five years. In every case, the shuttle valve-based backup system maintained brake function and allowed operators to bring loaded trucks to a safe stop — with no runaways, no fatalities, and no equipment losses from brake failure.
Summary
Shuttle valves deliver mechanical reliability that electronic systems cannot match in mobile equipment — no sensors to fail from vibration, no programming to drift, and no lag between pressure change and valve response, making them the first choice for safety-critical priority and redundancy circuits across all mobile hydraulic applications.
Why Mobile Hydraulics Needs Specialized Solutions
Mobile equipment like excavators, combine harvesters, and haul trucks must perform multiple functions simultaneously while facing vibration, temperature extremes, and contamination that would disable less robust components.
Shuttle valves excel because they make autonomous pressure routing decisions without electronics, sensors, or programming. When an excavator operator steers while lifting a heavy load, shuttle valves instantly prioritize steering mechanically—even when covered in mud or operating in freezing temperatures. Their compact design integrates directly into manifolds, perfect for space-constrained mobile equipment.
Construction Equipment: Priority Circuits That Maintain Control
Excavator Steering and Implement Coordination
Excavators represent one of the most demanding applications for shuttle valve technology. Operators control multiple functions simultaneously—swing, boom, stick, bucket, and travel—while maintaining precise steering regardless of implement loads.
Steering circuits use shuttle valves to ensure steering receives priority pressure even when other functions demand maximum flow. When an operator turns while lifting a heavy load, the shuttle valve automatically diverts sufficient pressure to steering, temporarily reducing boom flow. This happens instantaneously and mechanically, without lag or electronic intervention.
Practical Implementation:
The typical excavator steering priority circuit places a shuttle valve between the steering and work function circuits. The steering pump supplies constant pressure to one inlet, while work function pressure feeds the second inlet. The output connects to work functions, ensuring they receive flow only after steering demand is satisfied.

Many excavators implement load-sensing systems using shuttle valve networks to identify the highest load pressure among multiple functions. These valve networks watch all the pressures—boom, stick, bucket, and swing—and tell the pump controller which one needs the most power. That way, the pump only works as hard as it needs to.
Wheel Loader Performance Optimization
Wheel loaders face similar challenges with different operational patterns. During typical loading cycles, operators drive into piles, raise buckets, back away, and turn toward trucks—often executing these simultaneously.
Case Study: Quarry Loading Operations
A limestone quarry upgraded their wheel loader fleet with improved shuttle valve configurations. Previously, operators reported steering becoming unresponsive when lifting full buckets. After installing higher-capacity shuttle valves with faster response times, operators noted immediate improvement. The valves redirected adequate flow to steering within milliseconds, regardless of bucket load. This increased loading cycle efficiency by approximately 8% as operators maintained higher speeds with confident steering response.
Agricultural Machinery: Load-Sensing Networks for Precision Farming
Combine Harvester Multi-Function Management
Modern combine harvesters integrate dozens of hydraulic functions: header height control, reel speed, feeder engagement, cleaning shoe adjustment, unloading auger control, and steering—all operating simultaneously during harvest.
Load-sensing hydraulic systems use shuttle valve networks to manage these competing demands efficiently. Each function has its own load-sensing line reporting current pressure. These feed into a shuttle valve network that identifies the highest load and routes this signal to the pump controller, which adjusts output to maintain appropriate pressure while minimizing excess.
Real-World Impact:
A Midwest farming operation documented fuel consumption before and after upgrading combines to load-sensing systems with improved shuttle valve networks. Over one harvest season covering 12,000 acres, the load-sensing equipped machines showed 18% lower fuel consumption compared to older fixed-displacement systems while maintaining identical productivity.
The savings stemmed from the shuttle valve network reducing pump pressure during low-load operations. When combining travel between fields with headers raised and systems idle, the load-sensing system recognizes minimal load and reduces pump output. Fixed-displacement systems maintain full pressure regardless, wasting significant fuel.
Tractor Implement Hydraulics
Agricultural tractors serve as universal power sources for dozens of implements, each with unique hydraulic demands. A single tractor might operate a front loader, three-point hitch, mid-mount mower, and auxiliary outlets—all from a common system.
Shuttle valves manage priority between these diverse functions while ensuring steering and braking always receive adequate pressure. Priority hierarchy flows mechanically: steering receives top priority, followed by brakes, then implement control, with auxiliary functions receiving lowest priority.
Forestry Equipment: Multi-Function Control in Extreme Conditions
Harvester Head Hydraulics
Forestry harvesters perform complex operations in harsh environments—felling trees, delimbing, measuring logs, and cutting to length while traveling through forests on uneven terrain. The harvester head alone may incorporate 10-15 different hydraulic functions operating simultaneously.
Shuttle valves coordinate functions including feed roller pressure, saw motor control, delimbing knife positioning, and head rotation. Feed roller grip pressure receives high priority to prevent tree slippage, while head rotation operates at lower pressure. The saw motor demands high pressure during cutting but minimal pressure between cuts. The shuttle valve network allocates pressure dynamically based on instantaneous demands.

Forestry equipment faces extreme temperatures from -40°F to 120°F, constant vibration, impact loading, and contamination from sawdust and bark debris. Shuttle valves excel because they contain no electronics to fail from vibration or contamination, no complex sealing vulnerable to debris, and no adjustments that drift during operation.
Forwarder Load Management
Forwarders transport logs using hydraulic grapples and boom systems to load and unload. Load weights vary dramatically between empty and fully loaded states, affecting machine stability.
Field data from a Canadian forestry operation showed forwarders equipped with load-sensing hydraulics and optimized shuttle valve configurations achieved 23% better fuel efficiency compared to earlier constant-pressure systems, while operators reported improved control and reduced hand fatigue.
Mining Operations: Brake Redundancy and Safety Systems
Haul Truck Brake Circuit Redundancy
Mining haul trucks carrying 200-400 tons navigate steep haul roads where brake failure would be catastrophic. Shuttle valves provide the mechanical reliability necessary for critical brake circuit redundancy.
Dual-Circuit Architecture:
Haul truck brake systems separate front and rear circuits. Each has independent pressure sources, accumulator backup, and control systems. Shuttle valves connect these circuits at brake actuators, ensuring brakes receive pressure from whichever circuit is functioning.
During normal operation, both circuits supply pressure, and the shuttle valve passes the higher pressure to brakes. If the primary circuit fails due to ruptured lines, pump failure, or leaks, the shuttle valve immediately shifts to supply pressure from the backup circuit, maintaining brake function without operator intervention.
Safety Impact:
An Arizona copper mining operation documented 17 primary brake circuit failures over five years in their haul truck fleet. In every case, shuttle valve-based backup systems maintained brake function, allowing operators to safely stop loaded trucks. Without shuttle valve redundancy, these failures could have resulted in runaway trucks on steep haul roads, potentially causing fatalities and equipment losses worth millions.

Underground Mining Vehicle Control
Underground mining presents additional challenges: space constraints, poor visibility, and personnel working near equipment demand precise vehicle control. Load-haul-dump (LHD) machines operating in confined underground spaces require exceptional maneuverability using articulated steering with hydraulic cylinders. Shuttle valves ensure steering receives adequate pressure even when buckets load material near maximum system pressure. Any steering delay in tunnels barely wider than the machine could result in wall collisions or equipment damage. Mechanical prioritization provides more reliable response than electronic systems in underground environments where electromagnetic interference from blasting and electrical equipment can disrupt controls.
Design Considerations for Mobile Applications
Vibration and Environmental Resistance
Mobile equipment subjects components to vibration levels far exceeding industrial applications. Shuttle valves designed for mobile use incorporate hardened bodies resisting fatigue cracking, precision fits maintaining sealing despite vibration, and anti-vibration mounting provisions.
Mobile systems operate in dirty environments where contamination control proves challenging. Shuttle valves offer inherent advantages with simple internal designs providing fewer contaminant accumulation locations. The shuttling element moves relatively short distances within a simple bore, making stuck operation less likely than in complex valve designs.
Filtration Requirements:
- Return line filtration rated 10-15 microns for standard mobile applications
- Pressure line filtration for critical circuits like steering and brakes
- Breather filters on reservoirs preventing airborne contamination
- Regular fluid sampling monitoring contamination trends
- Scheduled filter replacement based on operating hours
Temperature Performance and Seal Selection
Mobile equipment operates across extreme temperature ranges. Construction equipment in desert conditions reaches 120°F ambient, while forestry equipment in Canadian winters faces -40°F.
Seal Material Selection:
- NBR (Nitrile): -40°F to 250°F, suitable for most applications with mineral oil
- FKM (Viton): -15°F to 400°F, necessary for high-temperature or synthetic fluids
- EPDM: -65°F to 300°F, for extreme cold performance
- Polyurethane: -30°F to 200°F, excellent wear resistance for high-cycle applications
Compact Integration
Mobile equipment designers constantly battle space constraints. Shuttle valves excel through extensive cartridge-style designs integrating directly into manifolds. Rather than external valves consuming space, cartridge shuttle valves install in drilled cavities within aluminum or steel manifolds.
Manifold integration eliminates external plumbing, reduces leak points, eliminates vulnerable hose routings, and simplifies machine assembly. Custom manifolds integrate multiple shuttle valves with other hydraulic functions—pressure relief, check valves, flow controls—creating complete circuits in compact packages.

Troubleshooting Common Mobile Application Issues
Sluggish Steering Response
When operators report slow steering or requiring more input force, issues may be responsible. Diagnosis steps:
- Measure steering circuit pressure during straight-ahead operation (should be minimal)
- Apply steering input while monitoring pressure (should rise immediately to system pressure)
- Load implement functions and repeat steering pressure test (pressure should remain adequate)
If steering pressure drops when implements operate, the steering priority shuttle valve may be sticking from contamination or seal wear.
Excessive Heat Generation
Mobile hydraulic systems generate significant heat, but reservoir temperatures exceeding 180°F indicate problems. Shuttle valves can contribute if internal leakage allows high-pressure fluid to leak across the shuttle element constantly, converting hydraulic energy to heat. Diagnosing internal leakage requires precise flow measurements and pressure testing under load.
Intermittent Function Loss
When functions work normally sometimes but fail intermittently, worn or damaged shuttle elements may stick in intermediate positions, partially blocking flow to both circuits. Testing requires operating the affected circuit while monitoring pressures at all shuttle valve ports. Pressure readings that fluctuate unexpectedly indicate shuttle valve problems.
The Future of Shuttle Valves in Mobile Hydraulics
Electronic Integration and Smart Hydraulics
While shuttle valves provide purely mechanical operation today, future mobile hydraulic systems will likely integrate sensors and electronic monitoring without sacrificing mechanical reliability. Pressure sensors at valve ports can provide real-time data to machine controllers, enabling predictive maintenance and performance optimization while maintaining mechanical backup functionality.
Some manufacturers are developing shuttle valves with integral position sensors that report shuttle element position electronically. This information allows monitoring of how frequently the valve switches between positions, load distribution between circuits, and early warning of sticking or degraded operation.
Electro-Hydraulic Hybrid Approaches
The next generation of mobile hydraulic systems may use electro-hydraulic hybrid approaches where shuttle valves provide mechanical pressure selection and circuit protection while electronic controls optimize overall system performance. This architecture maintains the reliability advantages of mechanical shuttle valves while adding intelligent system management.
For example, an excavator might use traditional shuttle valves for steering priority and implement pressure selection, but add electronic controls that adjust pump displacement and implement speed based on operational conditions. They ensure safe operation even if electronics fail, while electronic controls optimize efficiency during normal operation.
Miniaturization and Integration
As mobile equipment becomes more compact and multifunctional, hydraulic components must shrink accordingly. Future shuttle valve designs will likely incorporate more functions into smaller packages through advanced manufacturing techniques.
Additive manufacturing (3D printing) of metal components may enable valve designs with complex internal passages and integrated functions impossible to manufacture with conventional machining. These advanced designs could integrate shuttle valve functions with pressure relief, flow control, and logic elements in single compact units.
Making the Right Shuttle Valve Choice for Your Mobile Application
Selecting appropriate shuttle valves for mobile hydraulic applications requires understanding your specific operational requirements, environmental conditions, and performance expectations.
Priority System Requirements: Clearly define which functions require priority over others in your application. Steering and braking always demand top priority, but secondary priorities vary by machine type and operational requirements.
Pressure and Flow Specifications: Match shuttle valve pressure ratings to your system maximum pressure with appropriate safety margin—typically 1.5x maximum operating pressure. Flow capacity must accommodate maximum instantaneous flow demands with minimal pressure drop.
Environmental Conditions: Consider operating temperature range, contamination exposure, vibration levels, and shock loading when specifying valve construction materials, seal materials, and mounting requirements.
Integration Approach: Decide between standalone valves with external porting or cartridge valves for manifold integration based on space constraints, serviceability requirements, and manufacturing considerations.
Maintenance Accessibility: Ensure valve locations allow inspection and replacement without extensive machine disassembly. Balance this against the packaging efficiency of integrated manifolds.
At HFD Hydraulic, we manufacture shuttle valves specifically designed for demanding mobile applications across construction, agricultural, forestry, and mining industries. Our engineering team works with equipment manufacturers and end users to specify optimal shuttle valve solutions for specific applications.
Whether you’re designing a new machine, upgrading existing equipment, or troubleshooting performance issues, proper valve selection and integration makes the difference between reliable operation and costly downtime.
Contact us today to discuss your mobile hydraulic application. Our engineers will help you select shuttle valves that provide the reliability, performance, and longevity your equipment demands. Looking for other hydraulic components for mobile applications? Explore our complete product range including counterbalance valves, flow control valves, pressure relief valves, and pilot operated check valves.